LANGUAGE
 中文简体
 русский
 Français
 Español
 Português
 عربى
Content
- 1 1. The Role of Extrusion in Modern Cable Manufacturing
- 2 2. Product Overview
- 3 3. Multi-Material Processing Capability
- 4 4. Precision Plasticization and Melt Stability
- 5 5. Torque Transmission and Hardened Helical Gear Reduction
- 6 6. Intelligent Power Regulation and Energy Management
- 7 7. Material Utilization and Cost Reduction
- 8 8. Output Capacity for High-Volume Production
- 9 9. Product Quality and Dimensional Consistency
- 10 10. Compliance-Oriented Cable Production
- 11 11. Advantages Compared with Conventional Extruders
- 12 12. Advanced Manufacturing Strengths Behind the Equipment
- 13 13. Integration into a Complete Cable Production Line
- 14 14. Operational Workflow
- 15 15. Automation, Labor Efficiency, and Production Management
- 16 16. Installation and Selection Considerations
- 17 17. Safety and Maintenance Priorities
- 18 18. Return on Investment and Total Cost of Ownership
- 19 19. Recommended Applications
- 20 20. Frequently Asked Questions
- 20.1 Q1: Which materials can the High-Efficiency PP PVC PE Cable Extruder process?
- 20.2 Q2: What is the maximum production output?
- 20.3 Q3: How does the machine improve material utilization?
- 20.4 Q4: Why is a hardened helical gear reducer important?
- 20.5 Q5: Can one machine process both PP and PVC?
- 20.6 Q6: Is the machine suitable for a complete cable production line?
- 20.7 Q7: What quality standards are associated with the product?
- 20.8 Q8: Does high output necessarily mean higher energy consumption?
- 20.9 Q9: What information should a buyer provide when requesting a quotation?
- 20.10 Q10: How can manufacturers protect long-term equipment performance?
- 21 21. Why This Extruder Is a Practical Strategic Investment
- 22 22. Conclusion
- 23 References
- 24 Product: High-Efficiency PP PVC PE Cable Extruder
The cable industry is under constant pressure to produce more while using fewer resources. Manufacturers must manage changing material prices, increasingly demanding quality requirements, shorter delivery schedules, and a broad range of cable specifications. In this environment, an extrusion line is not simply a machine for melting and shaping polymer. It is a central production asset that directly influences material consumption, output stability, surface quality, energy use, labor efficiency, and the overall competitiveness of a cable factory.
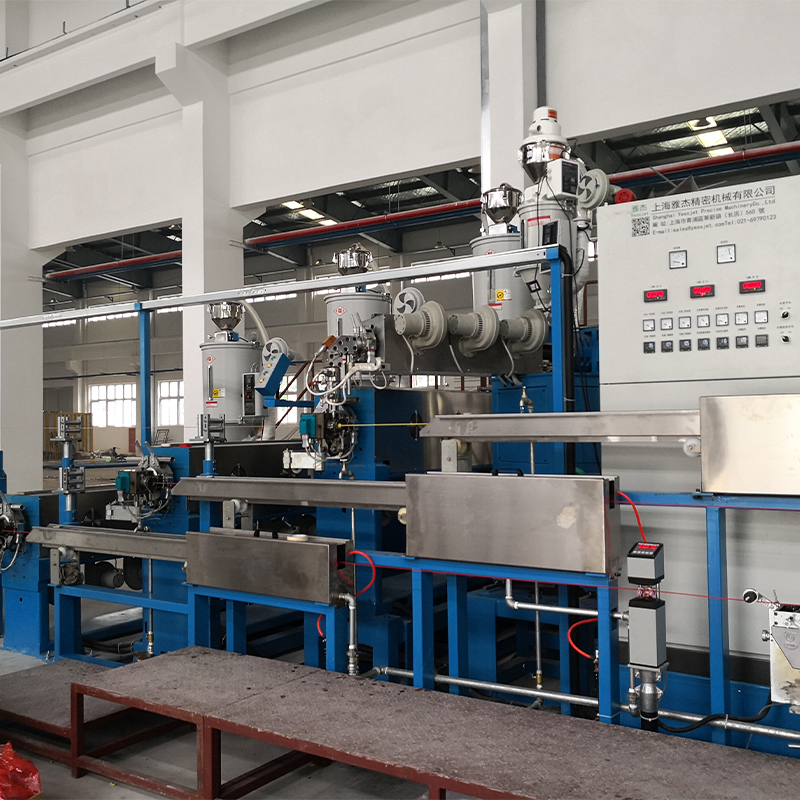
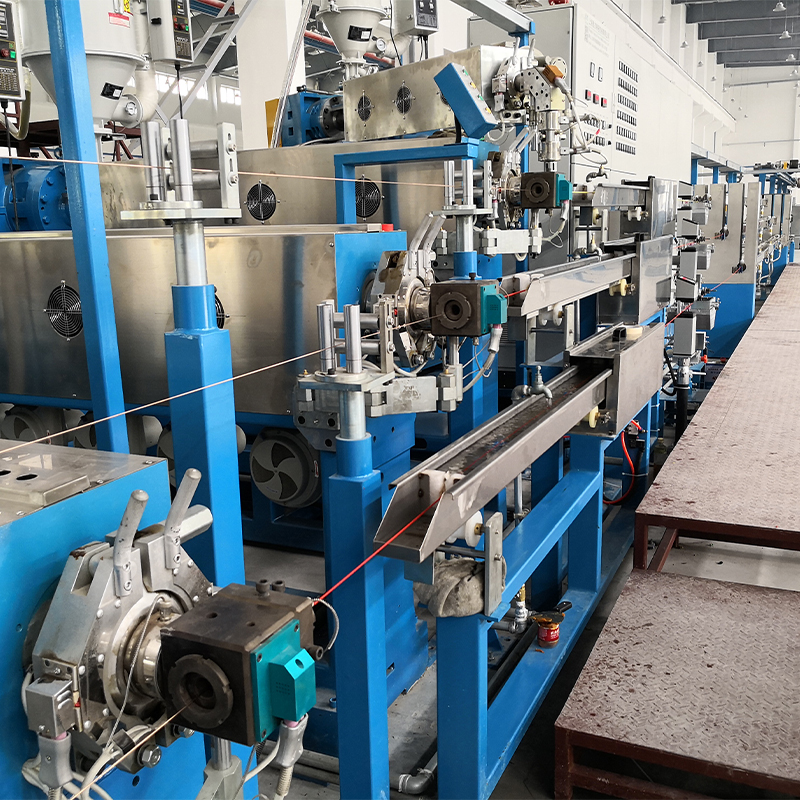
The High-Efficiency PP PVC PE Cable Extruder is designed as a multifunctional core device for cable insulation and jacketing applications. It is compatible with polypropylene (PP), polyvinyl chloride (PVC), and polyethylene (PE), allowing one production platform to support multiple cable product categories. Its engineering combines a precision plasticization system, advanced torque transmission, a hardened helical gear reducer, and intelligent power regulation. Together, these features are intended to deliver stable extrusion, efficient energy use, and reliable operation across different polymer characteristics.
With a maximum output of up to 240 kg/h for large-caliber cable applications, the extruder is suitable for cable enterprises that need a practical balance between production volume, material economy, and process flexibility. Its stated material-utilization improvement of 15% compared with conventional models gives manufacturers an important opportunity to lower raw material costs, which are often one of the largest expenses in cable production.
This article examines the machine’s operating concept, material compatibility, technical strengths, production value, quality advantages, and the manufacturing capabilities behind its design. It also explains how the equipment can contribute to a more streamlined wire and cable production workflow.
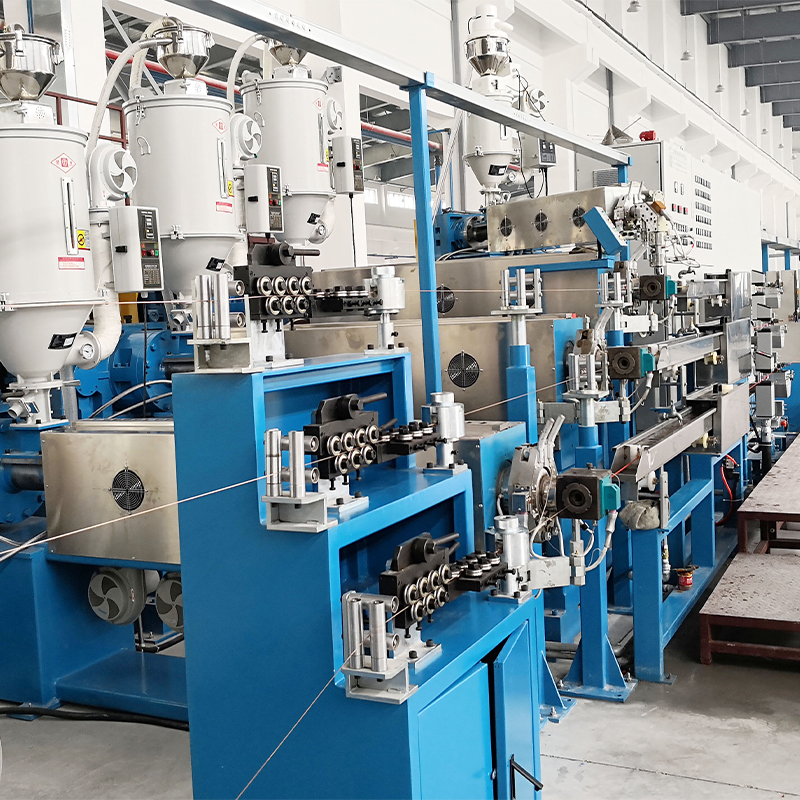
High-Efficiency PP PVC PE Cable Extruder
1. The Role of Extrusion in Modern Cable Manufacturing
Extrusion is one of the most important stages in the manufacture of insulated wires and power, control, communication, and specialty cables. During the process, polymer pellets or compound are heated, plasticized, compressed, and conveyed through a die. The molten material is then formed around a conductor or applied as an outer jacket. After exiting the die, the coating is cooled and stabilized so that it meets the required dimensions and performance specifications.
Although the principle appears straightforward, the actual process involves several variables. Polymer temperature, screw speed, back pressure, torque, melt homogeneity, die centering, line speed, cooling conditions, and take-up tension all influence the final product. A small deviation in any one of these factors can cause eccentric insulation, surface roughness, voids, inconsistent diameter, poor adhesion, or excessive material consumption.
For this reason, an effective cable extruder must perform more than basic melting. It must deliver a consistent melt, maintain predictable pressure, transmit torque efficiently, and respond appropriately when production conditions change. It should also make it possible to process different materials without requiring an entirely separate machine for each polymer family.
The High-Efficiency PP PVC PE Cable Extruder addresses these requirements through a combination of mechanical strength and intelligent regulation. Rather than focusing only on maximum nominal speed, its design emphasizes stable operation, high material utilization, and compatibility with multiple cable production requirements.
2. Product Overview
The High-Efficiency PP PVC PE Cable Extruder is designed for the insulation and jacketing of cables using PP, PVC, and PE. These materials have different processing characteristics. PP is a relatively crystalline polymer with a higher melting range and specific requirements for thermal control. PVC is an amorphous material whose processing window is closely related to shear, temperature, residence time, and thermal stability. PE has its own melt behavior, viscosity profile, and cooling requirements depending on the grade and formulation.
A machine intended to work with all three materials must provide sufficient control across different operating conditions. It must heat materials evenly, avoid unnecessary thermal degradation, maintain stable conveying, and provide a consistent output rate. The equipment’s torque transmission and plasticization systems are therefore central to its performance.
The machine is positioned as a high-efficiency solution for cable enterprises that manufacture different products or change materials according to customer requirements. Instead of investing in a separate extrusion platform for each polymer type, a manufacturer can use a versatile extruder as part of a broader production line. This approach can simplify equipment planning, reduce idle capacity, and support more responsive production scheduling.
The extruder can be integrated with upstream pay-off systems, conductor preheating or guiding equipment where required, crossheads and dies, cooling equipment, diameter control devices, spark testers, capstans, take-up systems, coiling machines, and packaging equipment. It may also be used within a complete wire and cable production solution supplied by an experienced machinery manufacturer.
3. Multi-Material Processing Capability
3.1 PP Processing
Polypropylene is valued in selected cable applications for its low density, chemical resistance, electrical insulation properties, and favorable mechanical performance. Because PP has a crystalline structure, it requires careful management during melting and forming. Inconsistent heating or conveying can lead to uneven plasticization, fluctuations in melt pressure, or variations in the finished insulation layer.
The extruder’s precision plasticization system is intended to create a more uniform melt before the material reaches the die. Consistent plasticization helps improve the stability of the coating process and reduces the risk of unplasticized particles or irregular flow. Intelligent power regulation can also help the machine respond to changing load conditions during production, especially when the material feed rate or line speed changes.
3.2 PVC Processing
PVC is widely used for insulation and jacketing because it can be formulated to provide different combinations of flexibility, flame resistance, abrasion resistance, and environmental performance. However, PVC processing requires disciplined control. Excessive heat, excessive residence time, or unsuitable shear conditions may negatively affect the compound.
The hardened helical gear reducer and stable torque transmission system support consistent screw movement under varying loads. This is valuable when the machine transitions between different PVC formulations or cable sizes. A controlled conveying action can help limit process fluctuations and support steady output, provided that the material formulation, temperature profile, screw configuration, die design, and line settings are correctly selected for the application.
3.3 PE Processing
Polyethylene is used in a wide range of cable products due to its electrical properties, moisture resistance, chemical resistance, and processing flexibility. Different PE grades can have different melt flow behavior and mechanical characteristics. A stable extruder helps manufacturers adjust production parameters without losing control of the melt.
For PE insulation and jacketing, the relationship between screw speed, melt temperature, die geometry, cooling rate, and line speed is particularly important. A well-regulated extrusion system allows the operator to establish repeatable conditions for each product specification. Repeatability is important not only for product quality but also for reducing setup waste when changing from one cable size to another.
3.4 Advantages of One Flexible Platform
Multi-material compatibility can provide several practical advantages. It can reduce the need for duplicate equipment, make factory floor planning more efficient, and allow manufacturers to allocate production according to current orders. It can also support product diversification. A company that produces PVC power cables, PE communication cables, and PP-insulated specialty wires can use one adaptable extrusion platform instead of maintaining entirely independent processing systems.
Material flexibility must always be managed through appropriate process recipes. Operators should establish separate temperature profiles, screw speeds, pressure limits, die settings, and cooling conditions for each material and product. The value of a multi-material machine is therefore not that all materials run under identical settings, but that the equipment can provide a controlled operating foundation for different material requirements.
4. Precision Plasticization and Melt Stability
Plasticization is the transformation of solid polymer into a homogeneous melt that can be formed around a conductor. The quality of this transformation affects almost every downstream result. Poor plasticization may lead to surface defects, weak spots, unstable dimensions, or an inconsistent insulation layer.
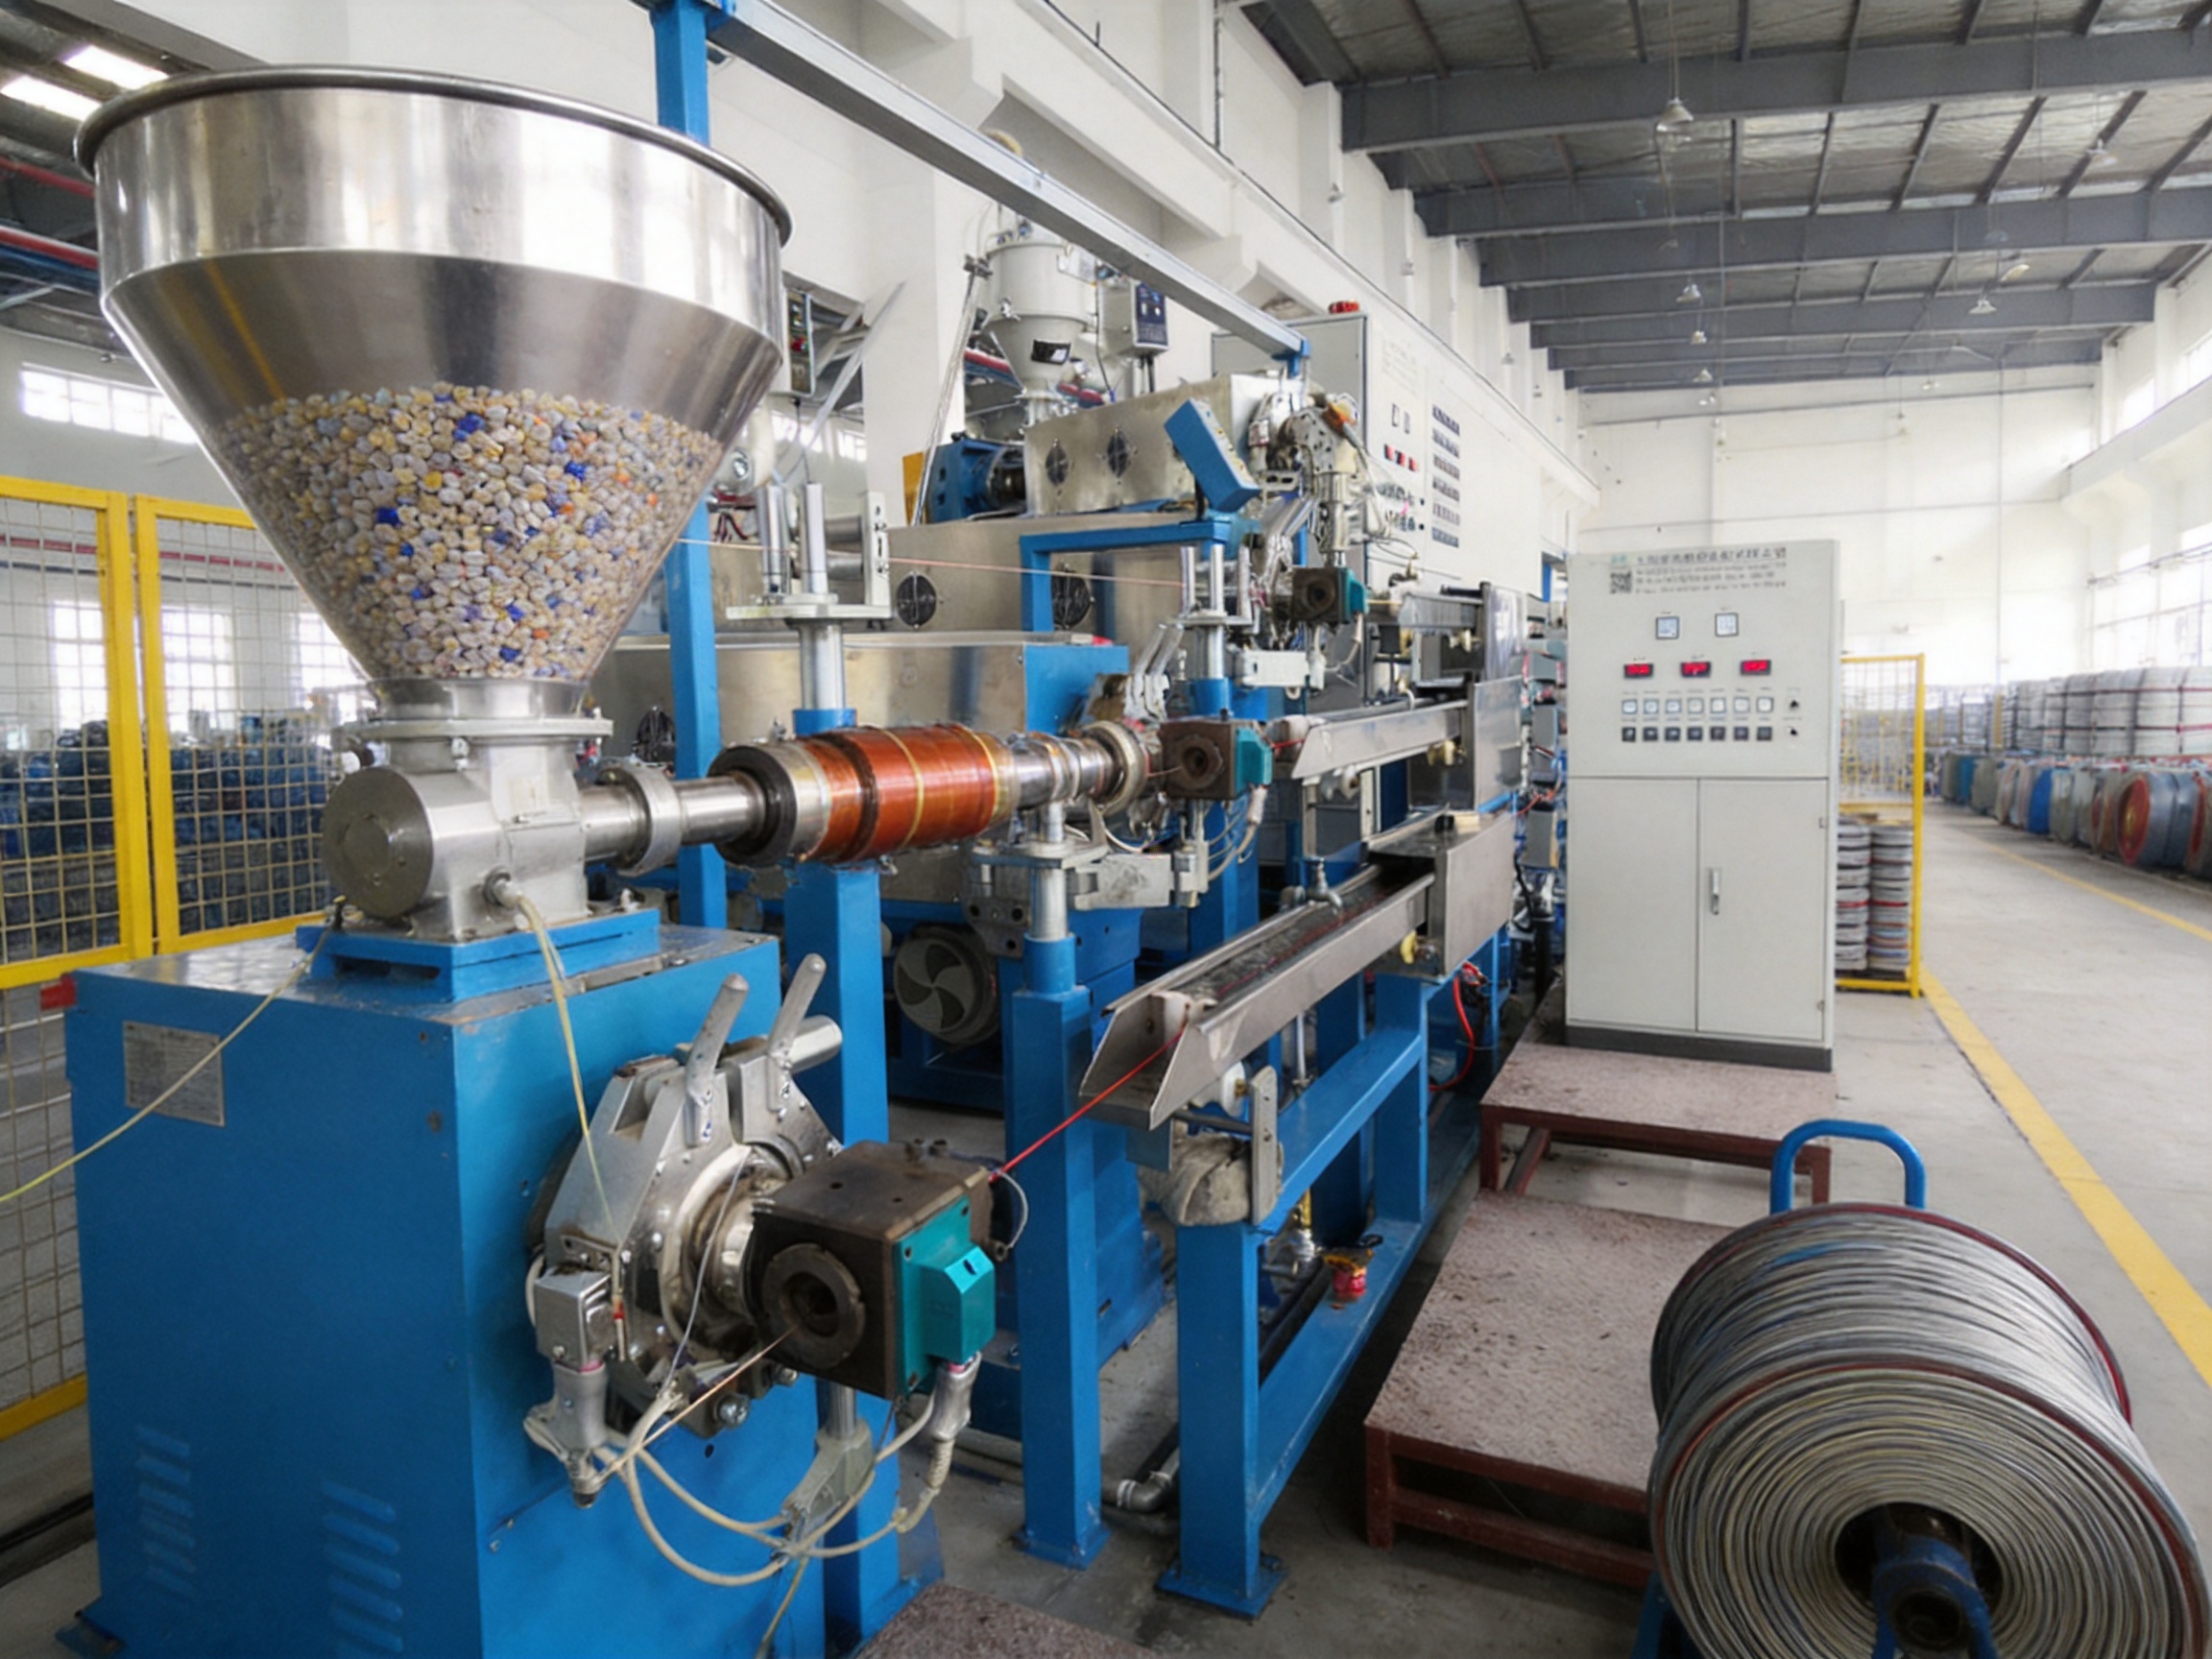
The High-Efficiency PP PVC PE Cable Extruder incorporates a precision plasticization system intended to improve melt uniformity. A stable plasticization process distributes heat and mechanical energy through the material while minimizing unnecessary fluctuation. This is especially important when processing compounds with different flow properties or when the production line operates for extended periods.
A uniform melt supports more consistent die flow. When the melt pressure and temperature remain stable, the crosshead can apply the coating more evenly around the conductor. This contributes to better concentricity and more predictable finished dimensions. It also helps reduce the amount of material that must be removed or downgraded because of visible surface irregularities.
Precision plasticization is closely connected to the screw and barrel system, heating control, cooling arrangements, feeding consistency, and reducer performance. No single component creates quality in isolation. The machine’s advantage comes from the coordinated operation of its mechanical and control systems.
For manufacturers, improved plasticization can deliver value in several ways. It can lower startup waste, reduce the frequency of process adjustments, support consistent insulation thickness, and make it easier to repeat established production recipes. These benefits become increasingly significant as cable sizes, materials, and customer specifications become more varied.
5. Torque Transmission and Hardened Helical Gear Reduction
Torque transmission is a fundamental part of extrusion performance. The screw must rotate with sufficient force to convey and plasticize the polymer under changing load conditions. If the drive system is inefficient or unstable, the machine may experience speed fluctuations, excess noise, increased wear, or reduced output consistency.
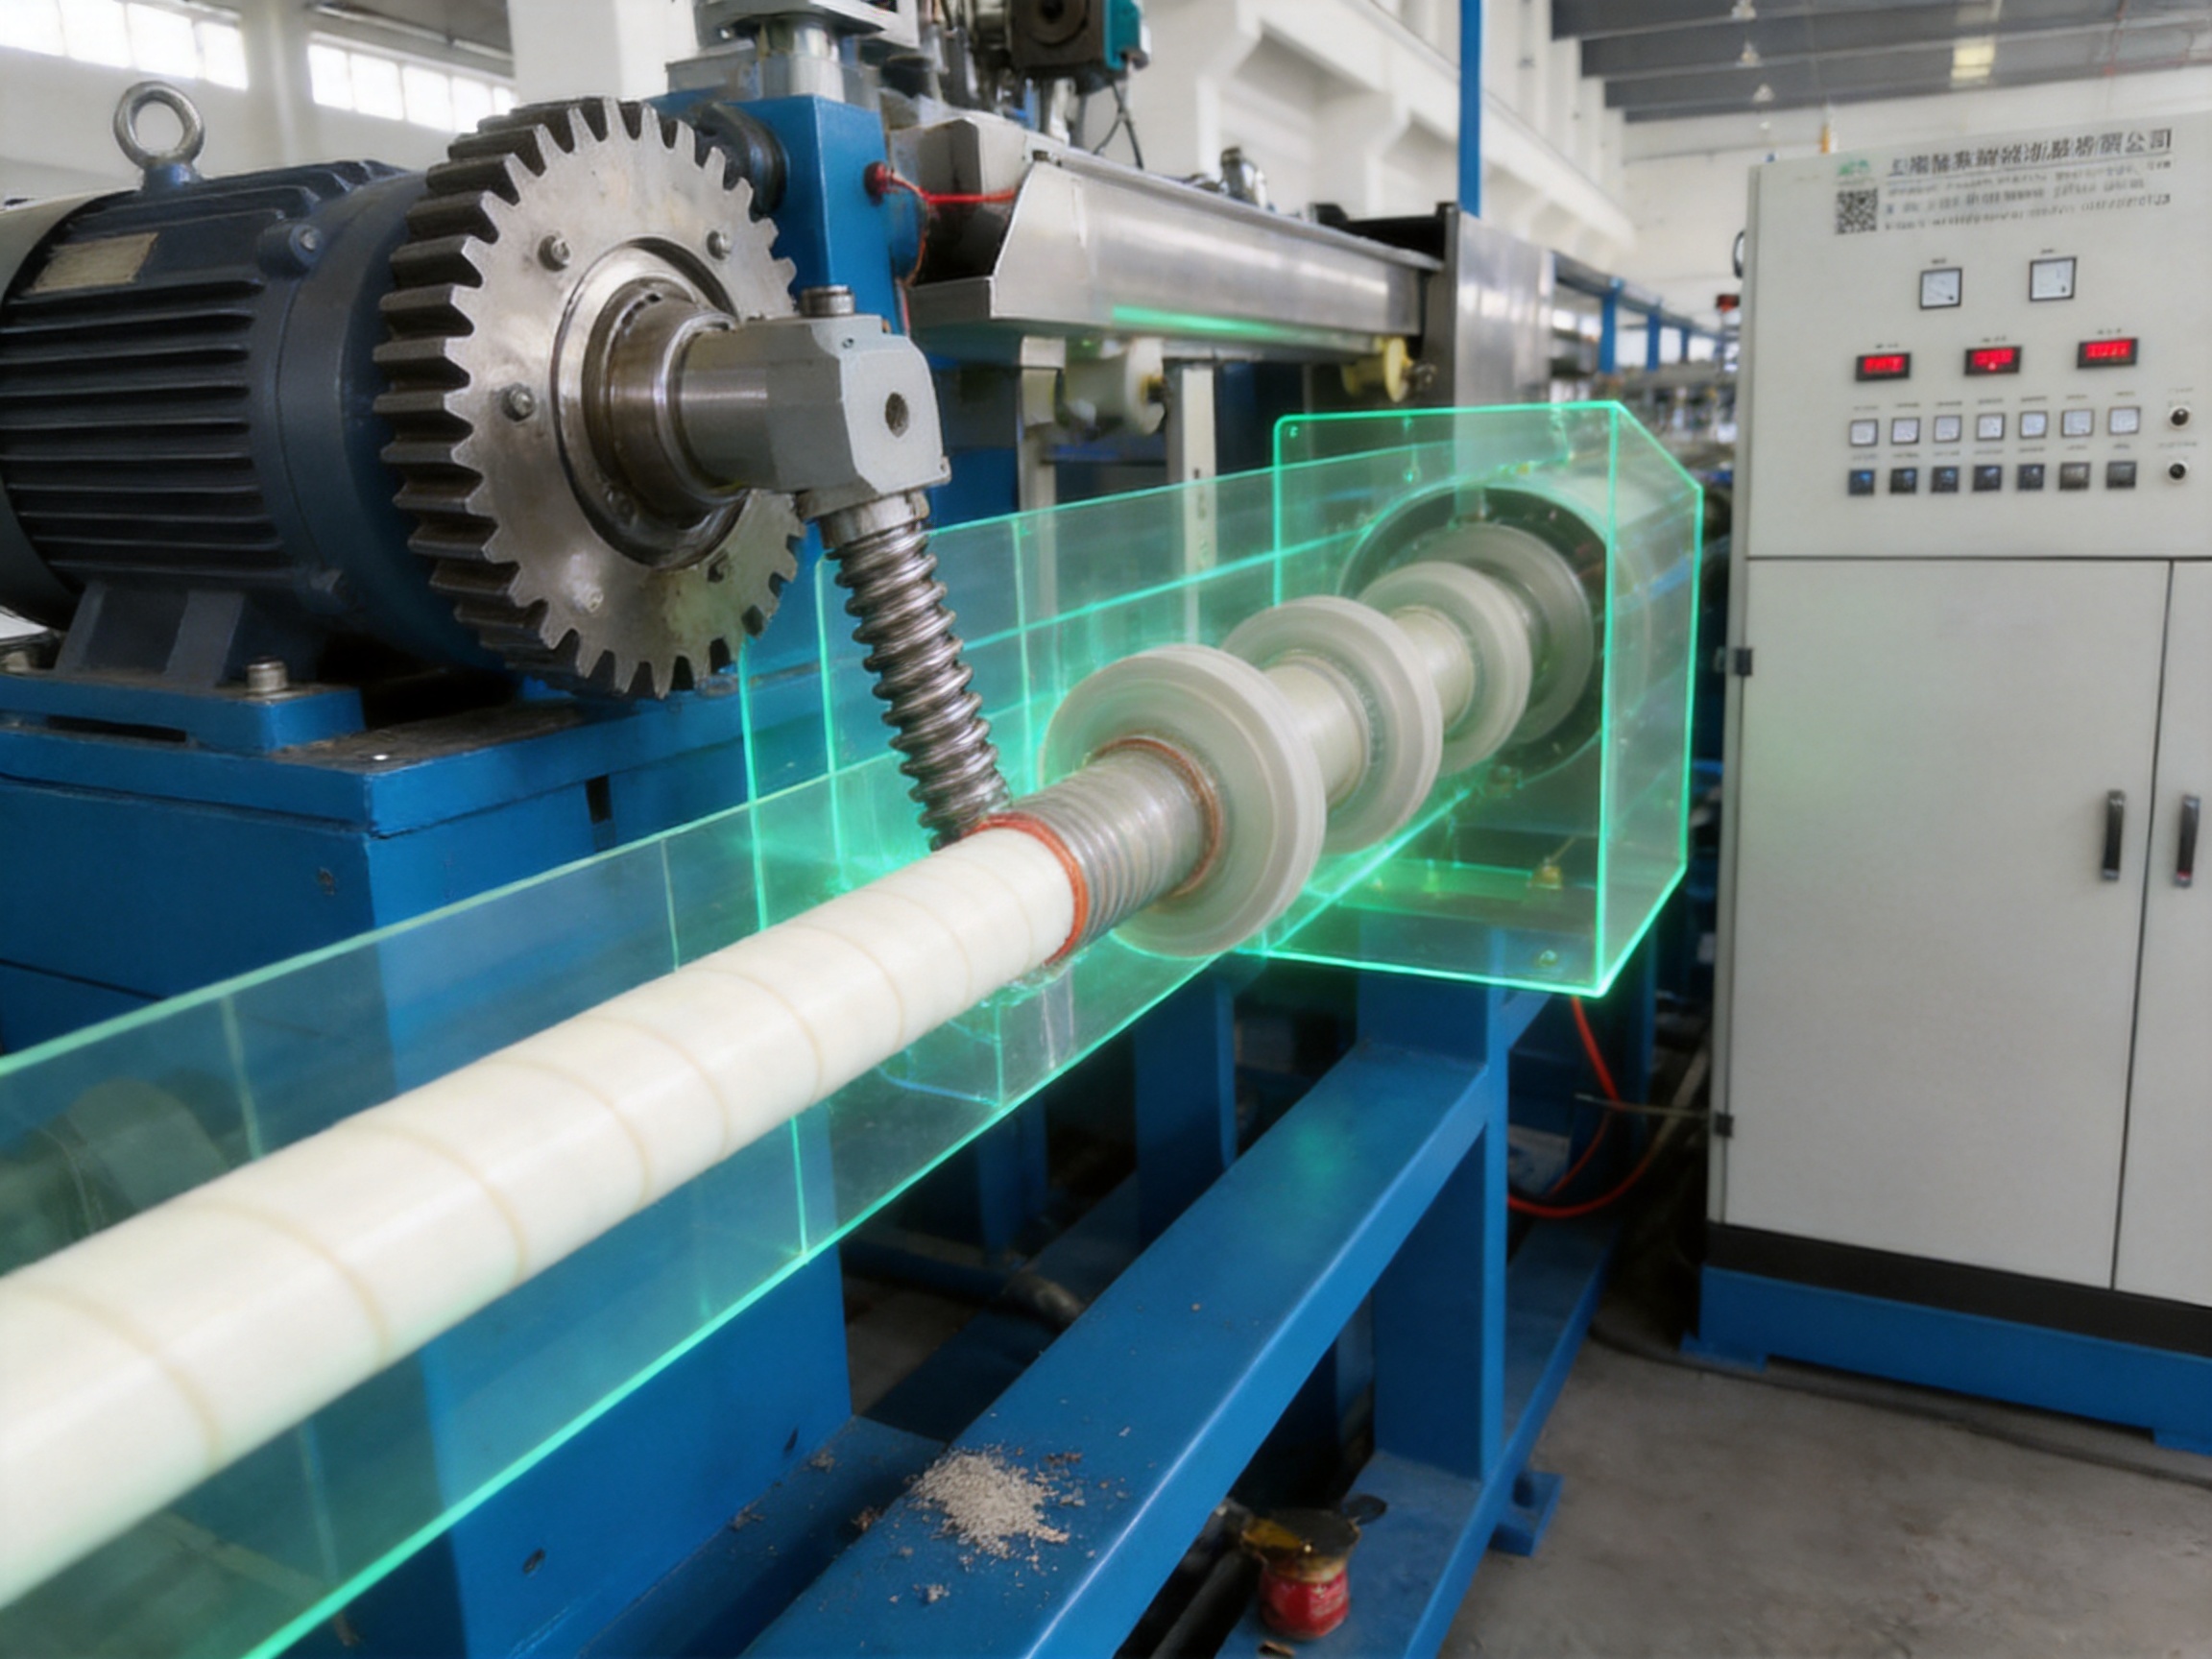
The use of a hardened helical gear reducer provides a robust transmission foundation. Helical gears are designed to engage progressively, which can support smoother torque transfer and lower vibration compared with less refined gear arrangements. Hardened gear surfaces are intended to improve resistance to wear under continuous operation.
In a cable extrusion environment, the reducer must operate reliably over long production periods. A stable drive system helps the screw maintain its intended speed even when material resistance changes. This is important when switching between PP, PVC, and PE, as well as when processing different cable diameters and compound formulations.
The reducer also contributes to the machine’s service value. Durable transmission components can help reduce unplanned stoppages and extend maintenance intervals when operated according to the manufacturer’s procedures. For a production manager, this translates into better equipment availability and more predictable scheduling.
Compared with a conventional system that may show greater speed fluctuation or less efficient power transfer, a hardened helical gear reducer can provide a stronger foundation for stable extrusion. The benefit is not limited to mechanical durability. Smooth torque delivery can also improve plasticization consistency and help the machine maintain a more uniform output.
6. Intelligent Power Regulation and Energy Management
Energy consumption is a major consideration in polymer processing. The extruder must supply heat to melt the polymer and mechanical energy to convey and plasticize it. If the drive or heating system operates inefficiently, unnecessary energy is consumed, operating costs rise, and the machine may generate excess heat that complicates process control.
The intelligent power regulation system is designed to adjust machine power according to operating demand. Rather than relying on a fixed, undifferentiated power profile, the equipment can regulate energy use as production conditions change. This approach can help support stable operation during startup, steady-state production, material changes, and output adjustments.
Intelligent regulation can be particularly valuable when the line is not running at its maximum capacity. A machine that operates efficiently across a range of output levels is more useful than one that performs well only at a single production point. Manufacturers often produce multiple cable sizes, and each product may require a different line speed and material throughput.
Energy management also affects the working environment and component life. Better-controlled power delivery may reduce unnecessary thermal variation and mechanical stress. It can help the operator maintain more consistent conditions and may contribute to a lower total cost of ownership over the equipment’s operating life.
Energy efficiency should be evaluated together with output, material utilization, product quality, maintenance, and downtime. A low-power machine that produces excessive waste is not necessarily economical. The High-Efficiency PP PVC PE Cable Extruder addresses efficiency more broadly by combining power regulation with stable conveying and improved material utilization.
7. Material Utilization and Cost Reduction
Raw material is one of the largest cost factors in cable production. Even a small reduction in polymer waste can create meaningful savings when production volumes are high. Waste may occur during startup, product changeover, unstable extrusion, off-center coating, incorrect diameter, damaged surfaces, or excessive process trimming.
The extruder is stated to improve material utilization by 15% compared with conventional models. This figure represents a significant potential advantage for manufacturers, particularly those producing large volumes or high-value compounds. Improved utilization means that a greater proportion of purchased polymer becomes saleable cable rather than startup scrap, downgraded product, or process waste.
Several design features can contribute to this result. Stable torque transmission helps maintain a consistent screw speed. Precision plasticization supports a more uniform melt. Intelligent power regulation helps maintain operating conditions across changing loads. Together, these features can reduce fluctuations that often cause unnecessary material consumption.
Material utilization also depends on the complete production line. A high-performing extruder should be coordinated with the conductor pay-off, crosshead, cooling system, diameter control, spark tester, capstan, and take-up equipment. If downstream tension is unstable or cooling is inconsistent, the final product may still require rework. For this reason, the extruder is most effective when integrated into a properly configured cable production system.
The financial impact can be assessed through a practical production review. A manufacturer can compare polymer input, saleable cable output, startup waste, changeover waste, and rejected product before and after installation. It can then calculate the effect of improved utilization on material cost per kilometer of cable. The result will vary according to polymer price, cable diameter, output volume, product mix, and operating discipline, but the economic opportunity is clear.
8. Output Capacity for High-Volume Production
The maximum stated output of the High-Efficiency PP PVC PE Cable Extruder is 240 kg/h for large-caliber cable applications. This capacity allows the machine to support demanding production schedules and high-volume orders. Output capability is particularly important for manufacturers that need to reduce the number of production shifts or increase capacity without adding a large number of separate lines.
High output must be matched with process stability. A machine that reaches a high theoretical rate but produces inconsistent cable at that speed may offer limited practical value. The combination of high throughput and controlled plasticization is therefore more important than nominal capacity alone.
Production managers should evaluate output according to the actual cable product. Required throughput may change with conductor size, insulation thickness, jacket thickness, material density, line speed, and quality requirements. The maximum output figure should be understood as an application-dependent capability rather than a universal operating rate for every product.
When correctly matched to the product and auxiliary equipment, a high-output extruder can improve factory productivity. It may reduce the time needed to complete large orders, support better asset utilization, and create additional capacity for product expansion. It can also help manufacturers respond more quickly to urgent orders without compromising established quality procedures.
9. Product Quality and Dimensional Consistency
Cable quality is determined by both electrical and physical performance. The insulation or jacket must provide a continuous protective layer with controlled thickness, suitable mechanical properties, and a clean surface. Dimensional consistency is essential because excessive thickness increases material cost, while insufficient thickness may compromise protection and compliance.
A stable extrusion system supports the production of consistent cable dimensions. Uniform melt flow helps the die maintain a predictable coating pattern. Stable screw rotation helps minimize output pulsation. Controlled line speed and coordinated take-up tension help prevent stretching or irregularity after the material leaves the die.
The High-Efficiency PP PVC PE Cable Extruder is designed to support these conditions through its precision plasticization and torque transmission systems. When integrated with suitable dies, cooling equipment, and monitoring devices, it can help manufacturers produce insulation and jackets with repeatable dimensions.
Surface appearance is another important quality indicator. Smooth, uniform surfaces are valued in many cable applications because they demonstrate controlled processing and reduce the risk of defects. A stable melt and properly adjusted temperature profile can help reduce roughness, lines, bubbles, and other visible imperfections.
Quality control should include dimensional measurement, visual inspection, spark testing where applicable, mechanical testing, electrical testing, and verification of the material formulation. The extruder provides the production foundation, but complete quality assurance depends on the entire process and the manufacturer’s control system.
10. Compliance-Oriented Cable Production
The equipment is described as compliant with IEC 60228 and ASTM D2240 standards. These references are relevant to cable conductor and material-related testing requirements, but manufacturers should always confirm the exact standards applicable to their product, market, material formulation, and customer specification.
IEC 60228 is associated with conductors of insulated cables and provides requirements related to conductor classification and resistance characteristics. ASTM D2240 is commonly associated with the measurement of rubber and plastic hardness using durometer methods. The inclusion of these standards in the product positioning indicates that the machine is intended for professional cable manufacturing environments where process control and product verification are important.
Compliance is not achieved by the extruder alone. It requires suitable raw materials, qualified conductor construction, correct die selection, controlled processing parameters, calibrated test equipment, documented procedures, and traceable inspection records. Nevertheless, a stable extrusion platform is an important part of building a compliant production process.
Manufacturers should work with their technical teams to establish product-specific process windows. These may include insulation thickness, conductor diameter, jacket dimensions, tensile properties, elongation, hardness, aging performance, electrical resistance, spark-test voltage, and other requirements. The extruder can then be configured and operated to support these targets.
11. Advantages Compared with Conventional Extruders
11.1 Broader Material Flexibility
Many conventional extrusion arrangements are optimized for a limited material range. The ability to process PP, PVC, and PE on one platform gives the High-Efficiency extruder a competitive advantage for factories with varied product portfolios. It can reduce the need for dedicated machines and support more flexible production planning.
11.2 Improved Material Economy
The claimed 15% improvement in material utilization is one of the machine’s most important competitive features. Conventional equipment may create higher waste during startup, changeover, or unstable operation. Better plasticization and control can help manufacturers reduce the amount of polymer consumed per unit of saleable cable.
11.3 Stable Operation under Changing Loads
The hardened helical gear reducer and advanced torque transmission system are intended to maintain smooth screw operation when material resistance changes. This is beneficial when switching between polymers with different structures or when adjusting production for different cable diameters.
11.4 Higher Production Potential
With output of up to 240 kg/h for large-caliber cables, the machine is positioned for high-volume production. A higher practical throughput can improve factory productivity and help manufacturers meet demanding delivery schedules.
11.5 Integrated Efficiency
The product does not rely on a single headline feature. Its competitive value comes from the combined effect of torque transmission, plasticization, power regulation, multi-material capability, and high output. This integrated approach is more valuable than a machine that offers high speed but lacks process stability or material economy.
11.6 Suitability for Turnkey Production
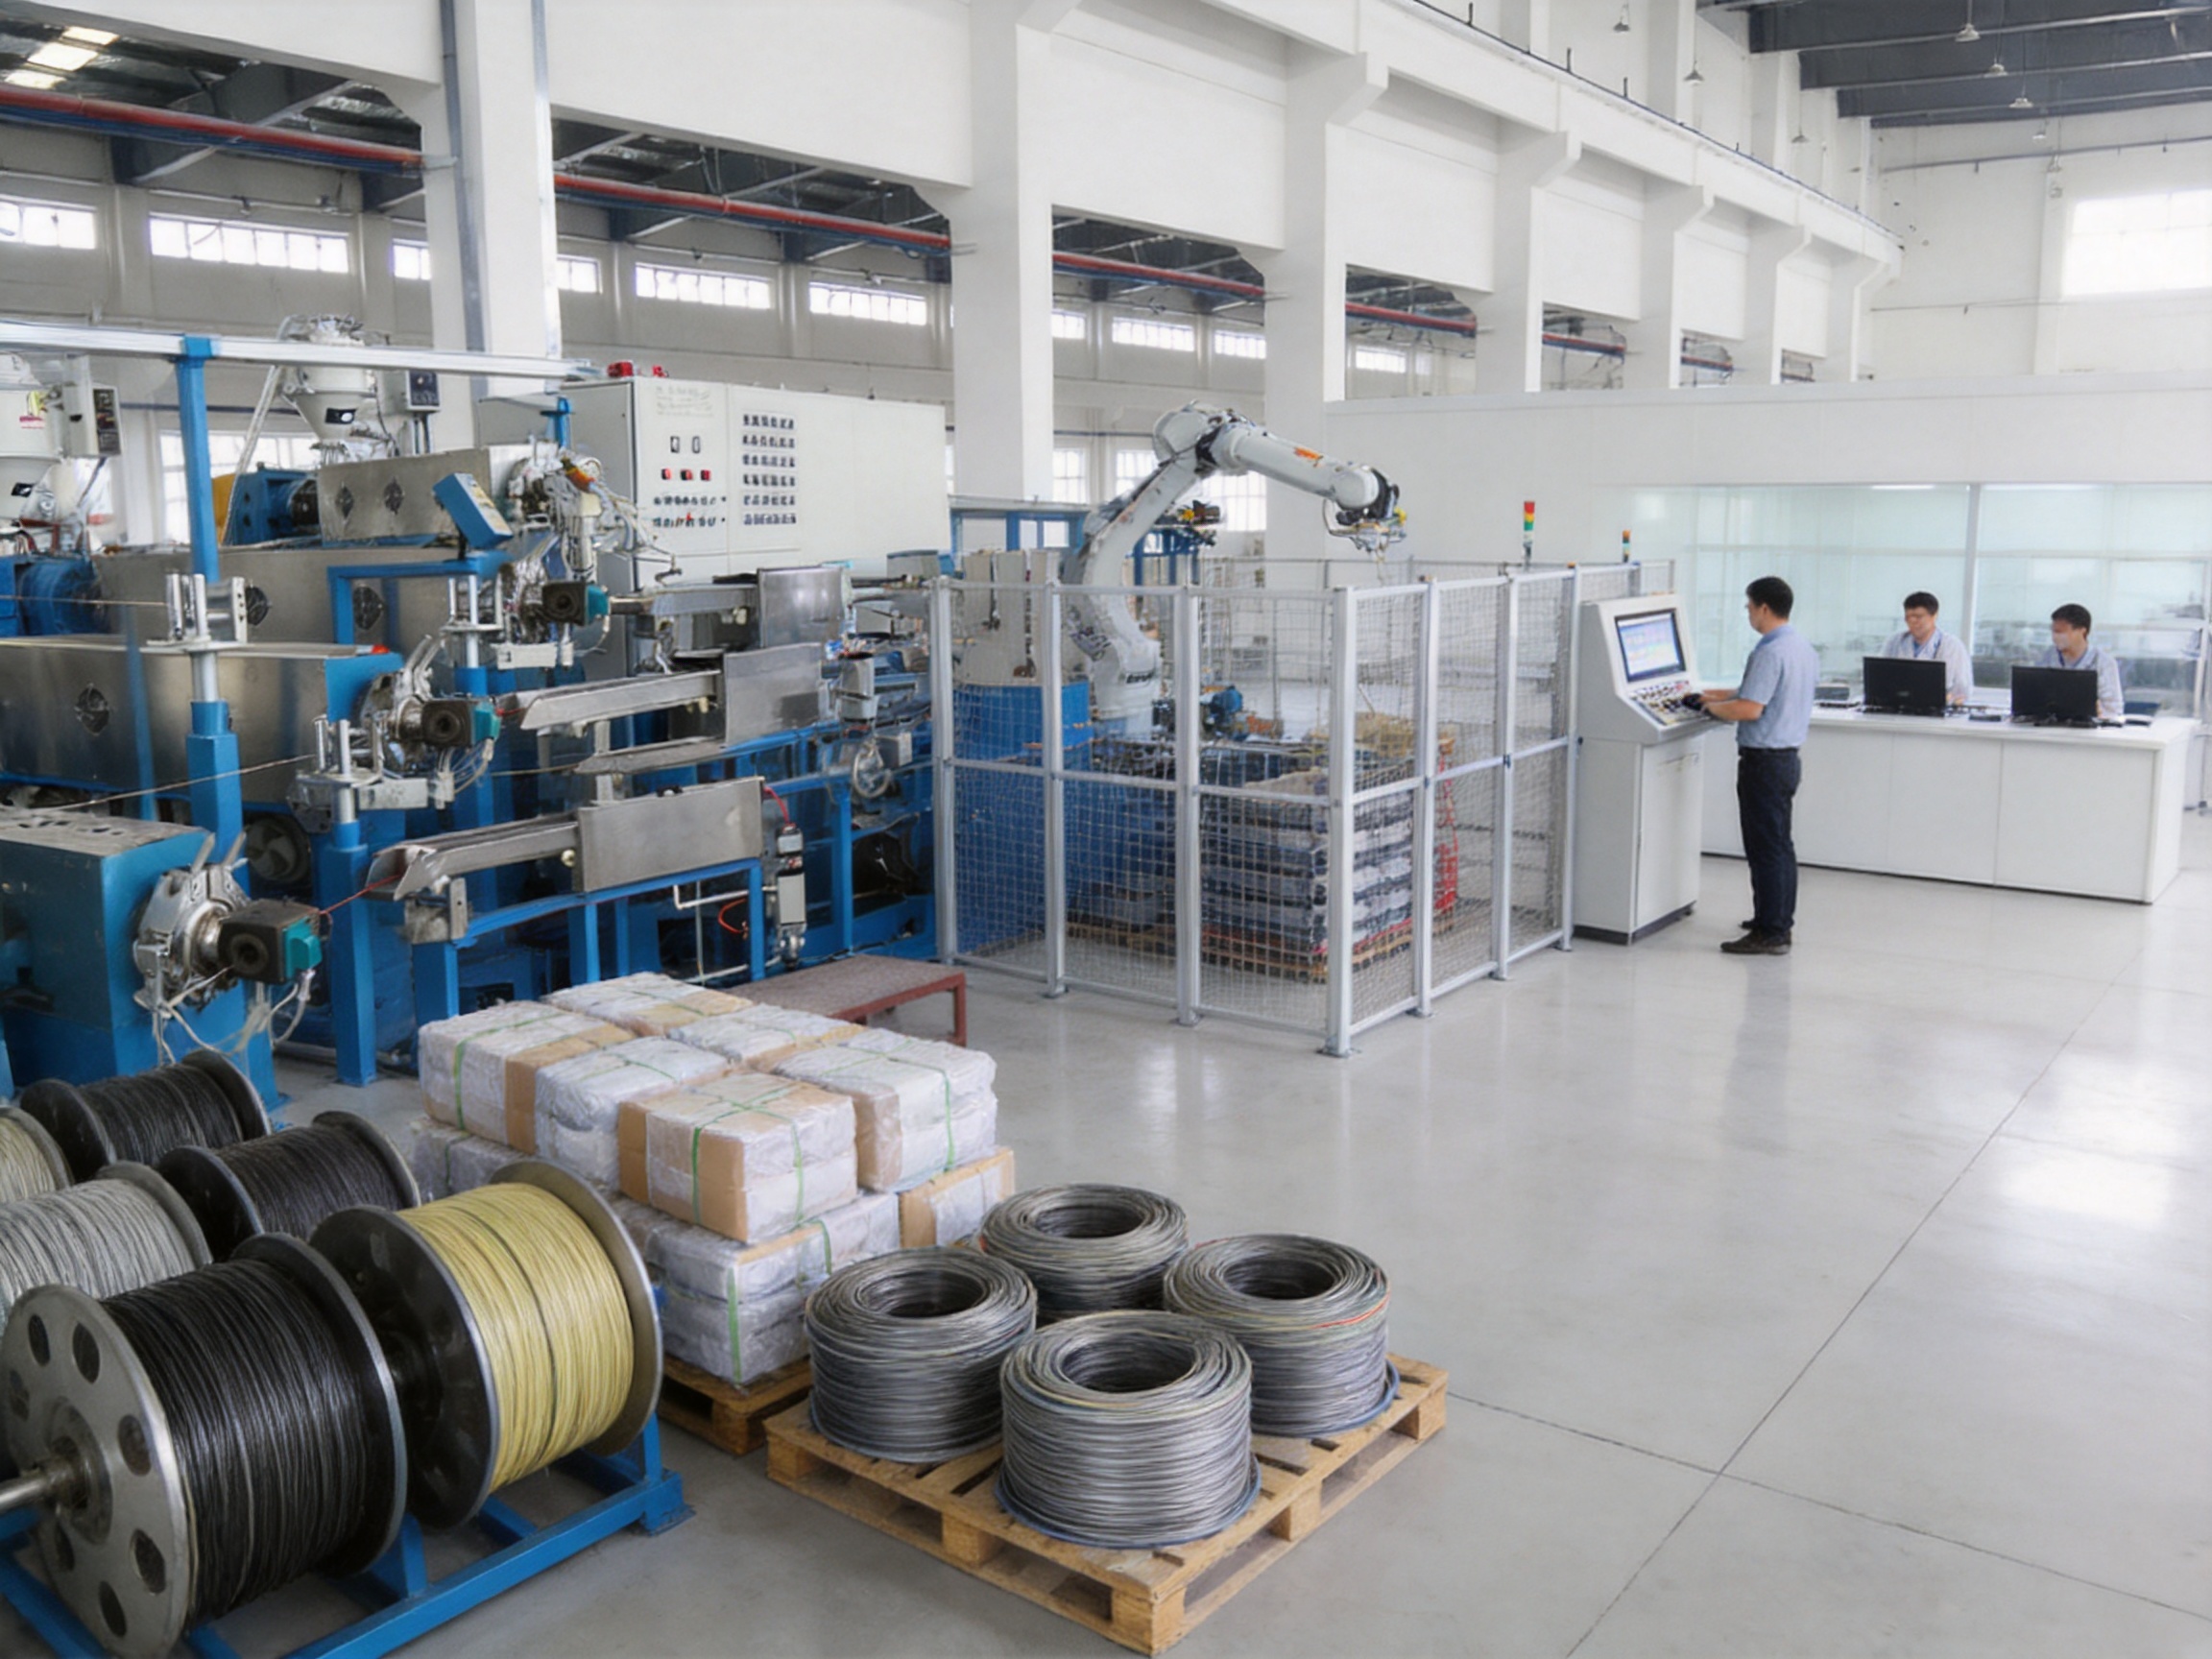
As part of a broader wire and cable machinery portfolio, the extruder can be combined with motorized pay-off equipment, motorized take-up equipment, coiling machines, fully automatic coiling and packaging equipment, intelligent robot stackers, and accessory equipment. This allows manufacturers to develop a more complete production workflow from conductor feeding through finished product handling.
12. Advanced Manufacturing Strengths Behind the Equipment
The performance of an industrial machine depends heavily on how it is designed, manufactured, assembled, tested, and supported. Shanghai Yessjet Precise Machinery Co., Ltd. develops equipment for wire and cable production, including extrusion lines and related automation systems. Its product range indicates a focus on complete production solutions rather than isolated components.
A machinery supplier with capabilities across extrusion, pay-off, take-up, coiling, packaging, stacking, and accessories can approach a production line as an integrated system. This is important because cable manufacturing equipment must operate in coordination. Line speed, tension, material flow, cooling, length measurement, coiling, and packaging all influence the final result.
The company’s emphasis on precise machinery is reflected in the product’s focus on torque transmission, plasticization, power regulation, and material utilization. These are areas where manufacturing accuracy and assembly quality directly affect field performance. A reducer, screw system, drive assembly, or control cabinet must be built and aligned correctly to deliver the intended operating stability.
Advanced manufacturing strength also includes application understanding. Different cable products require different combinations of extrusion temperature, line speed, die dimensions, cooling, take-up tension, and inspection. A supplier that understands these relationships can help customers choose a suitable configuration rather than simply offering a standard machine without considering the production target.
The company’s location in Jiangsu Province, China, places it within a region known for industrial manufacturing and machinery supply networks. Access to industrial components, machining resources, electrical control technologies, and engineering labor can support the development and production of specialized cable equipment.
For an equipment buyer, manufacturing strength should be evaluated through technical documentation, machine testing, component specifications, quality records, installation support, spare-parts availability, and after-sales service. These factors help determine whether the equipment can provide reliable value over its full service life.
13. Integration into a Complete Cable Production Line
The extruder is normally one part of a larger line. A typical cable coating process may begin with a motorized pay-off that supplies the conductor at controlled tension. The conductor passes through guiding and centering components before entering the extrusion crosshead. The polymer is melted and applied around the conductor, after which the cable passes through a cooling section.
Following cooling, the cable may pass through a diameter measuring device, spark tester, length counter, capstan, and take-up system. Depending on the product, it may then be wound into coils, transferred to a packaging machine, or handled by a robotic stacking system.
The motorized pay-off must provide smooth unwinding without sudden tension changes. The take-up system must collect the finished cable without damaging the surface or changing its dimensions. Coiling and packaging equipment should maintain consistent coil geometry and protect the product during storage and transportation.
The High-Efficiency PP PVC PE Cable Extruder can serve as the central processing unit in this arrangement. Its value increases when the connected machines communicate effectively and are matched to the extrusion rate. An oversized extruder connected to inadequate downstream equipment may create bottlenecks, while insufficient pay-off or take-up capacity can limit the entire line.
A complete solution also simplifies responsibility during installation and commissioning. When major equipment is supplied by one experienced machinery partner, technical coordination may be more straightforward. Line layout, speed matching, control interfaces, safety arrangements, and production testing can be planned as a unified project.
14. Operational Workflow
14.1 Preparation
Before production begins, operators should confirm that the selected polymer is suitable for the intended cable application and that the material is clean, correctly stored, and properly identified. The die, crosshead, screw configuration, and temperature zones should match the product specification.
The conductor path should be checked from the pay-off through the crosshead and cooling section to the take-up. Tension settings, guide alignment, safety guards, emergency stops, and monitoring instruments should be verified before heating begins.
14.2 Heating and Startup
The temperature zones should be brought to the appropriate settings for the selected polymer. Operators should allow sufficient time for the machine to reach thermal stability rather than starting production immediately after the display reaches a target value. Stable temperatures help reduce startup waste and improve the consistency of the first acceptable cable.
The screw should initially run at a controlled speed while material begins to fill the conveying and plasticization zones. Output should be increased gradually as the melt becomes stable. This approach helps protect the equipment and reduces the likelihood of sudden pressure changes.
14.3 Steady-State Extrusion
During normal production, operators should monitor melt pressure, temperature, screw speed, motor load, line speed, cable diameter, insulation eccentricity, and surface appearance. The intelligent power regulation system can support stable operation, but process monitoring remains essential.
Any change in material batch, conductor size, die, line speed, or insulation thickness should be treated as a process change. Operators should use approved production recipes and record the final settings for future runs.
14.4 Changeover
Material changes between PP, PVC, and PE require proper planning. The machine should be purged according to the supplier’s instructions, and the temperature profile should be adjusted for the new polymer. Residual material can affect color, surface quality, pressure, and plasticization if the transition is not managed carefully.
A controlled changeover can reduce waste and shorten downtime. The machine’s multi-material capability is most valuable when supported by clear procedures, trained operators, and well-organized material handling.
14.5 Shutdown and Maintenance
At the end of production, the extruder should be shut down according to the recommended sequence. Material remaining in the barrel and crosshead should be managed appropriately for the polymer in use. Operators should inspect the die, clean accessible areas, check for leakage, and record any unusual vibration, noise, pressure fluctuation, or temperature behavior.
Routine maintenance should include lubrication, inspection of the reducer, examination of heating and cooling components, verification of electrical connections, and checking of safety devices. Preventive maintenance helps preserve output stability and protects the investment in the equipment.
15. Automation, Labor Efficiency, and Production Management
Automation is becoming increasingly important in cable production because manufacturers must control labor costs while improving repeatability. The extruder’s intelligent power regulation contributes to process automation, while its potential integration with automated pay-off, take-up, coiling, packaging, and stacking equipment can support a more efficient factory workflow.
Automation reduces the number of manual interventions required during routine production. It can help maintain consistent line speed, coordinate connected machines, and reduce the risk of operator-related variation. Automatic data collection can also provide production records for traceability and performance analysis.
Labor efficiency does not mean removing the need for skilled operators. Instead, it allows operators to focus on process supervision, quality verification, recipe management, maintenance, and continuous improvement. A well-designed system can make technical work more productive by presenting important information clearly and responding quickly to changes.
For management teams, automation can also improve planning. Stable output makes it easier to estimate production time, material requirements, and delivery schedules. When the extruder is integrated with coiling and packaging systems, finished-product handling can be standardized from one order to the next.
16. Installation and Selection Considerations
Before purchasing the extruder, manufacturers should define their actual production requirements. Important questions include the cable diameter range, insulation and jacket materials, target output, conductor types, required line speed, product standards, available floor space, power supply, cooling-water capacity, and level of automation.
The machine should be selected according to the complete production line rather than as an isolated piece of equipment. The pay-off, crosshead, cooling trough, capstan, take-up, coiler, packaging unit, and control system must be compatible with the intended output.
Factory layout is also important. Sufficient space should be provided for raw material handling, operator access, die changes, maintenance, cooling systems, electrical cabinets, and finished cable handling. Proper access improves safety and reduces the time required for service work.
Installation should include mechanical alignment, electrical connection, control-system testing, heating verification, no-load operation, material trials, and product qualification. A structured commissioning process helps identify issues before full production begins.
Training should cover operation, recipe management, material changes, alarm response, cleaning, preventive maintenance, and safety. The performance of any extrusion machine depends partly on how effectively the operating team uses it.
17. Safety and Maintenance Priorities
Extrusion equipment includes rotating components, heated surfaces, pressurized polymer, electrical systems, and moving cable-handling devices. Safety guards, emergency stops, warning labels, interlocks, and operating procedures must be used correctly.
Operators should avoid contact with hot barrels, dies, and molten polymer. Appropriate personal protective equipment should be worn during material handling, die changes, cleaning, and maintenance. Lockout and isolation procedures should be followed before service work begins.
Maintenance priorities include the screw and barrel, reducer, motor, heating zones, temperature sensors, cooling components, electrical cabinet, control interface, crosshead, die, and cable-guiding components. A maintenance schedule should distinguish between daily inspections, weekly checks, periodic service, and major overhaul requirements.
Signs that require attention may include abnormal vibration, increasing motor load, unstable pressure, irregular temperature readings, unusual gear noise, material leakage, slow heating, or unexplained changes in cable dimensions. Early intervention can prevent a minor problem from becoming a production stoppage.
18. Return on Investment and Total Cost of Ownership
The purchase price of an extruder is only one part of its economic value. Manufacturers should also consider material consumption, energy use, output, labor, maintenance, spare parts, downtime, product quality, and the ability to process future orders.
The High-Efficiency PP PVC PE Cable Extruder can support return on investment through several channels. Its 15% material-utilization improvement may reduce polymer costs. Its output capacity may increase production volume. Its multi-material design may reduce the need for duplicate machines. Its torque transmission and hardened reducer may support long-term reliability. Intelligent power regulation may help lower energy use and stabilize operation.
A proper evaluation should compare the expected annual production volume with the present cost of material waste, energy, labor, rejected cable, maintenance, and downtime. It should also consider the value of increased flexibility. A machine that allows a factory to accept more product types may create revenue opportunities that are not visible in a simple energy calculation.
Total cost of ownership is influenced by the quality of installation, operator training, preventive maintenance, material handling, and spare-parts management. A strong equipment supplier should provide technical information that enables the buyer to plan these factors from the beginning.
19. Recommended Applications
The extruder is suitable for manufacturers producing cable insulation and jackets using PP, PVC, and PE. Potential applications include power cables, control cables, industrial wires, flexible cables, communication-related products, and other cable types whose material and dimensional requirements match the machine configuration.
It is particularly relevant for companies that need to change between different polymer families, produce multiple cable sizes, or reduce raw material waste. It can also support factories that are expanding from a single product line into a broader portfolio.
Large-caliber cable production may benefit from the stated output capacity of up to 240 kg/h. However, the final configuration should be selected based on the specific cable structure, polymer formulation, insulation thickness, conductor size, die system, and required line speed.
The equipment may be used by new cable factories establishing a production line or by existing manufacturers upgrading older extrusion equipment. In both cases, the greatest benefit is likely to come from a complete assessment of the current workflow and the desired production target.
20. Frequently Asked Questions
Q1: Which materials can the High-Efficiency PP PVC PE Cable Extruder process?
The machine is designed to process PP, PVC, and PE for cable insulation and jacketing applications. Each material requires its own temperature profile, screw speed, die setup, and cooling conditions. Manufacturers should confirm the appropriate configuration for the selected compound and cable product.
Q2: What is the maximum production output?
The stated maximum output is up to 240 kg/h for large-caliber cables. Actual output depends on material type, cable diameter, insulation or jacket thickness, line speed, die design, and the complete line configuration.
Q3: How does the machine improve material utilization?
The machine is designed with stable torque transmission, precision plasticization, and intelligent power regulation. These systems can reduce process fluctuation, startup waste, and off-specification production. The stated improvement in material utilization is 15% compared with conventional models.
Q4: Why is a hardened helical gear reducer important?
A hardened helical gear reducer provides a durable transmission structure for transferring motor torque to the extrusion screw. Its design supports smooth engagement, resistance to wear, reduced vibration, and stable screw operation under changing material loads.
Q5: Can one machine process both PP and PVC?
Yes, the machine is designed for both PP and PVC, as well as PE. However, operators must use material-specific process parameters and follow appropriate purging and changeover procedures when switching between polymers.
Q6: Is the machine suitable for a complete cable production line?
Yes. It can be integrated with pay-off equipment, take-up equipment, cooling systems, testing devices, coiling machines, packaging equipment, intelligent robot stackers, and other cable-production accessories. Correct matching of all line components is essential.
Q7: What quality standards are associated with the product?
The product is described as compliant with IEC 60228 and ASTM D2240 standards. Buyers should confirm the exact standards and testing requirements applicable to their cable products, materials, and target markets.
Q8: Does high output necessarily mean higher energy consumption?
Not necessarily. The machine combines high output potential with intelligent power regulation, which is intended to adjust energy use according to operating demand. Actual energy consumption depends on material, output, temperature settings, line speed, and operating conditions.
Q9: What information should a buyer provide when requesting a quotation?
A buyer should provide the cable type, conductor size, insulation or jacket material, finished diameter, coating thickness, target output, required line speed, voltage and frequency, level of automation, and any applicable standards. This information helps the supplier recommend a suitable configuration.
Q10: How can manufacturers protect long-term equipment performance?
Manufacturers should follow the operating manual, use suitable materials, maintain correct temperature and speed settings, perform preventive maintenance, inspect the reducer and drive system, keep the die and crosshead clean, and train operators in safe production and changeover procedures.
21. Why This Extruder Is a Practical Strategic Investment
The High-Efficiency PP PVC PE Cable Extruder is more than a basic polymer processing machine. It is a production platform intended to address several major challenges faced by cable manufacturers: material cost, product variety, energy management, output pressure, quality consistency, and equipment integration.
Its ability to process PP, PVC, and PE creates flexibility. Its precision plasticization system supports uniform melt preparation. Its advanced torque transmission and hardened helical gear reducer provide a stable mechanical foundation. Its intelligent power regulation contributes to efficient operation. Its stated 15% improvement in material utilization directly targets raw material costs, while its output capability of up to 240 kg/h supports high-volume production.
The machine’s value is strengthened by the broader capabilities of Shanghai Yessjet Precise Machinery Co., Ltd., which supplies wire and cable machinery and related turnkey production equipment. A supplier able to support extrusion, pay-off, take-up, coiling, packaging, stacking, and accessory systems can help manufacturers develop a more coordinated production solution.
For companies seeking to modernize their cable manufacturing operations, the most important consideration is not simply whether an extruder can melt polymer. The key question is whether it can deliver stable, efficient, repeatable, and adaptable production within the complete factory workflow. The High-Efficiency PP PVC PE Cable Extruder is designed around these requirements and offers a strong foundation for manufacturers pursuing lower production costs and more competitive cable output.
22. Conclusion
Modern cable production requires equipment that combines flexibility, precision, efficiency, and reliability. A cable extruder must process different polymers, maintain stable output, minimize waste, protect product quality, and integrate smoothly with upstream and downstream machinery.
The High-Efficiency PP PVC PE Cable Extruder addresses these priorities through its compatibility with PP, PVC, and PE; precision plasticization system; advanced torque transmission; hardened helical gear reducer; intelligent power regulation; and high output capability. Its stated 15% improvement in material utilization and maximum output of 240 kg/h give manufacturers measurable targets for improving productivity and cost control.
When supported by proper line design, qualified materials, trained operators, preventive maintenance, and appropriate testing, the machine can become a central asset in a modern wire and cable factory. Its combination of multi-material capability and integrated efficiency makes it suitable for manufacturers that want to expand product range, reduce waste, and establish a more streamlined production workflow.
References
International Electrotechnical Commission. IEC 60228: Conductors of Insulated Cables.
ASTM International. ASTM D2240: Standard Test Method for Rubber Property—Durometer Hardness.
General principles of polymer extrusion processing, screw conveying, plasticization, melt pressure control, and die forming.
Industrial practices for wire and cable insulation, jacketing, cooling, dimensional control, spark testing, coiling, and packaging.
Technical product information for the High-Efficiency PP PVC PE Cable Extruder supplied by Shanghai Yessjet Precise Machinery Co., Ltd.