LANGUAGE
 中文简体
 русский
 Français
 Español
 Português
 عربى
Content
- 1 What Is a Wire and Cable Extrusion Line?
- 2 Why an Integrated Production Line Is Superior to Disconnected Equipment
- 3 Main Components of a Modern Cable Extrusion Line
- 3.1 Motorized Pay-Off Equipment
- 3.2 Straightening Stand
- 3.3 Extrusion Machine
- 3.4 Crosshead and Die Assembly
- 3.5 Electrical Control and Operation Cabinet
- 3.6 Cooling System
- 3.7 Outer Diameter Measuring Instrument
- 3.8 Ink Printing Machine
- 3.9 Haul-Off and Tension Control
- 3.10 Take-Up, Coiling, and Packaging Equipment
- 4 Material-Specific Extrusion Performance
- 5 Representative Extruder Models and Output Range
- 6 How Screw Design Influences Product Quality
- 7 Temperature Control and Process Stability
- 8 Diameter Control, Eccentricity, and Quality Assurance
- 9 Advanced Manufacturing Strengths
- 10 Advantages Compared with Basic or Incompatible Competitor Systems
- 11 Automatic Coiling and Robotic Stacking Integration
- 12 Operating and Maintenance Recommendations
- 13 How to Select the Correct Line Configuration
- 14 Applications of Wire and Cable Extrusion Lines
- 15 Frequently Asked Questions
- 15.1 What materials can be processed on the line?
- 15.2 How is the extruder model selected?
- 15.3 Can the line produce both insulation and cable jackets?
- 15.4 Why is tension control important?
- 15.5 Can outer diameter control guarantee uniform insulation thickness?
- 15.6 What is the purpose of multiple barrel heating zones?
- 15.7 Can automatic coiling be added later?
- 15.8 Does the company provide complete production-line solutions?
- 15.9 Can older cable extrusion equipment be upgraded?
- 15.10 What information should be included in an equipment inquiry?
- 16 Conclusion
- 17 References
- 18 Product: Wire And Cable Extrusion Line
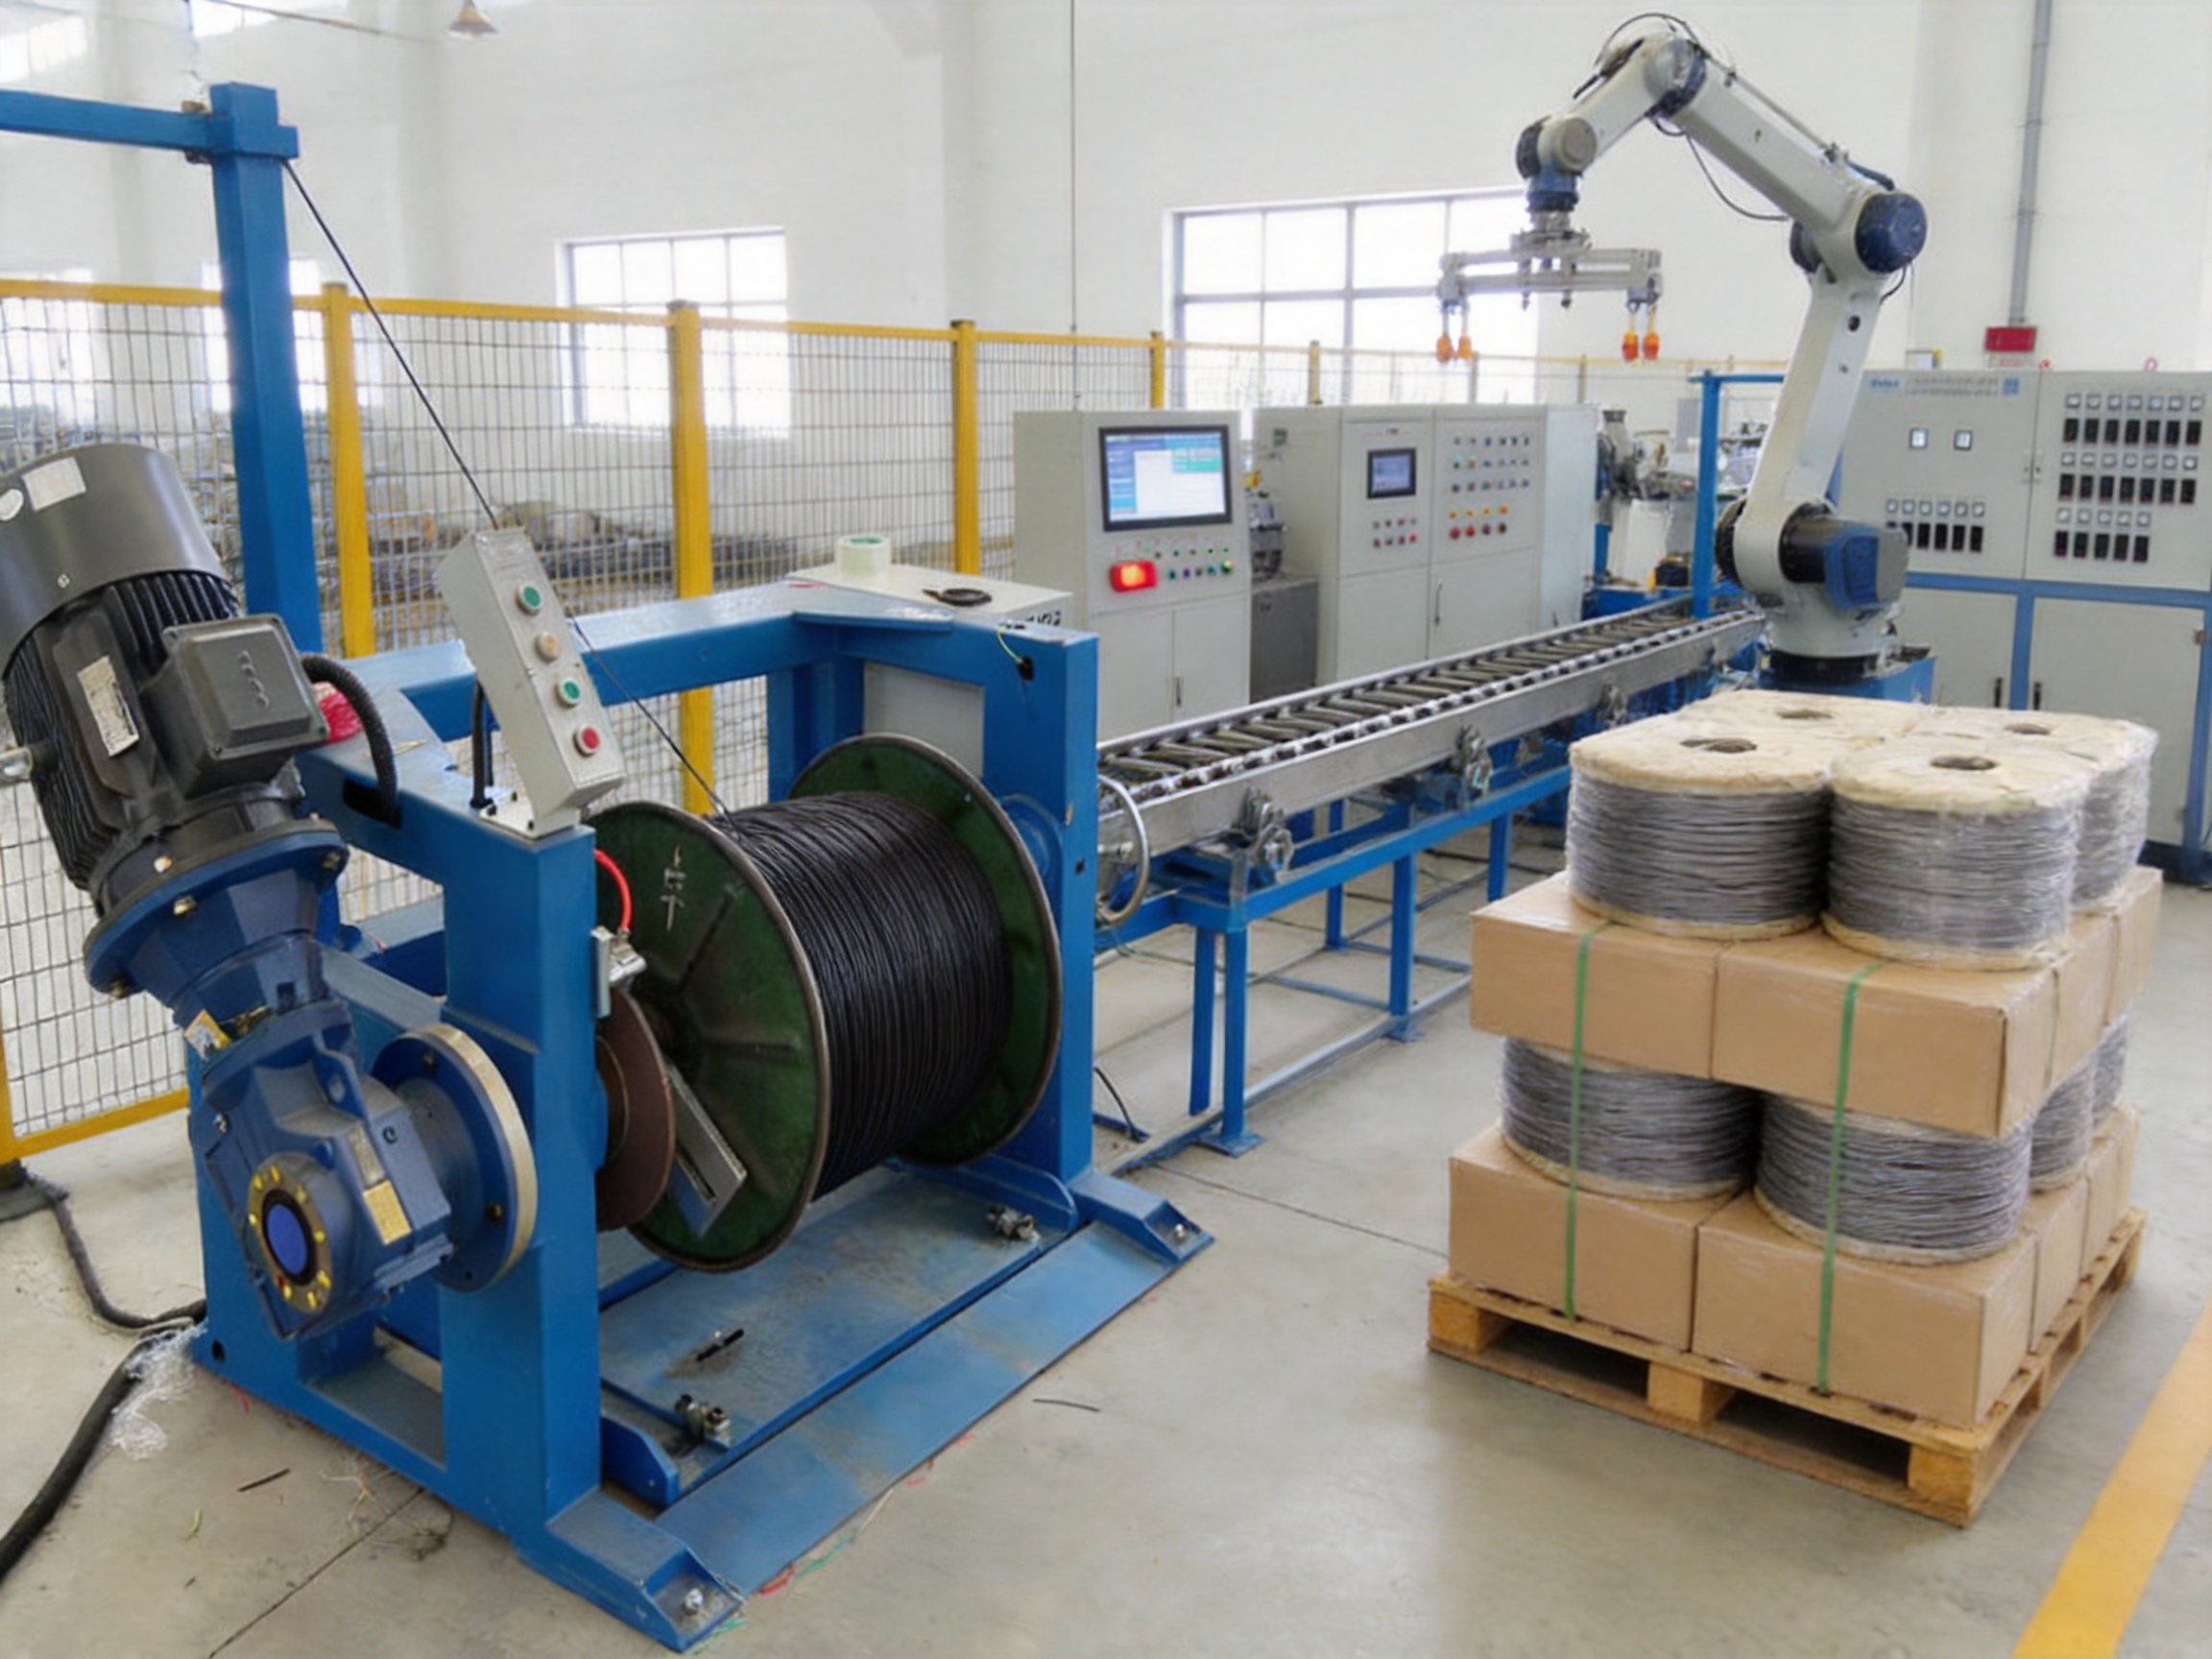
Wire and cable manufacturing demands far more than a conventional plastic extruder. A modern production line must coordinate conductor pay-off, straightening, insulation or jacketing, diameter measurement, cooling, printing, tension management, take-up, and final packaging with stable accuracy. When these processes are properly integrated, manufacturers can produce cables with consistent insulation thickness, reliable electrical performance, clean surfaces, controlled winding, and repeatable production efficiency.
A complete wire and cable extrusion line is therefore both a processing machine and a coordinated manufacturing system. The extruder determines how effectively the polymer is melted and homogenized, while the crosshead, cooling section, haul-off, measurement systems, and take-up equipment determine whether the finished product meets dimensional and appearance requirements. The quality of the final cable depends on the interaction of every section rather than on the extruder alone.
Shanghai Yessjet Precise Machinery Co., Ltd. develops and supplies wire and cable machinery, cable extrusion line solutions, coiling systems, motorized pay-off and take-up equipment, and related automation. Its equipment can be configured for different conductor sizes, insulation materials, production speeds, output targets, and end-of-line requirements. This approach enables cable manufacturers to purchase an integrated solution instead of assembling incompatible equipment from multiple suppliers.
What Is a Wire and Cable Extrusion Line?
A wire and cable extrusion line is an automated production system used to apply an insulating, protective, or jacket material around a conductor. Depending on the application, the conductor may be solid copper, stranded copper, aluminum, tinned wire, or another conductive core. The polymer may include PVC, polyethylene, low-smoke zero-halogen compounds, nylon, Teflon-based materials, or other engineering thermoplastics.
During operation, the conductor is unwound from a pay-off stand and guided through the production line. The extruder receives plastic pellets or compound, melts and mixes them, and delivers the material to a crosshead die. The crosshead centers the molten polymer around the moving conductor. The coated wire then passes through cooling water, measuring devices, printing equipment, a haul-off, and a take-up unit. Depending on the product, the final cable may be wound onto a reel, coiled into a compact package, or transferred to an automated packaging system.
Each machine section has a defined responsibility:
- The pay-off stand supplies the conductor at a controlled speed and tension.
- The straightening stand removes unwanted curvature and helps maintain a stable entry path.
- The extruder plasticizes and meters the insulation or jacket compound.
- The crosshead applies the polymer concentrically around the conductor.
- The electrical control cabinet coordinates speed, temperature, alarms, interlocks, and production data.
- The outer diameter measuring instrument monitors the finished cable dimension.
- The pre-cooling tank begins solidification immediately after extrusion.
- The ink printer applies identification marks, standards, dates, or customer information.
- The main cooling tank completes polymer solidification.
- The haul-off or dual-wheel pulling unit transports the cable through the line at a controlled speed.
- The storage and tension sections stabilize the material before winding.
- The take-up machine winds the finished cable onto a reel or into a controlled package.
This arrangement allows the line to operate continuously. The operator can set the product recipe, target diameter, line speed, temperature profile, and take-up parameters through the control interface. Once the process reaches stable conditions, closed-loop measurement and coordinated drives help reduce manual adjustment and minimize material waste.
Why an Integrated Production Line Is Superior to Disconnected Equipment
Many cable producers begin with individual machines purchased from different sources. Although this may appear less expensive at the beginning, disconnected equipment often creates compatibility problems. Drive systems may respond differently, communication protocols may not match, and the operator may need to control several unrelated interfaces. Tension instability, inaccurate meter counting, poor synchronization, and difficult troubleshooting can reduce the practical output of the entire plant.
An integrated wire and cable extrusion line is designed around a common process objective. The pay-off, extruder, haul-off, measuring unit, printer, and take-up operate according to coordinated speed references. The line control system can also include alarm logic, emergency stops, recipe storage, temperature monitoring, and production data functions. These features reduce the number of manual decisions required during normal production.
The main advantages of an integrated system include:
- Improved synchronization between conductor speed, extrusion output, and take-up speed.
- More stable insulation wall thickness and outer diameter.
- Reduced risk of conductor stretching caused by excessive pulling tension.
- More consistent cooling and surface quality.
- Faster product changeovers through stored recipes and centralized settings.
- Reduced commissioning difficulty because the line is engineered as a complete system.
- Simpler maintenance and troubleshooting through unified electrical documentation.
- Greater flexibility for future coiling, packaging, and robotic palletizing upgrades.
Compared with basic extrusion equipment, the Yessjet approach emphasizes the entire production workflow. The objective is not simply to supply an extruder with an attached cooling tank. The objective is to provide a production line that can be adapted to the customer’s material, conductor construction, finished diameter, output target, packaging method, and factory layout.
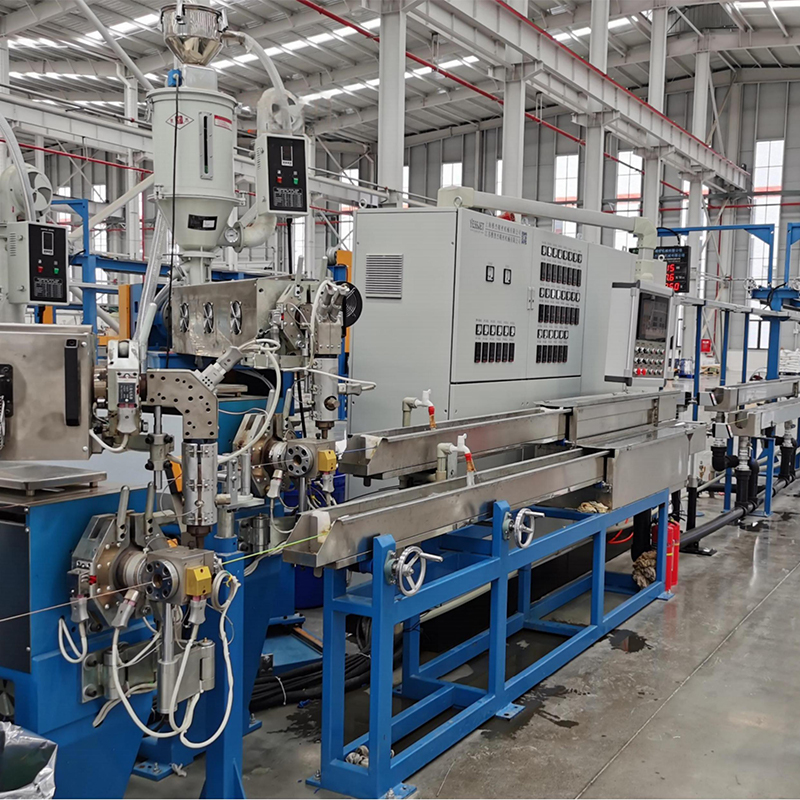
Wire And Cable Extrusion Line
Main Components of a Modern Cable Extrusion Line
Motorized Pay-Off Equipment
The pay-off is the starting point of the line and has a direct influence on downstream stability. A pay-off that releases the conductor irregularly can create tension fluctuations, conductor oscillation, and changes in insulation concentricity. For this reason, the motorized pay-off must be selected according to the conductor diameter, reel size, conductor weight, line speed, and required tension range.
Modern motorized pay-offs use controlled drive systems to unwind the conductor smoothly. Tension feedback, dancer systems, or other control methods can be used to maintain a consistent supply. When the pay-off and haul-off are correctly coordinated, the conductor enters the crosshead with fewer disturbances, allowing the polymer to form a more uniform layer around the core.
The equipment can be configured for different reel dimensions and production conditions. Safety guarding, emergency stop functions, reel clamping, and guided threading improve operator protection and reduce setup time. For manufacturers producing several cable types, the pay-off design can be selected to simplify reel changes and accommodate different conductor packages.
Straightening Stand
Conductors stored on reels may develop curvature or lateral movement. A straightening stand uses guide rollers or forming elements to reduce this effect before the conductor enters the extrusion crosshead. Straightening is especially important when the line is producing small-diameter wires or cables that require accurate concentricity.
A properly adjusted straightening system prevents the conductor from moving unevenly through the die. It also helps reduce contact between the conductor and internal crosshead components. The result is a more stable coating process and less risk of surface defects caused by an irregular conductor path.
Extrusion Machine
The extrusion machine is the central processing unit. It receives polymer material, conveys it through the barrel, melts it, mixes it, and delivers a stable melt flow to the crosshead. The barrel and screw design must match the compound being processed. PVC, polyethylene, LSZH, Teflon-based materials, nylon, and other polymers have different melting behavior, viscosity, thermal sensitivity, and processing windows.
Yessjet extrusion machines can be equipped with imported barrel and screw components from Taiwan, depending on the selected configuration. The available screw designs and machine models support different output requirements. A suitable screw geometry improves plasticization, melt homogeneity, and output stability. It also helps reduce unmelted particles, excessive shear heating, and fluctuations in melt pressure.
The machine uses independently controlled heating zones. Temperature controllers, solid-state relay circuits, and programmable control functions help maintain process stability. The supplied reference specifies temperature deviation of approximately plus or minus 2 degrees Celsius under suitable operating conditions. Actual performance depends on material, ambient conditions, machine configuration, calibration, and operating practice.
Crosshead and Die Assembly
The crosshead applies molten polymer around the conductor. Its geometry, die design, centering adjustment, and melt channel condition influence concentricity and surface appearance. A correctly selected die must correspond to the conductor size, target insulation thickness, compound type, and production speed.
Die centering is essential because outer diameter alone does not confirm wall thickness uniformity. If the conductor is not centered correctly, one side of the insulation may become thinner even when the measured outside diameter remains within the nominal range. A stable crosshead structure and accurate adjustment mechanism therefore contribute directly to product reliability.
Electrical Control and Operation Cabinet
The electrical control cabinet serves as the coordination center of the line. A programmable logic controller manages sequence logic, drive communication, alarms, safety interlocks, temperature signals, and auxiliary equipment. An operator interface can display line speed, extruder speed, temperature zones, measured diameter, alarm status, and production parameters.
Centralized control provides several advantages over individually operated machines. Operators can start and stop the line according to a defined sequence, preventing premature material flow or uncontrolled conductor movement. The system can also coordinate acceleration and deceleration so that the conductor, extruder, haul-off, and take-up remain synchronized.
Recipe management is particularly valuable for manufacturers producing multiple cable specifications. A saved recipe may include temperature settings, screw speed, haul-off speed, target diameter, printer data, cooling parameters, and winding settings. The operator can then load a validated recipe and make controlled adjustments rather than rebuilding the process from memory.
Cooling System
The cooling system removes heat from the extruded polymer and fixes the final dimensions. A pre-cooling water tank receives the cable shortly after it leaves the die. A longer main cooling tank then completes solidification before the cable reaches the measuring, printing, and take-up sections.
Cooling performance must be matched to polymer type, wall thickness, line speed, and cable diameter. Insufficient cooling can cause deformation, sticking, surface marks, or dimensional drift. Excessive or poorly distributed cooling can create internal stress or affect surface appearance. Water temperature, flow, tank length, cable immersion, and guide alignment all contribute to the final result.
Yessjet line layouts can be configured with suitable cooling lengths and guide arrangements for different products. For larger cables or high-output applications, a longer cooling path may be required. For smaller wires, compact configurations can reduce factory space requirements while maintaining adequate solidification.
Outer Diameter Measuring Instrument
Continuous diameter measurement gives the operator a direct view of production stability. A laser measuring instrument can monitor the cable after cooling and provide data to the control system. If the diameter deviates from the target, the line can adjust the extruder speed, haul-off speed, or another selected control variable.
Closed-loop diameter control reduces dependence on manual sampling. It is particularly useful during steady production, material changes, acceleration, and transition between product specifications. A well-configured feedback system can help maintain a narrow diameter range and reduce the quantity of cable that must be downgraded or scrapped.
Diameter measurement has limits. It measures the external dimension and does not automatically reveal internal eccentricity or the thinnest wall point. For applications with demanding insulation requirements, manufacturers may combine outer diameter measurement with ultrasonic wall thickness monitoring, capacitance-based eccentricity measurement, spark testing, and laboratory inspection.
Ink Printing Machine
Identification printing allows manufacturers to apply product codes, voltage ratings, meter marks, dates, brand information, and other required markings. Printing equipment must be synchronized with line speed to maintain consistent character spacing and legibility.
The printing position, ink compatibility, drying behavior, and surface condition of the cable all affect print quality. A stable cooling and haul-off process provides a better surface for printing. The control system can coordinate the printer with the line meter counter so that marking data remains consistent throughout the production run.
Haul-Off and Tension Control
The haul-off transports the cable through the cooling and winding sections. It also influences the draw-down ratio and therefore the finished insulation thickness. If haul-off speed increases while extruder output remains constant, the insulation may become thinner. If haul-off speed decreases, the insulation may become thicker.
Dual-wheel or caterpillar-style haul-off systems provide positive contact with the cable. Belt pressure, contact length, belt material, and cable stiffness must be selected carefully. Soft compounds require sufficient traction without excessive compression or surface marking. Rigid cables may tolerate higher contact pressure, while flexible materials often need wider pads and lower clamping force.
Tension control is equally important at the pay-off and take-up. Excessive tension can stretch the conductor, especially in fine stranded constructions. Conductor elongation can alter lay length and electrical resistance. Insufficient tension can produce loops, unstable winding, and poor package formation. A properly designed line maintains a stable tension window through acceleration, steady production, reel change, and shutdown.
Take-Up, Coiling, and Packaging Equipment
The take-up machine collects the finished cable in a controlled manner. Depending on the product, the line may use a dual-axis reel take-up, automatic coiler, vertical storage rack, or other winding arrangement. The selected system must correspond to the cable diameter, package size, winding length, production speed, and customer requirements.
Automatic coiling equipment is valuable for small-gauge building wire and other products manufactured at high line speeds. Manual coiling may become a bottleneck when operators cannot handle the output rate of the extrusion line. An automatic system can measure the required length, control the coil diameter, cut the cable, transfer the finished coil, and begin the next cycle.
End-of-line automation may also include tying, taping, labeling, weighing, conveying, palletizing, or robotic stacking. Planning these functions during the initial line design provides a more reliable path for future expansion. Spare input and output capacity, documented signals, and defined handshake logic allow additional automation to be added without redesigning the complete control architecture.
Material-Specific Extrusion Performance
Different polymers require different processing strategies. A screw, barrel, die, and temperature profile that perform well with flexible PVC may not be suitable for LSZH, nylon, polyethylene, or Teflon-based materials. The compound’s melting point, viscosity, thermal stability, shear sensitivity, moisture content, and cooling behavior must be considered during line configuration.
PVC
PVC is widely used for building wire, appliance wire, control cable, and general-purpose insulation. Flexible PVC often requires controlled shear and stable temperature management because excessive heat can accelerate degradation. A suitable screw design promotes uniform mixing while avoiding unnecessary residence time and localized overheating.
For flexible PVC, a relatively moderate temperature profile may be used as a starting point, followed by adjustments based on melt pressure, surface appearance, torque, and final dimensions. The actual settings depend on the compound supplier’s recommendations and the formulation of the specific material.
Polyethylene
Polyethylene materials, including LDPE and HDPE, are used where electrical insulation, moisture resistance, and processing efficiency are important. Polyethylene may benefit from a progressive temperature profile that allows gradual melting. Proper feed-zone conditions help prevent premature melting and ensure consistent material conveyance.
Cooling is important because polyethylene can retain heat after leaving the die. Adequate tank length and stable water conditions help prevent deformation and improve dimensional consistency. Screw design, die geometry, and haul-off speed must be coordinated to achieve the desired wall thickness.
LSZH Compounds
Low-smoke zero-halogen compounds are used in applications where reduced smoke and halogen-free performance are required. These materials can be sensitive to processing conditions and may require careful control of melt temperature, shear, moisture, and residence time.
A barrier screw or an appropriate mixing section may improve melting and dispersion without creating excessive shear heat. The line should be operated within the compound manufacturer’s processing window. Stable feeding, controlled barrel zones, reliable cooling, and accurate diameter monitoring are important for maintaining a consistent jacket or insulation layer.
Nylon and Engineering Materials
Nylon and other engineering polymers can require controlled drying before extrusion. Moisture in the material may cause bubbles, surface defects, or reduced electrical performance. Material preparation, hopper design, barrel temperature, die temperature, and cooling conditions should therefore be considered together.
Engineering materials may also require specialized screw and die surfaces because of higher processing temperatures or different melt characteristics. A line intended for multiple material families should be configured with appropriate changeover procedures, cleaning methods, and temperature capabilities.
Representative Extruder Models and Output Range
The following table summarizes representative machine data supplied for the extrusion series. Actual output depends on polymer density, formulation, screw design, temperature profile, conductor size, product geometry, and operating conditions. The values should therefore be used for preliminary selection rather than as a guarantee for every material.
| Model | Screw Diameter | L/D Ratio | Maximum RPM | PVC Output kg/h | LDPE Output kg/h | LSNH Output kg/h | Finished Diameter mm | Drive Motor kW |
|---|---|---|---|---|---|---|---|---|
| EX-40G | 40 mm | 26:1 | 120 | 24 | 14 | — | 0.8–3 | 11 |
| EX-40S | 40 mm | 26:1 | 120 | 48 | 14 | — | 0.8–3 | 15 |
| EX-50G | 50 mm | 26:1 | 120 | 60 | 35 | — | 1–6 | 15 |
| EX-50S | 50 mm | 26:1 | 120 | 75 | 35 | — | 1–6 | 18.5 |
| EX-60G | 60 mm | 26:1 | 120 | 100 | 60 | 22 | 2–8 | 22 |
| EX-60S | 60 mm | 26:1 | 120 | 120 | 60 | 24 | 2–8 | 30 |
| EX-70G | 70 mm | 26:1 | 120 | 140 | 95 | 36 | 3–15 | 30 |
| EX-70S | 70 mm | 26:1 | 120 | 160 | 95 | 40 | 3–15 | 37 |
| EX-80G | 80 mm | 26:1 | 110 | 200 | 130 | 48 | 5–20 | 37 |
| EX-80S | 80 mm | 26:1 | 110 | 250 | 130 | 52 | 5–20 | 45 |
| EX-90G | 90 mm | 26:1 | 110 | 280 | 180 | 65 | 8–25 | 45 |
| EX-90S | 90 mm | 26:1 | 110 | 320 | 180 | 70 | 8–25 | 55 |
| EX-100G | 100 mm | 25:1 | 100 | 380 | 240 | 90 | 10–30 | 55 |
| EX-100S | 100 mm | 25:1 | 100 | 450 | 240 | 100 | 10–30 | 75 |
| EX-120G | 120 mm | 25:1 | 100 | 500 | — | — | 15–40 | 90 |
| EX-120S | 120 mm | 25:1 | 100 | 600 | — | — | 15–40 | 110 |
The G and S designations represent different configurations within the series. The higher-capacity models are suitable for manufacturers seeking increased throughput, larger conductor sizes, or higher jacket output. Selection should be based on the complete production requirement rather than maximum kilograms per hour alone. A machine that is too large for the target product may operate inefficiently, while an undersized machine may limit future production growth.
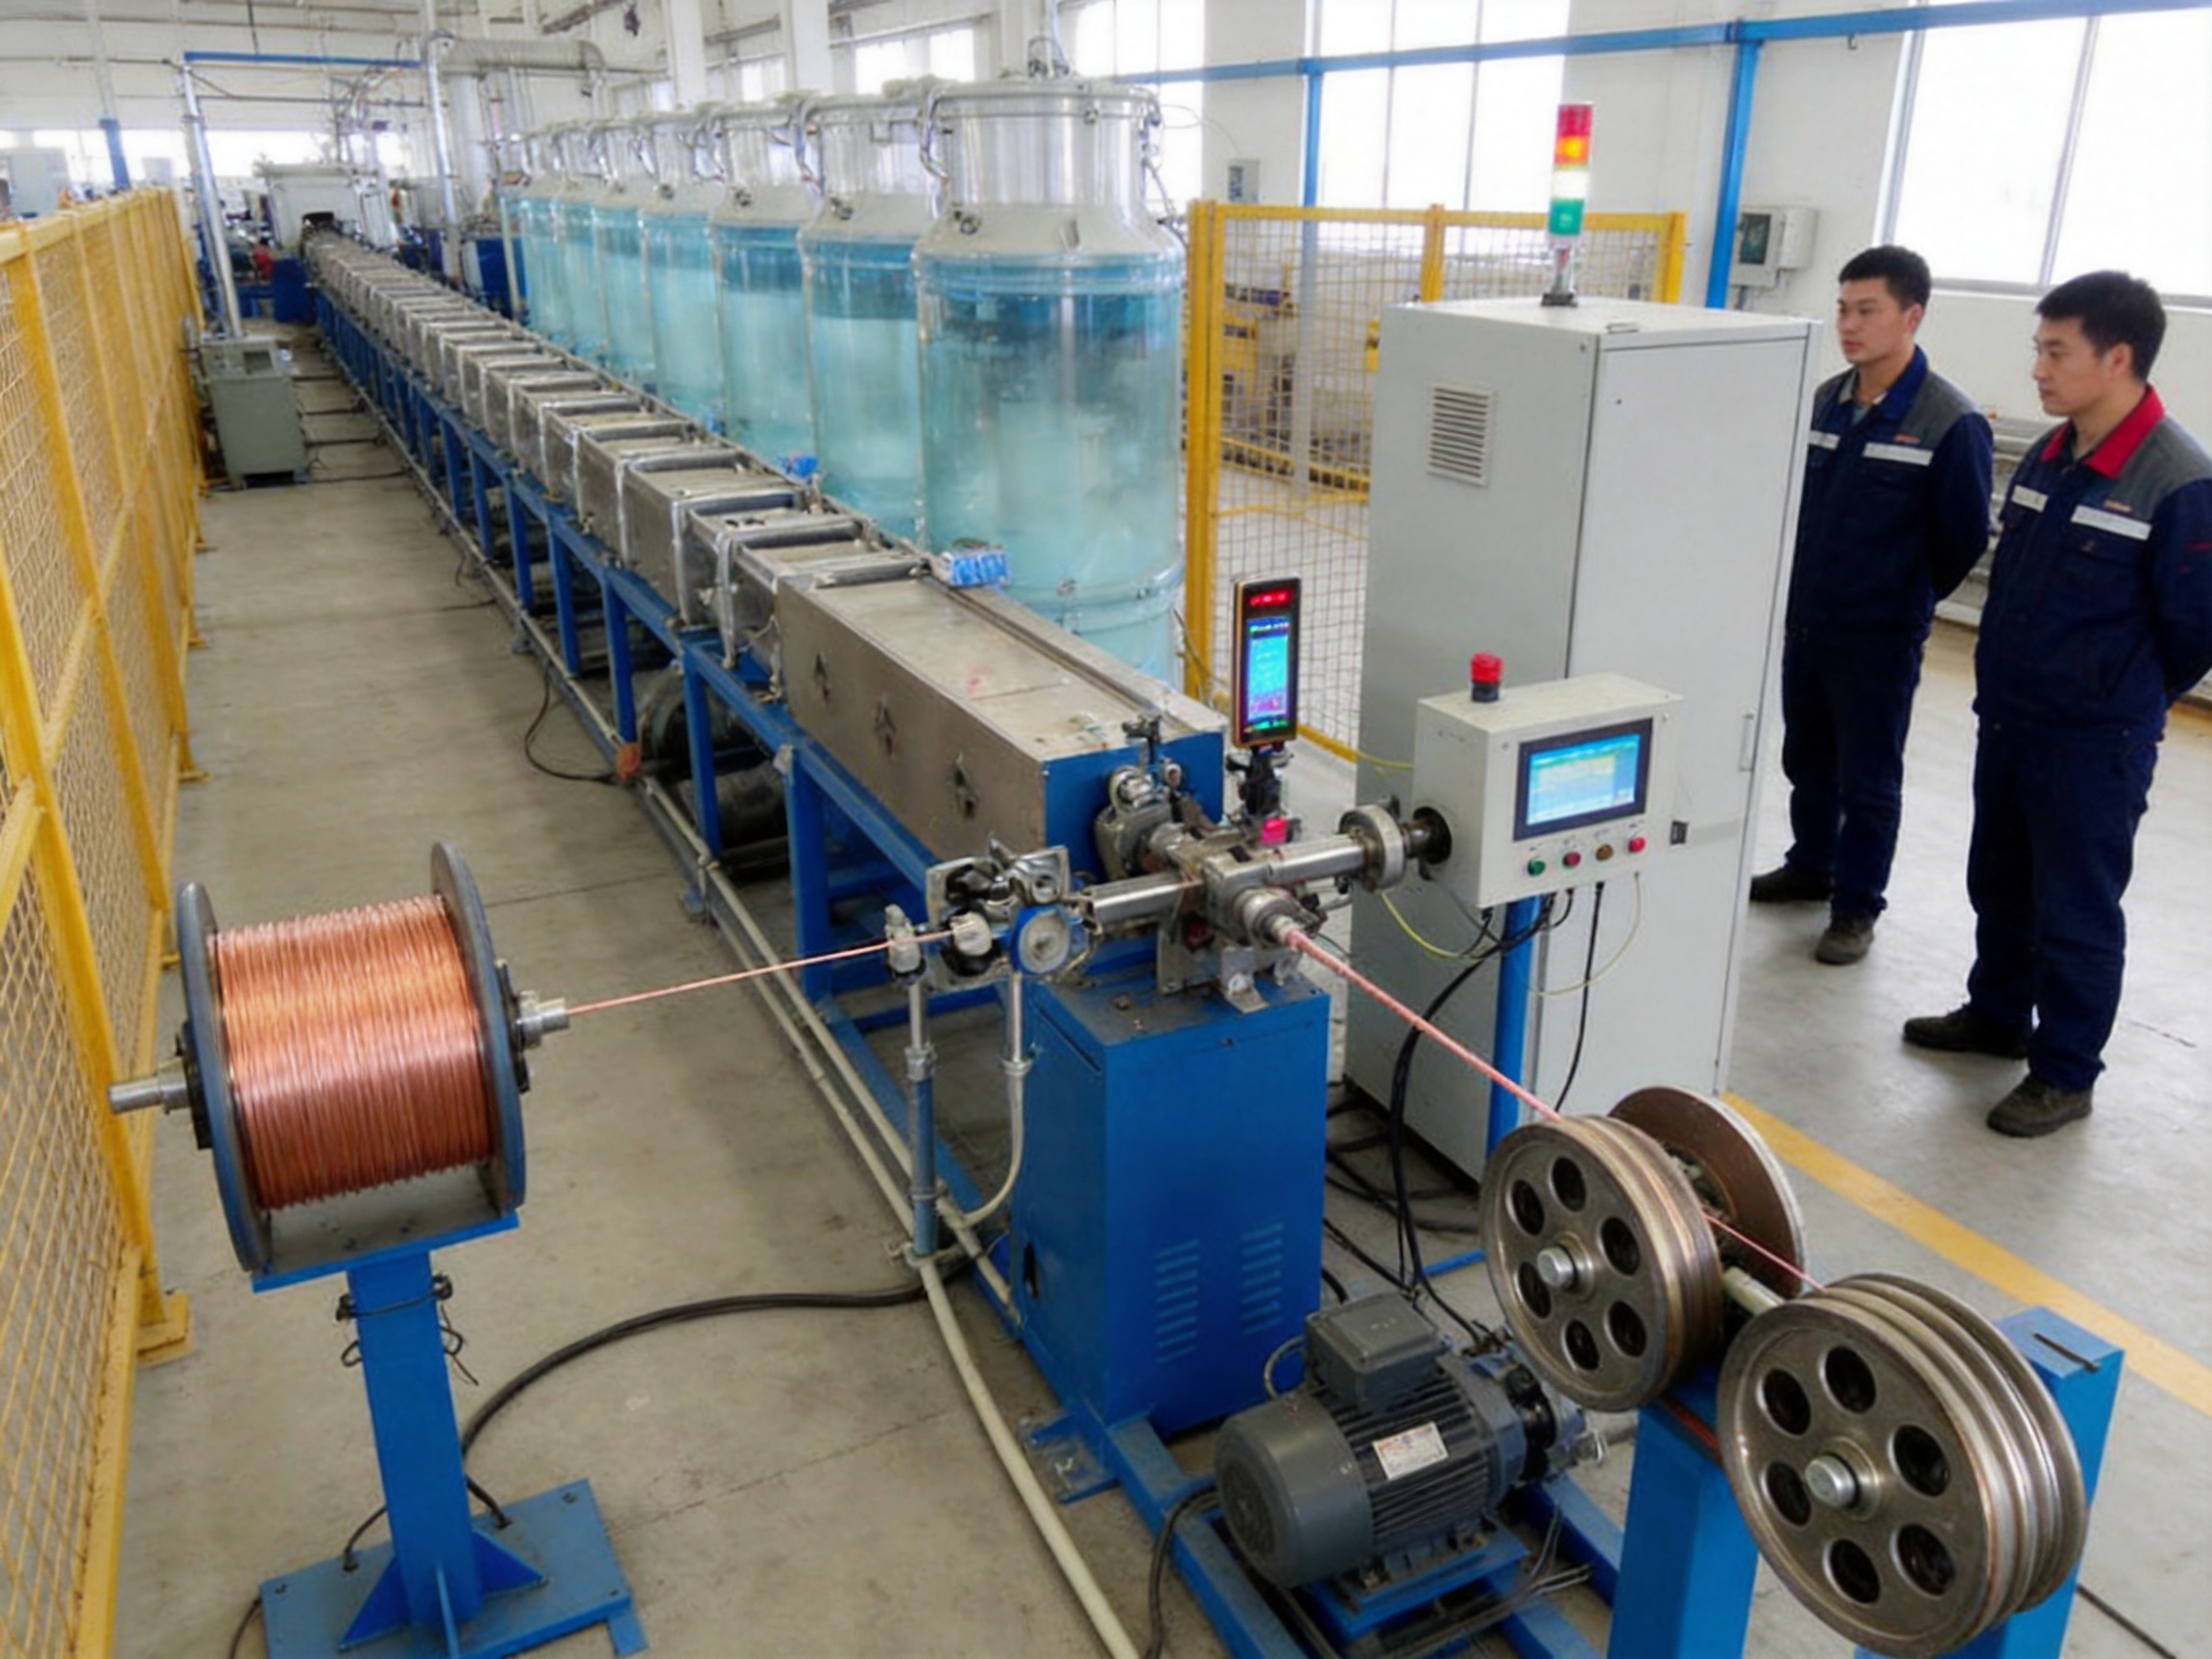
How Screw Design Influences Product Quality
The screw is one of the most important components in the extrusion machine. Its diameter, length-to-diameter ratio, compression ratio, flight geometry, mixing section, and barrier design determine how the material is conveyed and plasticized. These factors influence melt temperature, pressure stability, output, dispersion, and surface quality.
A longer L/D ratio gives the polymer more residence time for melting and mixing. Ratios around 25:1 to 30:1 are commonly used for many cable insulation applications. However, longer residence time can also increase shear heat and may not be ideal for heat-sensitive compounds. The correct balance depends on the material and the target output.
Barrier screw designs can separate solid and molten phases during processing. This may improve melting efficiency and reduce unmelted particles without relying entirely on high shear. A dedicated mixing section near the metering zone can improve melt uniformity when the compound requires additional dispersion.
Yessjet configures screw geometry according to the intended compound family and output range rather than applying one universal screw to every application. Considerations may include polymer viscosity, processing temperature, thermal sensitivity, conductor size, line speed, required wall thickness, and desired production capacity. This material-specific approach helps reduce defects that might otherwise be incorrectly attributed to die alignment or tension problems.
Temperature Control and Process Stability
Temperature control is not limited to reaching a single target temperature. The polymer experiences a thermal history as it moves through the feed, compression, metering, adapter, and die zones. Each zone must contribute to a stable melt condition without creating premature melting, excessive shear heat, degradation, or poor mixing.
Modern cable extrusion lines commonly use several independently controlled barrel zones in addition to adapter and die zones. The operator can establish a temperature gradient suited to the material. For polyethylene, a gradually rising profile may support controlled melting. For flexible PVC, a flatter profile may help limit thermal accumulation. LSZH materials may require a carefully managed profile that balances melting and low degradation risk.
Indicative starting profiles may be organized as follows:
| Material | Feed Zone | Compression Zone | Metering Zone | Die Zone |
|---|---|---|---|---|
| HDPE | 160–175°C | 190–200°C | 210–220°C | 215–225°C |
| Flexible PVC | 150–160°C | 165–175°C | 170–180°C | 175–185°C |
| XLPE | 100–115°C | 120–130°C | 125–135°C | 130–140°C |
| LSZH | 155–165°C | 170–180°C | 175–185°C | 180–190°C |
These values are reference ranges and not universal operating recipes. Compound suppliers may specify different conditions. Actual optimization should consider melt pressure, motor load, surface appearance, output stability, cooling behavior, and finished cable testing. Melt temperature measurement can also be useful because barrel setpoints do not always represent the actual temperature of the polymer at the die.
Diameter Control, Eccentricity, and Quality Assurance
Outer diameter is one of the most visible dimensions in cable production, but it is only one part of quality control. A cable may meet the outer diameter target while having uneven insulation distribution around the conductor. For this reason, line design should distinguish between diameter control and concentricity control.
Laser diameter gauges provide continuous measurement of the outside dimension. When connected to the line controller, the gauge can support automatic adjustment of extruder speed or haul-off speed. This is useful during steady production and can reduce gradual drift caused by material temperature, pressure, or speed changes.
Eccentricity can be influenced by conductor alignment, die centering, crosshead temperature, melt pressure, conductor vibration, and tension. A thermal shift in the crosshead may alter die alignment during a long production run. Ultrasonic or capacitance-based systems can provide additional information about insulation thickness and eccentricity where the application requires it.
Control-loop response time must also be considered. The distance between the die and measuring instrument creates a transport delay. At higher line speeds, a disturbance may travel a significant distance before the gauge detects it. A control system that reacts too aggressively may create oscillation instead of correcting the original problem. Proper deadband, filter, and response settings are therefore important for stable operation.
Quality assurance should combine online and offline methods. Typical checks may include outer diameter, insulation thickness, eccentricity, spark testing, conductor resistance, tensile performance, elongation, surface appearance, print legibility, package length, and winding quality. The exact test program depends on the cable type, applicable standard, and customer specification.
Advanced Manufacturing Strengths
The value of a cable extrusion line depends not only on its component list but also on how the equipment is engineered, manufactured, assembled, tested, and commissioned. Shanghai Yessjet Precise Machinery Co., Ltd. focuses on integrated wire and cable machinery and can support customers from initial process definition through line configuration and production startup.
Application-Based Engineering
Before selecting the extruder model, the engineering process should consider conductor material, conductor construction, insulation compound, target finished diameter, wall thickness, production speed, package type, factory space, utilities, and future expansion. This prevents the common mistake of selecting an extruder solely according to nominal motor power or maximum theoretical output.
Application-based engineering also enables better selection of die sets, cooling lengths, haul-off systems, tension devices, and take-up equipment. The result is a line that is more closely aligned with the customer’s actual production plan.
Component Matching
Every production section affects the next. The pay-off must be compatible with the conductor reel. The extruder must produce the required melt output. The crosshead must accept the die design. The haul-off must provide sufficient traction without damaging the surface. The take-up must handle the speed and package dimensions.
Yessjet’s integrated design approach seeks to match these components rather than treating them as independent purchases. This can reduce commissioning problems and simplify operator training. It also enables the control system to use consistent speed references and coordinated signals.
Control-System Capability
Programmable logic control, digital temperature regulation, drive coordination, alarm management, recipe storage, and measurement feedback are important features of a modern line. A well-designed system gives operators direct access to relevant information without overwhelming them with unnecessary settings.
The control architecture can also be planned with future automation in mind. Spare input and output capacity, defined communication signals, and documented interfaces make it easier to add automatic coilers, packaging stations, conveyors, or robotic palletizing later.
Mechanical and Electrical Commissioning
Commissioning is the stage at which engineering decisions are validated under operating conditions. Mechanical alignment, die centering, barrel heating, drive response, temperature calibration, water circulation, printer synchronization, diameter measurement, and take-up tension should all be checked systematically.
A structured commissioning process reduces the risk of transferring unresolved problems to the customer’s factory. It also helps establish baseline recipes and maintenance procedures. Operators can then learn how to recognize normal operating conditions and respond to deviations.
Retrofit Evaluation
Older extrusion lines may still have useful mechanical components, but obsolete control systems can limit productivity and data collection. Targeted retrofits may include PLC replacement, touchscreen HMI installation, digital temperature controllers, laser diameter measurement, servo haul-off drives, and improved tension feedback.
However, retrofit decisions should begin with a mechanical assessment. Barrel and screw wear, gearbox condition, frame alignment, crosshead condition, heater performance, and cooling-system integrity must be evaluated before investing in new controls. Upgrading electronics on severely worn mechanical equipment may not provide a reliable long-term solution.
A structured evaluation can include screw and barrel wear measurement, gearbox backlash checks, thermal imaging of heating zones, inspection of electrical components, and review of spare-parts availability. This approach helps customers determine whether to modernize the existing line or replace it with a new system.
Advantages Compared with Basic or Incompatible Competitor Systems
Wire and cable extrusion equipment is available from many suppliers, but product quality and operating results can vary considerably. The main distinction is often not the appearance of the machine but the depth of application engineering behind it.
- Material-specific configuration: Instead of using one generic screw for every polymer, the line can be configured according to the processing behavior of PVC, polyethylene, LSZH, nylon, Teflon-based materials, or other compounds.
- Integrated control: Pay-off, extruder, haul-off, measurement, printer, and take-up functions can be coordinated through a common control architecture.
- Stable temperature management: Multiple heating zones and digital control improve the ability to maintain a consistent melt condition.
- Flexible capacity selection: The model range covers small, medium, and high-output requirements, allowing customers to select equipment according to current needs and future growth.
- End-of-line readiness: The control design can provide a practical path for adding coiling, packaging, and robotic stacking equipment.
- Process-focused commissioning: Startup work addresses not only machine operation but also diameter stability, tension, cooling, printing, winding, and product testing.
- Retrofit capability: Existing lines can be assessed for control modernization where the mechanical platform remains suitable.
- Turnkey support: Customers can source extrusion, pay-off, take-up, coiling, and accessory equipment from one specialized supplier.
These advantages can reduce hidden costs associated with unstable production, excessive scrap, difficult changeovers, incompatible spare parts, and repeated troubleshooting between different vendors. The best supplier is not necessarily the one offering the lowest equipment price; it is the one able to deliver a stable and maintainable production process.
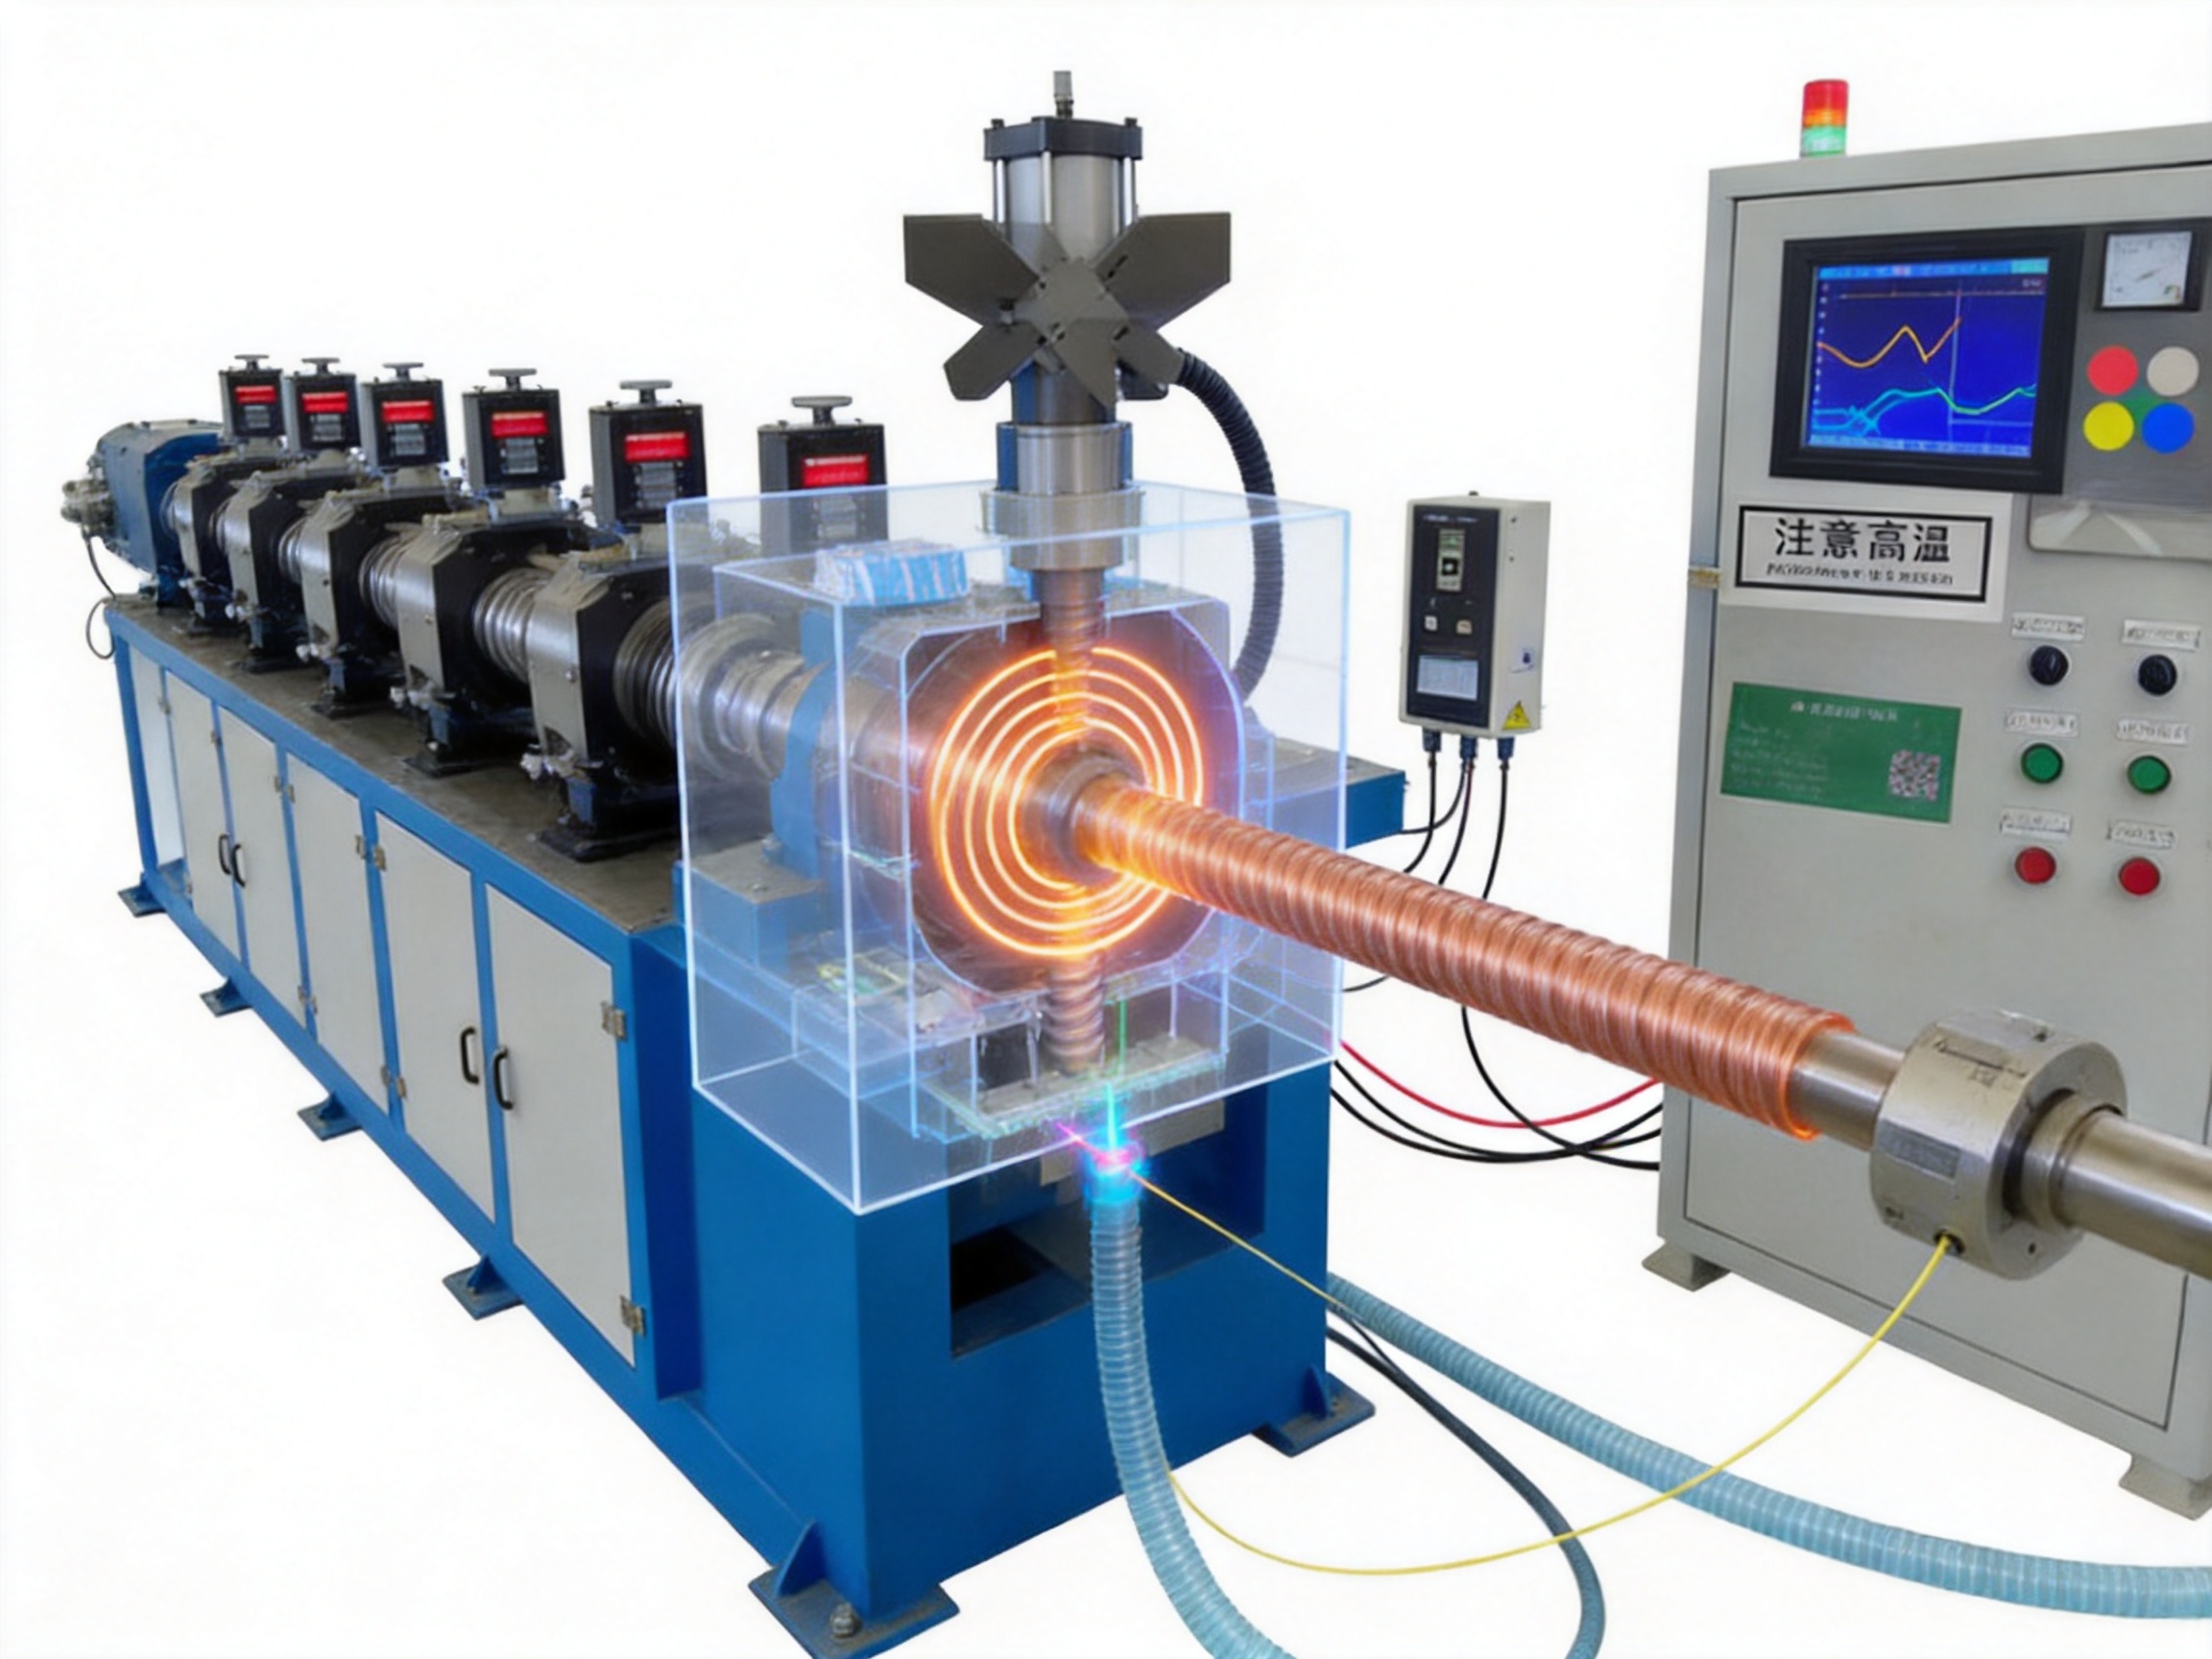
Automatic Coiling and Robotic Stacking Integration
End-of-line handling has become increasingly important as extrusion speeds rise. When a line produces cable faster than operators can coil, package, label, and stack it, the packaging section becomes the actual production limit. Automatic coiling and robotic stacking can remove this bottleneck.
An automatic coiling system requires reliable information from the extrusion line. The meter counter must accurately measure production length. The control system must issue a cut or transfer signal at the correct position. The cable must be guided without creating excess slack. The new coil core must be ready before the previous coil is removed. These functions require coordinated sequencing rather than a simple mechanical attachment.
Robotic stacking adds further requirements, including package detection, weight or size information, pallet position, safety guarding, and communication between the coiler, conveyor, and robot controller. When planned from the beginning, these interfaces can be included in the machine design. When added to an older line, the control system may require additional hardware and software integration.
A forward-compatible architecture may include spare I/O, reserved communication channels, terminal blocks, signal maps, and defined operating states. These provisions allow customers to add automation later without replacing the primary extrusion control system. This reduces future integration cost and protects the original investment.
Operating and Maintenance Recommendations
Stable production depends on regular maintenance as much as on initial machine quality. Operators should inspect the pay-off guides, conductor path, screw and barrel condition, heaters, thermocouples, water circulation, cooling guides, haul-off belts, printer heads, sensors, and take-up components according to a defined schedule.
Material handling is also essential. Polymer should be stored in suitable conditions and dried when required. Contamination, moisture, incorrect mixing, or excessive recycled content can create defects that no control system can fully correct. Materials should be identified clearly and loaded according to the approved production recipe.
Before starting a production run, the operator should verify:
- Correct conductor and reel installation.
- Correct die and tooling selection.
- Material identity and drying status.
- Temperature setpoints and warm-up completion.
- Water level, flow, and cooling temperature.
- Printer ink and marking information.
- Diameter gauge calibration and target settings.
- Haul-off belt condition and pressure.
- Take-up reel, coil former, or package configuration.
- Emergency stop and safety interlock condition.
During production, operators should monitor melt pressure, motor load, temperature deviations, line speed, measured diameter, tension, cooling water condition, and package formation. Trend information is often more valuable than a single measurement because gradual changes may indicate developing wear, material variation, or thermal drift.
Preventive maintenance should address wear before it causes product defects. Screw and barrel clearance, gearbox lubrication, die surfaces, belt wear, sensor calibration, electrical cabinet cleanliness, and cooling-system deposits should be included in the maintenance plan. Accurate records make it easier to identify recurring problems and plan spare-parts purchases.
How to Select the Correct Line Configuration
The correct extrusion line should be selected by answering several practical questions. What conductor types will be processed? What insulation and jacket materials will be used? What is the smallest and largest finished diameter? What output is required per hour? What line speed is expected? Will the final product be reeled, coiled, boxed, or palletized? What standards and tests must the cable meet?
The customer should also define future requirements. A line designed only for today’s product may become restrictive if the manufacturer later adds larger cables, LSZH compounds, automatic coiling, or robotic packaging. Selecting a suitable platform with expansion capacity may provide a lower total cost over the equipment’s service life.
Utility requirements must also be considered. These may include electrical supply, compressed air, cooling water, ventilation, material drying, floor loading, drainage, and factory space. A complete layout review helps prevent installation delays and ensures sufficient access for operation and maintenance.
Yessjet can support configuration decisions by matching the extruder model, screw design, pay-off, cooling length, diameter measurement, haul-off, take-up, and packaging equipment to the customer’s production objective. This application-based approach is more reliable than selecting equipment from a general-purpose catalog without reviewing the complete process.
Applications of Wire and Cable Extrusion Lines
Wire and cable extrusion lines can be used for a broad range of products, including building wire, appliance wire, control cable, automotive wire, communication cable, low-voltage power cable, industrial cable, flexible cable, and specialty insulated conductors.
Small-diameter wires often require high line speed, precise diameter measurement, efficient cooling, and automatic coiling. Medium-size cables may require stronger haul-off traction, longer cooling tanks, and reel take-up. Larger cables may require high-output extruders, reinforced pay-off systems, substantial cooling capacity, and heavy-duty take-up equipment.
Different markets may require different printing, testing, packaging, and documentation practices. An integrated line can be configured to accommodate these requirements while maintaining a common operating philosophy across product families.
Frequently Asked Questions
What materials can be processed on the line?
The equipment can be configured for materials such as PVC, LDPE, HDPE, LSZH compounds, nylon, Teflon-based materials, and other suitable thermoplastics. The correct screw, barrel, die, temperature profile, and cooling arrangement depend on the selected compound.
How is the extruder model selected?
Selection is based on required output, conductor size, finished diameter, material type, production speed, and future capacity requirements. The maximum output shown in a specification table is a reference value and should be confirmed through material-specific process evaluation.
Can the line produce both insulation and cable jackets?
With suitable tooling and process configuration, extrusion platforms can be adapted for insulation and jacketing applications. The die, crosshead, screw design, cooling length, and take-up system must be selected for the specific product structure.
Why is tension control important?
Stable tension keeps the conductor centered and prevents excessive elongation. High tension may stretch fine stranded conductors and alter electrical resistance, while low tension may cause loops, vibration, or poor winding. Coordinated pay-off, haul-off, and take-up control is therefore essential.
Can outer diameter control guarantee uniform insulation thickness?
No. Outer diameter measurement confirms the external dimension but does not directly measure wall thickness at every point around the conductor. For demanding applications, diameter control should be combined with die centering, conductor alignment, spark testing, and, where necessary, ultrasonic or capacitance-based eccentricity measurement.
What is the purpose of multiple barrel heating zones?
Multiple zones allow the operator to control the thermal gradient through the extrusion process. This supports gradual melting, stable mixing, controlled melt viscosity, and reduced risk of overheating or premature melting.
Can automatic coiling be added later?
It can be added when the existing line has sufficient mechanical space and a suitable control architecture. Spare I/O, communication interfaces, meter-counting signals, cut commands, and transfer logic make future integration easier. These requirements should be discussed during the original line design whenever possible.
Does the company provide complete production-line solutions?
The product range includes wire and cable extrusion lines, cable extrusion machines, motorized pay-off equipment, motorized take-up equipment, coiling machines, accessory equipment, fully automatic coiling and packaging equipment, and intelligent robot stackers. This enables customers to develop a coordinated production solution from one specialized machinery supplier.
Can older cable extrusion equipment be upgraded?
Many older lines can be upgraded if the extruder barrel, screw, gearbox, frame, crosshead, and cooling system remain mechanically suitable. Possible upgrades include PLC replacement, digital temperature control, touchscreen operation, laser diameter measurement, servo haul-off, and tension feedback. A mechanical inspection should be completed before selecting a retrofit package.
What information should be included in an equipment inquiry?
A useful inquiry should include conductor material and construction, conductor diameter, insulation or jacket material, target finished diameter, wall thickness, output requirement, line speed, reel size, package type, required printing, applicable standards, factory voltage, and desired automation level. Providing this information helps the engineering team recommend a suitable configuration.
Conclusion
A wire and cable extrusion line is a complete production system in which material processing, conductor handling, measurement, cooling, printing, tension, and winding must work together. The extruder is important, but the final product depends equally on the pay-off, crosshead, cooling tanks, diameter control, haul-off, take-up, and automation interfaces.
The main advantages of an integrated Yessjet solution are material-specific engineering, coordinated control, flexible machine capacity, stable temperature management, compatible line components, future-ready automation, and support for both new installations and selected retrofits. These strengths help manufacturers improve production consistency, reduce waste, increase operating efficiency, and prepare for automatic coiling, packaging, and robotic stacking.
By combining extrusion technology with practical process knowledge, Shanghai Yessjet Precise Machinery Co., Ltd. provides equipment for manufacturers seeking dependable wire and cable production capability. Whether the requirement is a compact line for small-gauge insulated wire, a high-output system for larger cable, an automatic coiling solution, or a complete turnkey production arrangement, the correct configuration should be developed around the product and the customer’s long-term manufacturing objectives.
References
1. General principles of polymer extrusion processing and screw design for thermoplastic materials.
2. Industrial practices for wire and cable insulation, jacketing, cooling, tension control, and take-up operation.
3. Technical guidance for continuous laser diameter measurement and closed-loop extrusion control.
4. Manufacturer process data for PVC, polyethylene, LSZH, nylon, and engineering polymer extrusion.
5. International cable manufacturing practices concerning conductor resistance, insulation thickness, eccentricity, spark testing, and dimensional inspection.
6. Equipment specification data for EX-series wire and cable extrusion machines, motorized pay-off systems, take-up systems, coiling equipment, and related automation.
7. Industrial automation principles for PLC control, recipe management, drive synchronization, automatic packaging, and robotic palletizing.