LANGUAGE
 中文简体
 русский
 Français
 Español
 Português
 عربى
Content
- 1 The Role of Automated Coiling in LAN Cable Production
- 2 Product Overview
- 3 Technical Specifications
- 4 How the Cross-Winding Process Works
- 5 Advantages Compared with Manual Coiling
- 6 Benefits for LAN Cable Manufacturers
- 7 Touch-Screen Operation and Production Flexibility
- 8 Manufacturing Strengths and Engineering Approach
- 9 Installation and Production Planning
- 10 Maintenance and Long-Term Performance
- 11 Safety Considerations
- 12 Choosing Between DCW-2540 and DCW-2540P
- 13 Applications Beyond Standard LAN Cable
- 14 Return on Investment Considerations
- 15 Why Supplier Support Matters
- 16 Frequently Asked Questions
- 16.1 What types of LAN cable can the machine process?
- 16.2 Can the machine produce a coil without a center hole?
- 16.3 Can the center-hole size be changed?
- 16.4 What is the maximum listed speed?
- 16.5 What cable diameter can the DCW-2540 process?
- 16.6 What cable diameter can the DCW-2540P process?
- 16.7 What are the listed coil dimensions?
- 16.8 Why is the net-type coil useful?
- 16.9 Is the machine suitable for a packaging line?
- 16.10 Does the machine eliminate the need for operators?
- 16.11 How should the correct model be selected?
- 16.12 Can one machine process different cable products?
- 16.13 What should be checked during a production trial?
- 16.14 What maintenance is normally required?
- 17 Conclusion
- 18 References
- 19 Product: Cross Winder For LAN Cable
Modern data communication networks depend on cables that must be manufactured, handled, stored, and packaged with a high degree of consistency. LAN cables such as Cat5, Cat5e, and Cat6 are produced in large volumes, and their packaging quality directly affects warehouse efficiency, transport safety, installation convenience, and the perceived quality of the finished product. A cable that is loosely wound, tangled, unevenly arranged, or poorly matched to its packaging box can create unnecessary labor, material waste, and customer complaints.
The Cross Winder for LAN Cable is designed to address these challenges through automatic cable coiling, adjustable winding control, and a net-type coil configuration. It is suitable for mainstream LAN cable products and can also process coaxial cable within the applicable diameter range. By replacing many manual winding operations with a controlled mechanical process, the machine helps manufacturers improve productivity while maintaining a more uniform appearance from coil to coil.
Available in DCW-2540 and DCW-2540P configurations, the equipment can handle cable diameters from 0.8 to 6 mm or from 1 to 12 mm, depending on the selected model. It can create coils with or without a center hole, while the hole size can be adjusted through a touch-screen interface. This flexibility allows the coiling process to be matched with different box sizes, cable specifications, and packaging requirements.
The Role of Automated Coiling in LAN Cable Production
LAN cable production does not end when the cable leaves the extrusion or testing section. The cable must still be collected in a form that preserves its physical condition and makes it ready for shipment or retail packaging. In many factories, coiling is one of the final operations before packing. Any inconsistency at this stage can slow down the entire production line.
Manual coiling is often difficult to standardize. Operators may apply different levels of tension, produce different coil diameters, or create uneven layers. When a cable is wound too tightly, its structure may experience unnecessary mechanical stress. When it is wound too loosely, the coil can shift, expand, or become tangled. Manual processes also require continuous labor and are affected by fatigue, training differences, and production fluctuations.
An automatic cross winder establishes a repeatable winding pattern. The cable is guided into a net-type coil, helping individual turns remain organized instead of forming an irregular bundle. The resulting coil is easier to handle, place into a box, label, and transport. The machine also enables operators to select a hole or hole-free winding format according to the packaging design.
For manufacturers producing large quantities of LAN cable, this repeatability is particularly valuable. A stable winding process supports predictable packing dimensions, simplifies material planning, and helps reduce the amount of time required for downstream handling. The machine therefore functions not only as a coiler but also as an important part of a broader cable production and packaging system.
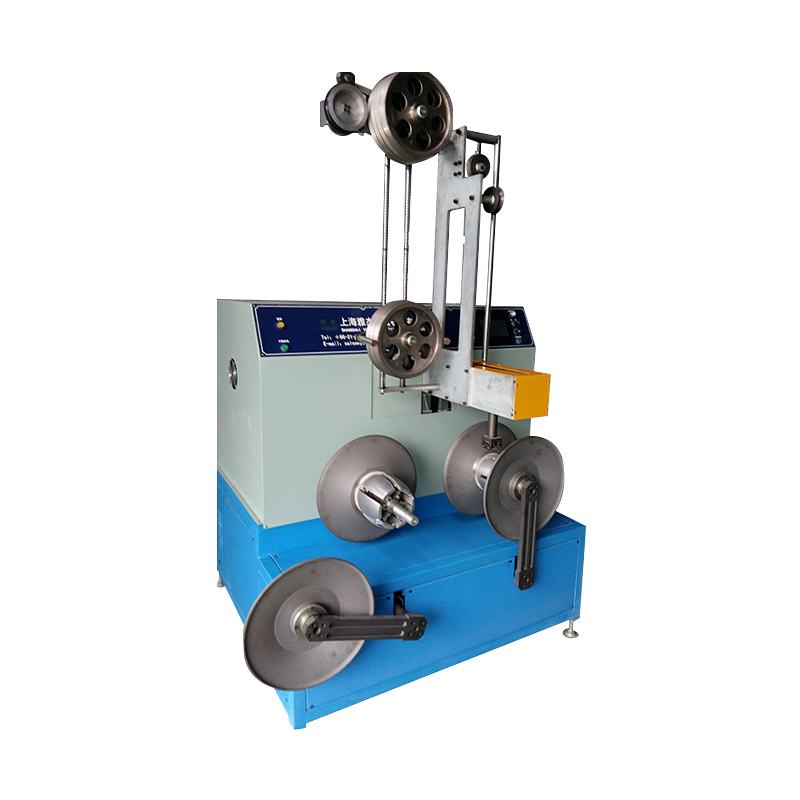
Cross Winder For LAN Cable
Product Overview
The Cross Winder for LAN Cable is an automatic coiling machine developed for efficient handling of communication and related cables. Its main application is the winding of Cat5, Cat5e, and Cat6 LAN cables. It is also applicable to coaxial cables, giving cable producers greater flexibility when one machine must support more than one product category.
The equipment forms the cable into a net-type coil. This winding style provides a neat and orderly arrangement while helping prevent cable turns from becoming entangled. The design is suitable for cable packaging operations in which the finished coil must be placed into a box, carton, or other container with a defined internal dimension.
One of the machine’s most useful functions is the choice between winding a coil with a hole and winding a coil without a hole. A central opening may be required for certain box designs, dispensing systems, or product presentation formats. Other applications may require a solid coil. Instead of changing the entire mechanical arrangement for each packaging format, the operator can select the required winding mode and adjust the hole dimension through the touch screen.
The product is available in two primary versions. The DCW-2540 is intended for cable diameters from 0.8 to 6 mm and does not require a pneumatic system according to the supplied specification. The DCW-2540P supports cable diameters from 1 to 12 mm and includes pneumatic operation. Both models provide a stated maximum speed of 250 RPM, with a listed outside coil diameter of 400 mm, inside diameter of 180 mm, and coil height of 250 mm.
Key Product Functions
Automatic LAN cable coiling: The machine automatically winds the cable, reducing dependence on manual labor and supporting stable production output.
Net-type winding: The cross-winding method forms a neat coil that is more resistant to tangling and easier to package.
Multi-cable application: The equipment is designed for Cat5, Cat5e, and Cat6 LAN cables and can also be used for coaxial cable within the applicable working range.
Selectable center-hole format: Operators can choose to produce a coil with a hole or without a hole.
Adjustable hole size: The central hole dimension can be adjusted through the touch-screen control system to correspond with packaging box requirements.
Two model configurations: The standard DCW-2540 and pneumatic DCW-2540P provide different cable diameter capabilities for different production needs.
Packaging-oriented design: The winding dimensions are suitable for applications in which cables are prepared for boxed or organized shipment.
Technical Specifications
| Model | Coil Height | Outside Diameter | Inside Diameter | Applicable Cable Diameter | Maximum Listed Speed | Pneumatic System |
|---|---|---|---|---|---|---|
| DCW-2540 | 250 mm | 400 mm | 180 mm | 0.8–6 mm | 250 RPM | No |
| DCW-2540P | 250 mm | 400 mm | 180 mm | 1–12 mm | 250 RPM | Yes |
The specifications show that both versions share the same listed coil height, outside diameter, inside diameter, and maximum rotational speed. The main selection difference is the applicable cable diameter range and the inclusion of pneumatic operation in the DCW-2540P. Selecting the correct model should be based on the cable products to be processed, the desired automation configuration, and the operating conditions of the production line.
The stated dimensions provide a practical reference for packaging planning. A maximum outside diameter of 400 mm and a coil height of 250 mm allow the packaging department to prepare suitable cartons or boxes. The adjustable hole function provides additional flexibility where internal packaging supports, dispensing cores, or presentation requirements vary.
Actual production results may depend on cable construction, material, surface friction, incoming tension, winding length, operator settings, and the specific packaging method. For this reason, manufacturers should confirm the final operating parameters through sample testing before placing the machine into full-scale production.
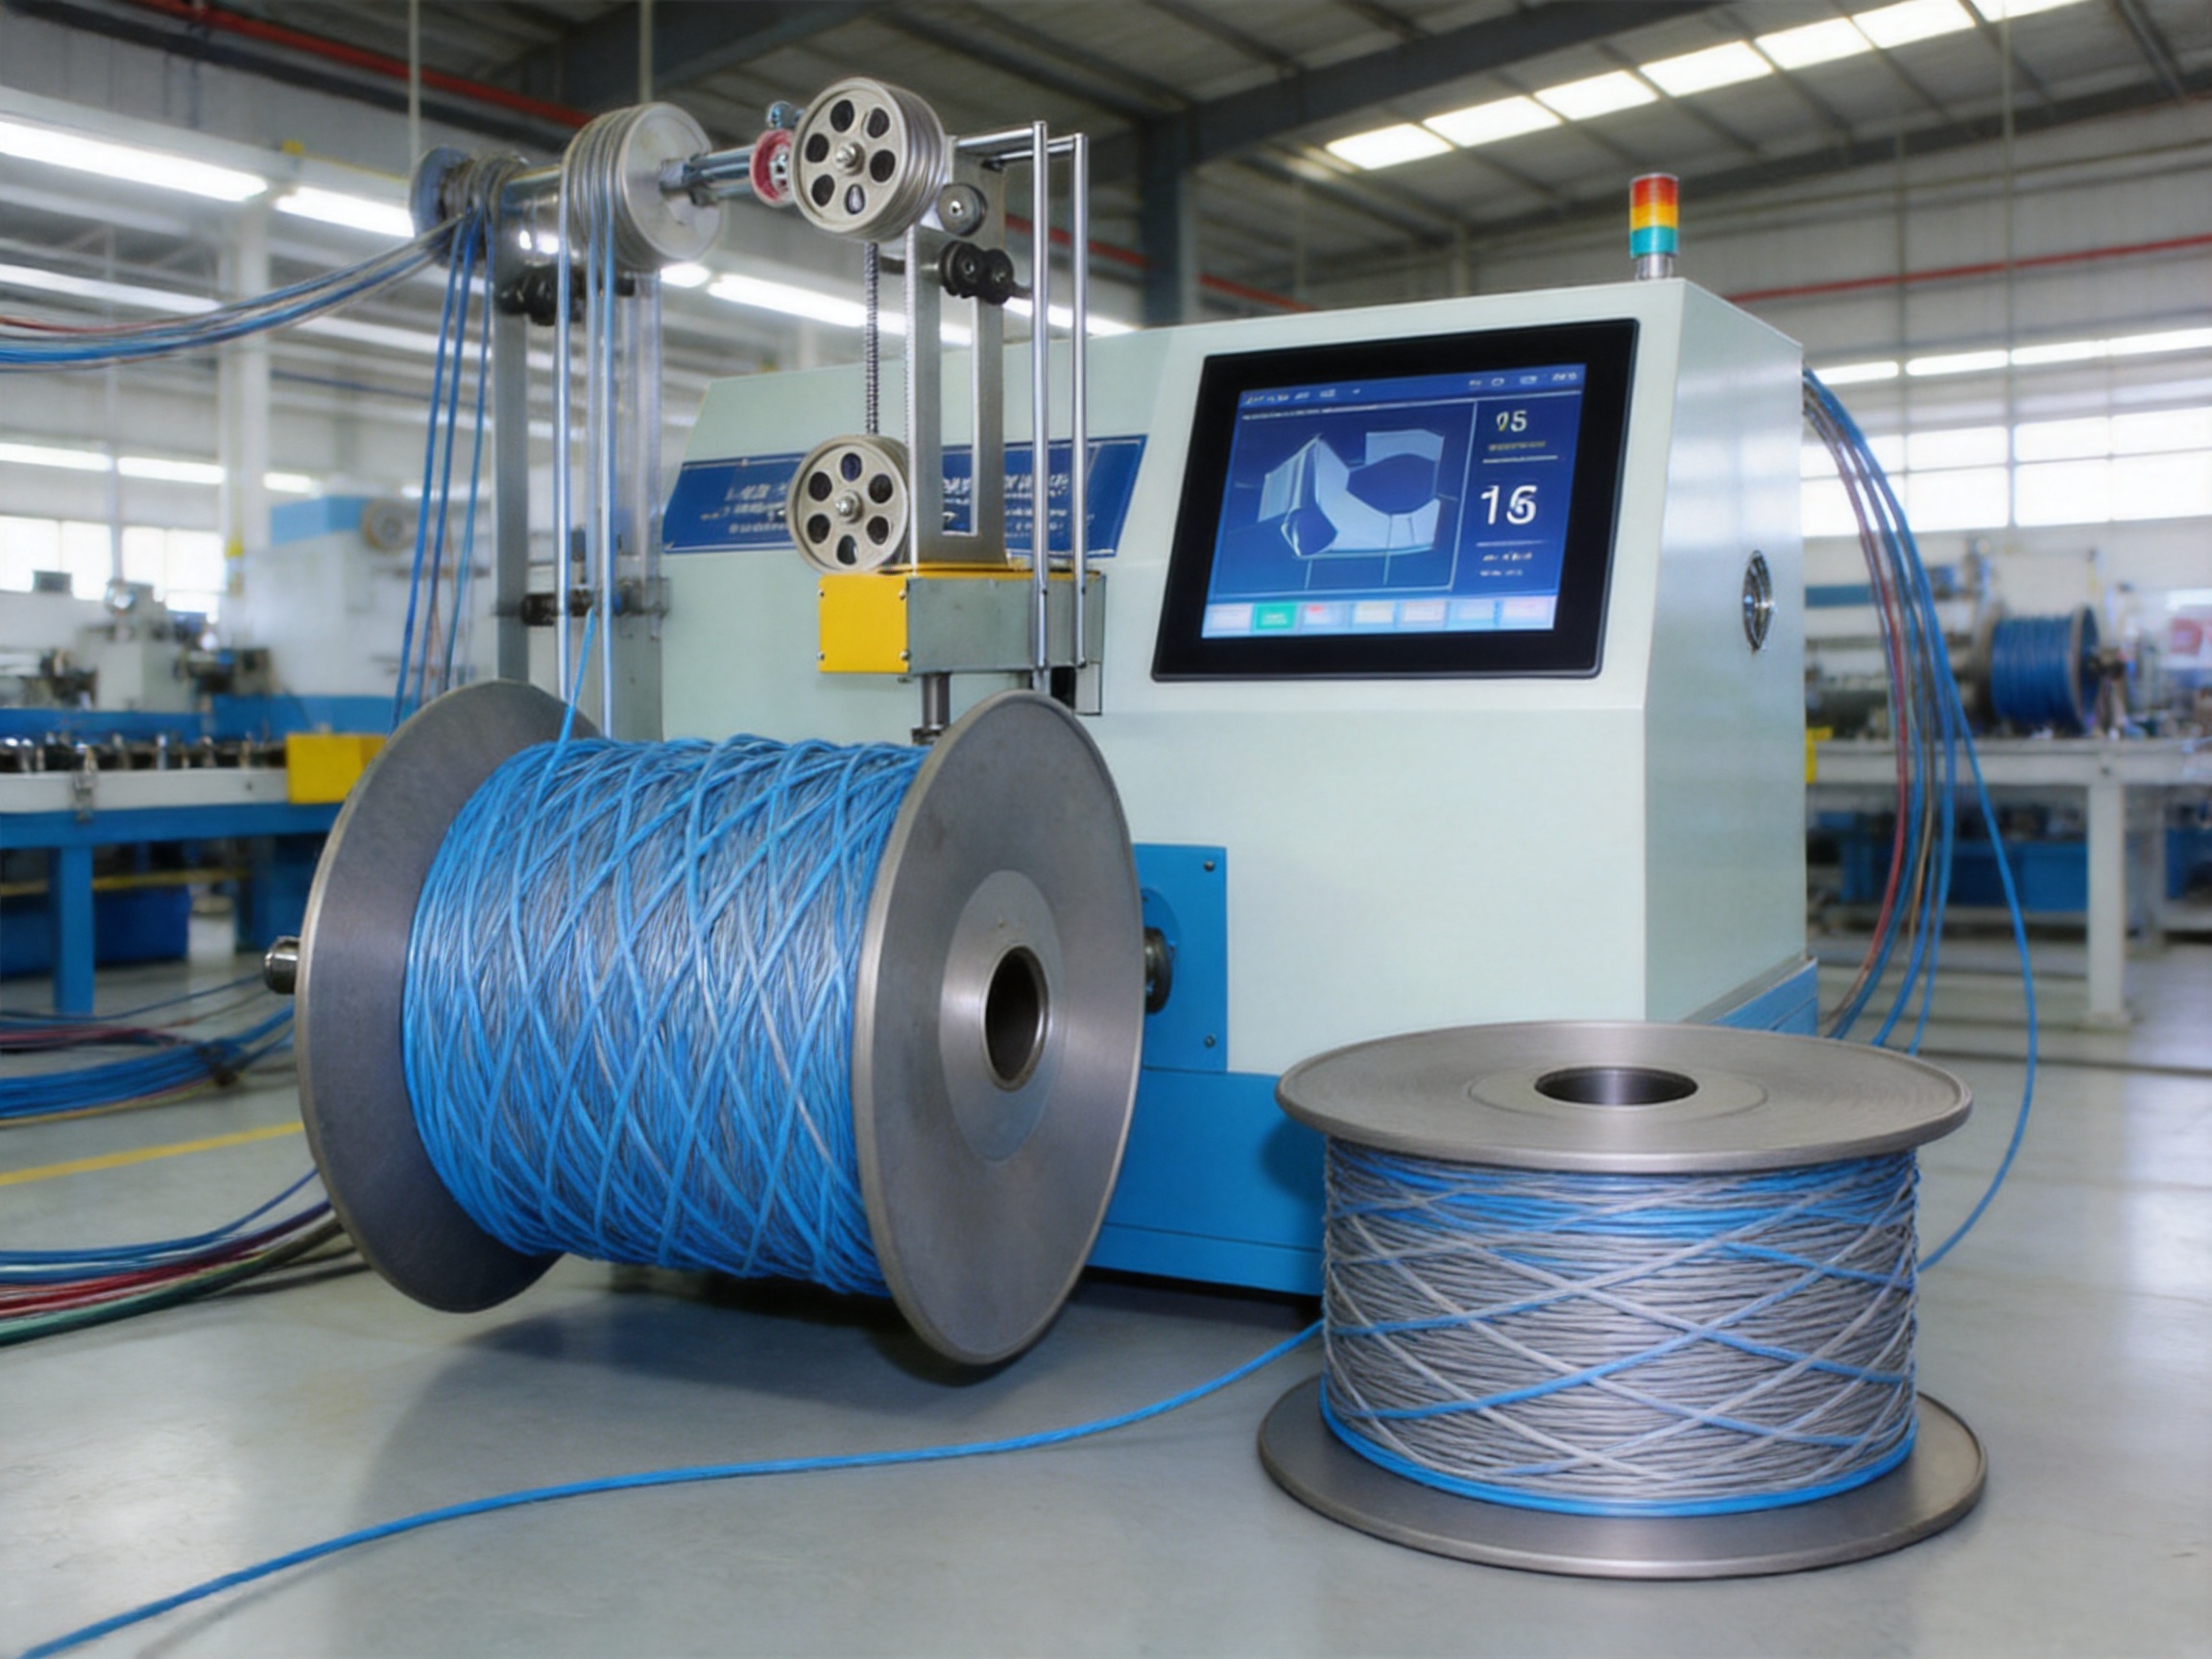
How the Cross-Winding Process Works
The operating principle is based on controlled cable guidance and organized winding. Cable supplied from an upstream pay-off or cable handling section enters the coiling unit. The machine directs the cable into the winding area, where coordinated movement creates the cross pattern that forms the net-type coil.
During winding, the cable is distributed across the coil width rather than being placed randomly in a single narrow track. This produces a more stable arrangement and helps the turns support one another. The result is a compact coil with a more regular external appearance and improved resistance to tangling.
When a center hole is required, the operator selects the appropriate mode and sets the target hole size on the touch screen. The machine then forms the coil around the selected opening. When a hole-free coil is needed, the corresponding setting can be chosen for the product being packaged.
The winding process should be coordinated with the upstream cable supply. A suitable pay-off arrangement helps maintain smooth feeding and prevents sudden tension changes. If the cable arrives with excessive twist, sharp bends, or irregular tension, the quality of the finished coil may be affected. A complete cable handling system therefore typically includes an appropriate pay-off, guiding components, and careful adjustment of the line speed.
At the end of the cycle, the completed coil can be transferred to the packing operation. Depending on the factory layout, this may involve manual removal, a conveyor, or integration with additional packaging equipment. The cross winder can consequently serve as a standalone machine or as part of a larger wire and cable packaging line.
Importance of Cable Tension
Cable tension is a critical factor in any automatic coiling operation. Too little tension may produce a loose or unstable coil. Too much tension may deform the cable, affect its geometry, or make the finished coil difficult to remove and package. A well-configured line aims to maintain consistent tension from the pay-off through the winder.
LAN cables contain insulated conductors, separators, shielding or drainage elements in some designs, and an outer jacket. Their electrical performance can be influenced by physical deformation. Controlled winding helps the manufacturer handle the cable carefully and reduces the risk of unnecessary bending or compression during packaging.
The correct tension setting will depend on cable diameter, jacket material, construction, and production speed. Operators should establish settings through trial production and monitor both the coil appearance and the cable’s quality test results.
Advantages Compared with Manual Coiling
The strongest advantage of the Cross Winder for LAN Cable is process consistency. Manual coiling depends heavily on operator skill and concentration. An automatic winding machine uses defined settings and a repeatable mechanical sequence, helping different production batches achieve a more uniform appearance.
Labor reduction is another important benefit. Manual coiling requires one or more workers to guide, shape, and secure the cable. Automatic operation allows personnel to focus on machine supervision, quality inspection, material preparation, and packing coordination. This can improve labor utilization, particularly in high-volume production environments.
Automatic coiling can also improve production rhythm. A machine running at a listed speed of up to 250 RPM can perform the winding action at a consistent rate, subject to cable characteristics and actual operating settings. A predictable cycle makes it easier to plan output and coordinate the coiler with extrusion, testing, printing, and packaging operations.
Another advantage is packaging compatibility. Manual coils often vary in outside diameter, internal opening, and height. Such variation can make it difficult to load products into standardized boxes. The adjustable hole function and defined coil dimensions help manufacturers prepare a more controlled package format.
The net-type coil is also beneficial for storage and transportation. An organized coil is less likely to unravel or develop severe tangles than an irregular bundle. It can be stacked or placed into a box more efficiently, helping reduce wasted internal space and simplifying later cable removal.
Advantages Compared with Less Flexible Automatic Coilers
Not every automatic coiler provides the same level of packaging flexibility. Some machines are designed for only one fixed coil format or one cable diameter range. The Cross Winder for LAN Cable offers selectable winding with or without a hole, while the hole size can be adjusted through the touch screen. This makes it better suited to manufacturers serving multiple customers or producing different box designs.
The availability of two model versions also supports more targeted equipment selection. The DCW-2540 is suitable for smaller cable diameters from 0.8 to 6 mm. The DCW-2540P expands the applicable range to 1–12 mm and adds pneumatic operation. Instead of forcing every user to purchase a larger or more complex machine, the two configurations allow the equipment to be matched more closely with the intended product range.
The ability to process both LAN cable and coaxial cable can further improve equipment utilization. A factory with several communication cable products may use the same coiling platform for multiple product families, provided the cable dimensions and process requirements fall within the model’s working range.
These features create practical advantages over coilers that are limited to one cable type, one fixed hole dimension, or one fixed packaging size. The machine is not merely designed to rotate a coil; it is designed to support a more adaptable packaging workflow.
Benefits for LAN Cable Manufacturers
Improved Product Presentation
A neat cable coil communicates quality before the package is opened. Customers expect LAN cables to be organized, clean, and easy to handle. The net-type winding pattern gives the finished product a deliberate appearance and helps avoid the disorder associated with loosely bundled cable.
For retail products, a consistent coil can improve the use of transparent packaging or boxes with display windows. For industrial products, it can make warehouse identification and installation preparation easier. In both cases, a clean winding format supports a more professional product presentation.
Reduced Tangling and Handling Problems
Tangled cable creates direct costs. Workers must spend time separating the cable, damaged sections may need to be removed, and the package may no longer meet customer expectations. The organized cross-winding pattern helps keep the cable turns in place and reduces the likelihood of uncontrolled unraveling during normal storage and transport.
Although no winding method can eliminate every possible handling issue, a stable net-type coil provides a stronger foundation for safe packaging than a randomly gathered bundle. The benefit is especially relevant for long cable lengths that are difficult to manage manually.
More Efficient Packaging Preparation
Packaging departments benefit when the product dimensions are predictable. A coil with a defined outside diameter, height, and center-hole option can be matched with a suitable box design. Adjustable hole size is particularly useful when the box includes an internal guide, core, insert, or dispensing feature.
By reducing variation, the machine can help shorten packing cycles. Operators do not need to reshape every coil before placing it in the box. This supports a smoother transition from winding to sealing, labeling, palletizing, or shipment preparation.
Support for Multiple Product Specifications
LAN cable manufacturers often produce several categories and conductor configurations for different markets. Cat5, Cat5e, and Cat6 cables may have different outer diameters and packaging requirements. A machine that can accommodate an applicable diameter range and offer adjustable winding parameters is more useful than a system built around one narrow specification.
The DCW-2540 and DCW-2540P options allow the user to select a configuration based on the intended production range. This can help control capital expenditure while maintaining the required processing capability.
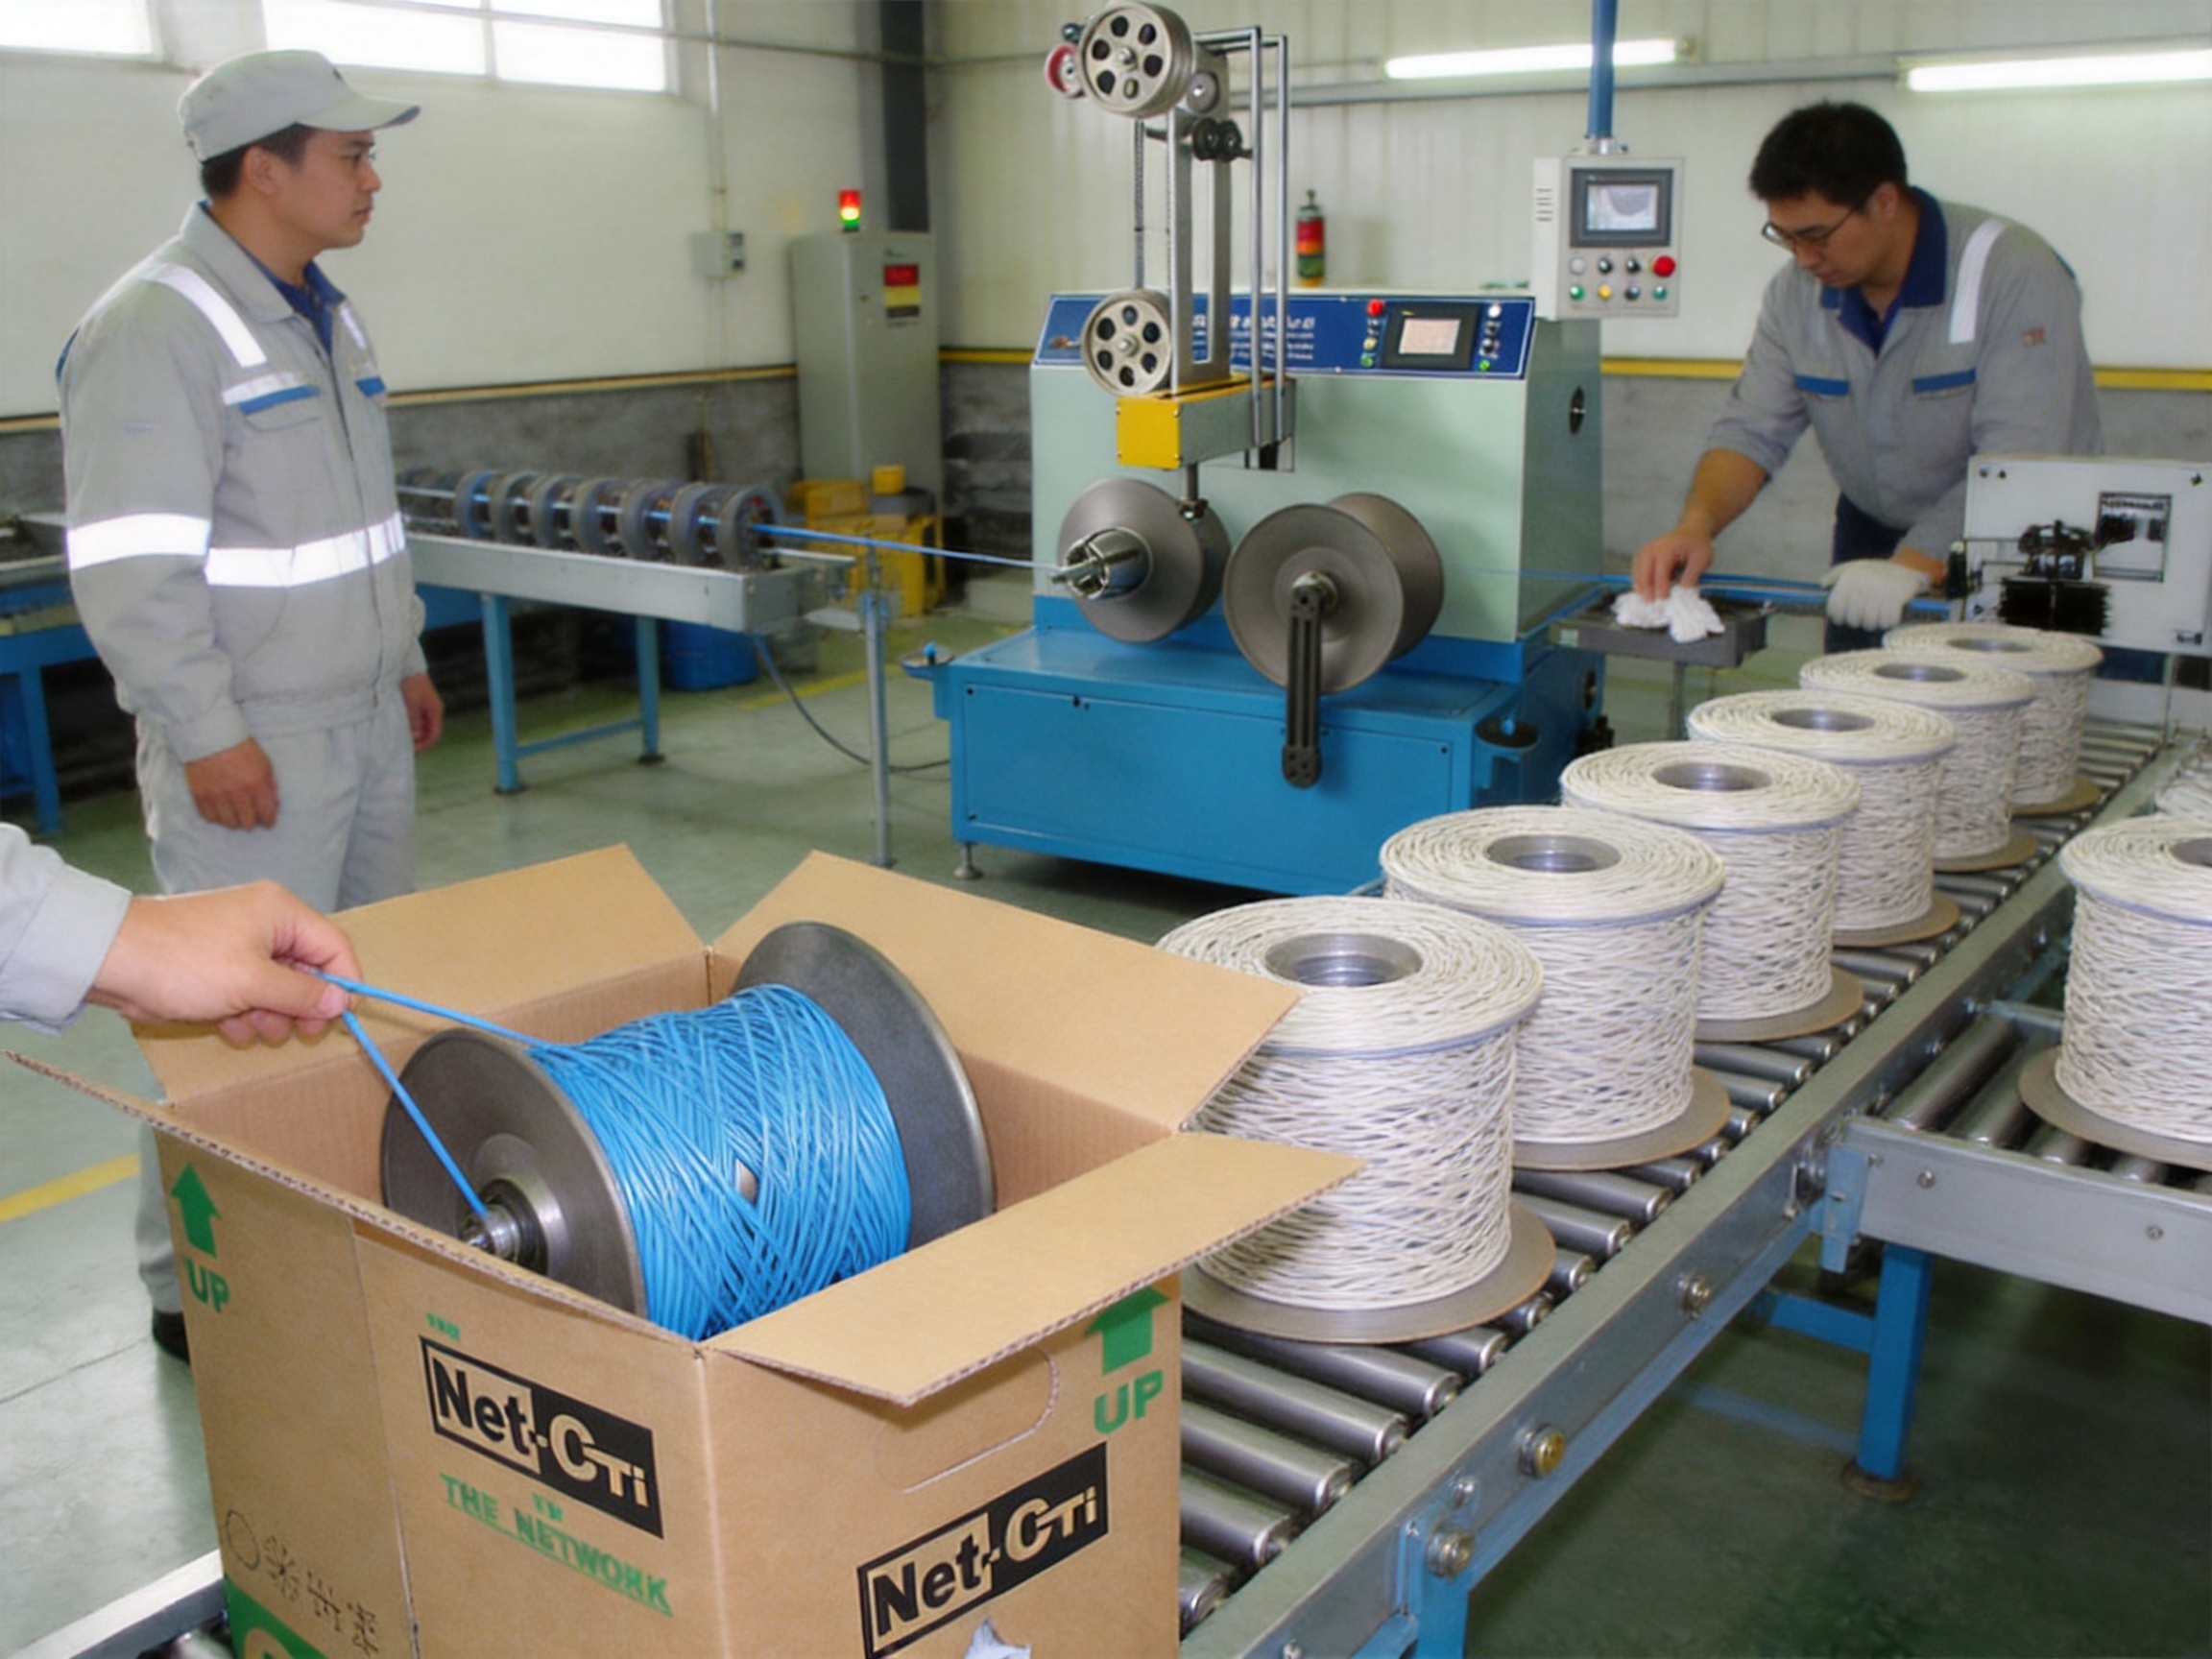
Touch-Screen Operation and Production Flexibility
The touch-screen control system is central to the machine’s ease of use. Instead of relying solely on mechanical adjustments, the operator can select the winding mode and adjust the center-hole size through an interface designed for practical production control.
A touch screen can simplify recipe changes when the factory processes different cable types or box sizes. Once the appropriate parameters have been established, they can be applied consistently for repeated production runs. This reduces the chance of adjustment errors and shortens the time needed to change from one product specification to another.
For new operators, a clear interface can also reduce the training burden. Basic operating instructions, parameter selection, and status checks can be organized in a more accessible format than a machine controlled entirely by manual knobs and mechanical indicators.
Touch-screen operation does not remove the need for experienced supervision. Operators still need to inspect the cable, confirm the model setting, verify the winding result, and respond to abnormal conditions. However, digital adjustment helps make the process more transparent and repeatable.
Recommended Operating Sequence
First, confirm the cable type and diameter. The selected material should fall within the working range of the chosen model. For the DCW-2540, the listed range is 0.8–6 mm. For the DCW-2540P, the listed range is 1–12 mm.
Second, inspect the upstream cable supply. The cable should be free from severe knots, excessive twist, contamination, or damage that could interfere with smooth winding.
Third, select the desired coil format. Choose winding with a center hole or without a center hole according to the packaging plan.
Fourth, enter or adjust the required hole size when the hole-winding mode is selected. The selected value should correspond to the internal dimensions of the packaging box or any supporting component placed inside the coil.
Fifth, start at a controlled setting and inspect the first coil. Check the outside diameter, height, hole size, winding tightness, and overall appearance.
Finally, record the approved settings for future production. Maintaining a parameter record for each cable and package specification can help improve repeatability between shifts and production orders.
Manufacturing Strengths and Engineering Approach
The performance of an automatic coiler depends not only on its visible structure but also on the quality of its engineering, assembly, controls, and production support. As a wire and cable machinery manufacturer, Shanghai Yessjet Precise Machinery Co., Ltd. presents this equipment as part of a broader product portfolio covering wire and cable extrusion lines, fully automatic coiling and packaging equipment, intelligent robot stackers, motorized pay-off equipment, motorized take-up equipment, accessory equipment, and cable extrusion machines.
This broader product range is significant because cable production is rarely limited to one isolated machine. Extrusion, cooling, sizing, printing, testing, pay-off, take-up, coiling, packing, and palletizing must work together. A supplier familiar with several stages of the process can better understand how an individual coiler fits into the complete manufacturing workflow.
The company’s equipment portfolio indicates an engineering focus on cable handling from material input to finished product packaging. For customers seeking a production line rather than a single machine, this can simplify technical communication and system planning. The coiler can be evaluated in relation to upstream cable output, product dimensions, required packing method, and downstream handling.
Process-Oriented Machine Design
A strong manufacturing approach begins with understanding the actual production process. For the Cross Winder for LAN Cable, this includes the cable diameter range, winding format, package dimensions, speed requirements, operator interaction, and transition between winding and packing.
The inclusion of two models shows attention to process matching. The standard configuration is intended for a smaller diameter range, while the pneumatic version is designed for larger cable diameters and a different operating arrangement. This approach helps avoid unnecessary over-sizing while preserving the option for more demanding applications.
The adjustable center-hole function is another example of process-oriented design. A hole is not simply a visual feature; it can affect box dimensions, cable dispensing, internal support, and product handling. Giving the operator control over hole size makes the machine more adaptable to the customer’s packaging system.
Integration with Cable Production Lines
Because the manufacturer also supplies pay-off and take-up equipment, the coiler can be considered as part of a coordinated cable handling system. A motorized pay-off can provide controlled material delivery, while suitable guiding and take-up arrangements can help maintain a stable cable path before coiling.
In a complete line, the coiling machine should be installed with attention to cable direction, floor space, operator access, emergency stopping, electrical supply, compressed air requirements for the pneumatic model, and the location of finished-coil handling equipment. Proper integration can improve safety and productivity while reducing unnecessary cable movement.
For larger projects, the supplier’s experience with intelligent robot stackers and automatic packaging equipment may also support future expansion. A factory may begin with automatic coiling and later add automated packing, case handling, or palletizing as production volume grows.
Quality Control Considerations
Manufacturing quality should be evaluated at several levels. Mechanical parts must be assembled accurately so that the cable guide and winding mechanism operate smoothly. Control functions should respond reliably to operator input. Pneumatic components in the DCW-2540P should be selected and maintained for stable operation. Finished coils should be inspected against defined acceptance criteria.
Important checks include coil outside diameter, height, center-hole diameter, winding density, cable surface condition, and ease of removal from the winding area. Production teams should also verify that the coiling operation does not negatively affect electrical or mechanical cable performance.
Documented inspection procedures help convert machine performance into repeatable manufacturing quality. The final result depends on both the equipment and the discipline of the production process.
Installation and Production Planning
Before installation, the user should confirm the available floor space and the material flow around the machine. The operator needs sufficient room to load cable, monitor the winding process, remove completed coils, and perform routine maintenance.
The production area should also provide the utilities required by the selected model. The DCW-2540 specification lists no pneumatic requirement, while the DCW-2540P is identified as pneumatic. Customers selecting the pneumatic model should confirm the required air supply conditions with the equipment supplier before installation.
Electrical supply, grounding, ventilation, lighting, and emergency access should be planned in accordance with local industrial requirements. Cable should not be allowed to run across walkways where it could create a trip hazard or be damaged by other equipment.
Packaging materials should be prepared before production trials. If the machine is configured to create a central hole, the trial box should represent the final packaging design as closely as possible. This allows the operator to verify the relationship between hole size, coil dimensions, box clearance, and product insertion.
Commissioning Procedure
Commissioning should begin with a visual inspection of the machine, cable path, control panel, and safety devices. The operator should confirm that moving parts are clear and that all protective measures are in place.
A low-risk test should then be performed without production material or at a controlled initial condition, depending on the supplier’s operating instructions. This helps verify the direction of movement and the response of the controls.
The first cable trial should use a representative product. The operator should observe the formation of the net-type coil and make gradual adjustments rather than changing multiple parameters at once.
After an acceptable coil is produced, the dimensions and appearance should be recorded. The result should be tested in the intended package. If the coil fits correctly and the cable remains orderly, the settings can be approved for routine production.
Maintenance and Long-Term Performance
Routine maintenance is essential for preserving consistent coiling quality. Cable dust, jacket particles, and packaging debris can accumulate around guides, sensors, moving supports, and winding components. Regular cleaning helps maintain smooth movement and reliable detection.
Operators should inspect the cable guide path for wear or sharp edges. Any damaged guide surface could mark the cable jacket or affect the way the cable enters the winding area. Mechanical fasteners, drive components, and adjustment points should be checked according to the maintenance schedule supplied with the equipment.
For the pneumatic DCW-2540P, air quality and pressure stability are important. Moisture, oil contamination, or insufficient pressure can affect pneumatic components. A suitable air preparation system and regular inspection can help protect the equipment.
The touch-screen interface should be kept clean and protected from excessive dust or impact. Production settings should be backed up or recorded so that approved recipes can be restored after maintenance or product changes.
Maintenance records should include inspection dates, replaced parts, abnormal conditions, and corrective actions. These records help identify recurring issues before they cause extended downtime.
Safety Considerations
Automatic winding equipment contains moving components that can create pinch, entanglement, or impact hazards. Operators should receive training before using the machine and should understand the function of emergency stops and protective devices.
Loose clothing, jewelry, and unsecured long hair should be kept away from moving cable and rotating parts. Operators should never reach into the winding area while the machine is operating. Any adjustment, cleaning, or maintenance inside a hazardous area should be performed only after the machine has been stopped and isolated according to the factory’s safety procedure.
The cable path should be kept clear. A sudden obstruction can increase tension or cause the cable to move unpredictably. Operators should stop the machine if they observe unusual vibration, noise, cable damage, control errors, or irregular coil formation.
Safety instructions should be adapted to local regulations and the final line configuration. The user remains responsible for establishing a complete risk assessment, training program, and lockout procedure for the installation.
Choosing Between DCW-2540 and DCW-2540P
The DCW-2540 is a suitable choice when the cable diameter is within the listed 0.8–6 mm range and the production line does not require the pneumatic configuration. It offers a practical solution for many standard LAN cable applications and can support the automatic formation of neat net-type coils.
The DCW-2540P is intended for a broader listed cable diameter range of 1–12 mm and includes pneumatic operation. It may be preferable for manufacturers handling larger communication cables, coaxial cables, or products requiring the additional operating capability provided by the pneumatic system.
The final decision should not be based only on the largest cable diameter. Users should also consider product mix, expected future expansion, packaging design, operating environment, utility availability, and the level of automation desired. Sample testing is recommended when the cable construction is unusual or when the packaging requirements are highly specific.
| Selection Factor | DCW-2540 | DCW-2540P |
|---|---|---|
| Listed cable diameter | 0.8–6 mm | 1–12 mm |
| Listed maximum speed | 250 RPM | 250 RPM |
| Coil height | 250 mm | 250 mm |
| Outside diameter | 400 mm | 400 mm |
| Inside diameter | 180 mm | 180 mm |
| Pneumatic operation | No | Yes |
| Typical selection logic | Standard smaller-diameter cable applications | Broader diameter range and pneumatic requirements |
Applications Beyond Standard LAN Cable
The primary application is LAN cable, including Cat5, Cat5e, and Cat6 products. These cables are commonly manufactured for network installations, structured cabling, communication systems, and data infrastructure projects.
The machine is also applicable to coaxial cable within the stated working conditions. This broadens its usefulness for manufacturers that produce communication cable, signal cable, and related products on the same or similar production platform.
Potential application suitability should always be confirmed through cable samples. Cable stiffness, jacket material, construction, and outer diameter influence the winding process. A cable that falls within the dimensional range may still require parameter adjustment to achieve the desired coil quality.
Return on Investment Considerations
The value of an automatic coiler comes from more than its rotational speed. A proper evaluation should include labor savings, output consistency, reduced rework, packaging efficiency, product presentation, and the ability to handle multiple cable types.
If manual coiling requires several workers or creates a bottleneck before packing, automation can release labor for higher-value tasks. If irregular coils lead to damaged packaging or customer complaints, improved winding consistency can reduce hidden quality costs.
Flexible hole adjustment may also reduce packaging complexity. A single adjustable machine can support several box formats instead of requiring separate coiling arrangements for each central opening. This can be particularly valuable for contract manufacturers or suppliers serving multiple brands.
Equipment utilization is another important factor. A machine that can process several LAN cable categories and coaxial cable products may be used for more hours per day than a dedicated single-product machine. Higher utilization can improve the economic return on the equipment investment.
Before purchase, users should estimate the current manual labor cost, production volume, number of product changes, average coil length, packaging cost, and expected operating hours. These figures can then be compared with the planned automation investment and projected maintenance cost.
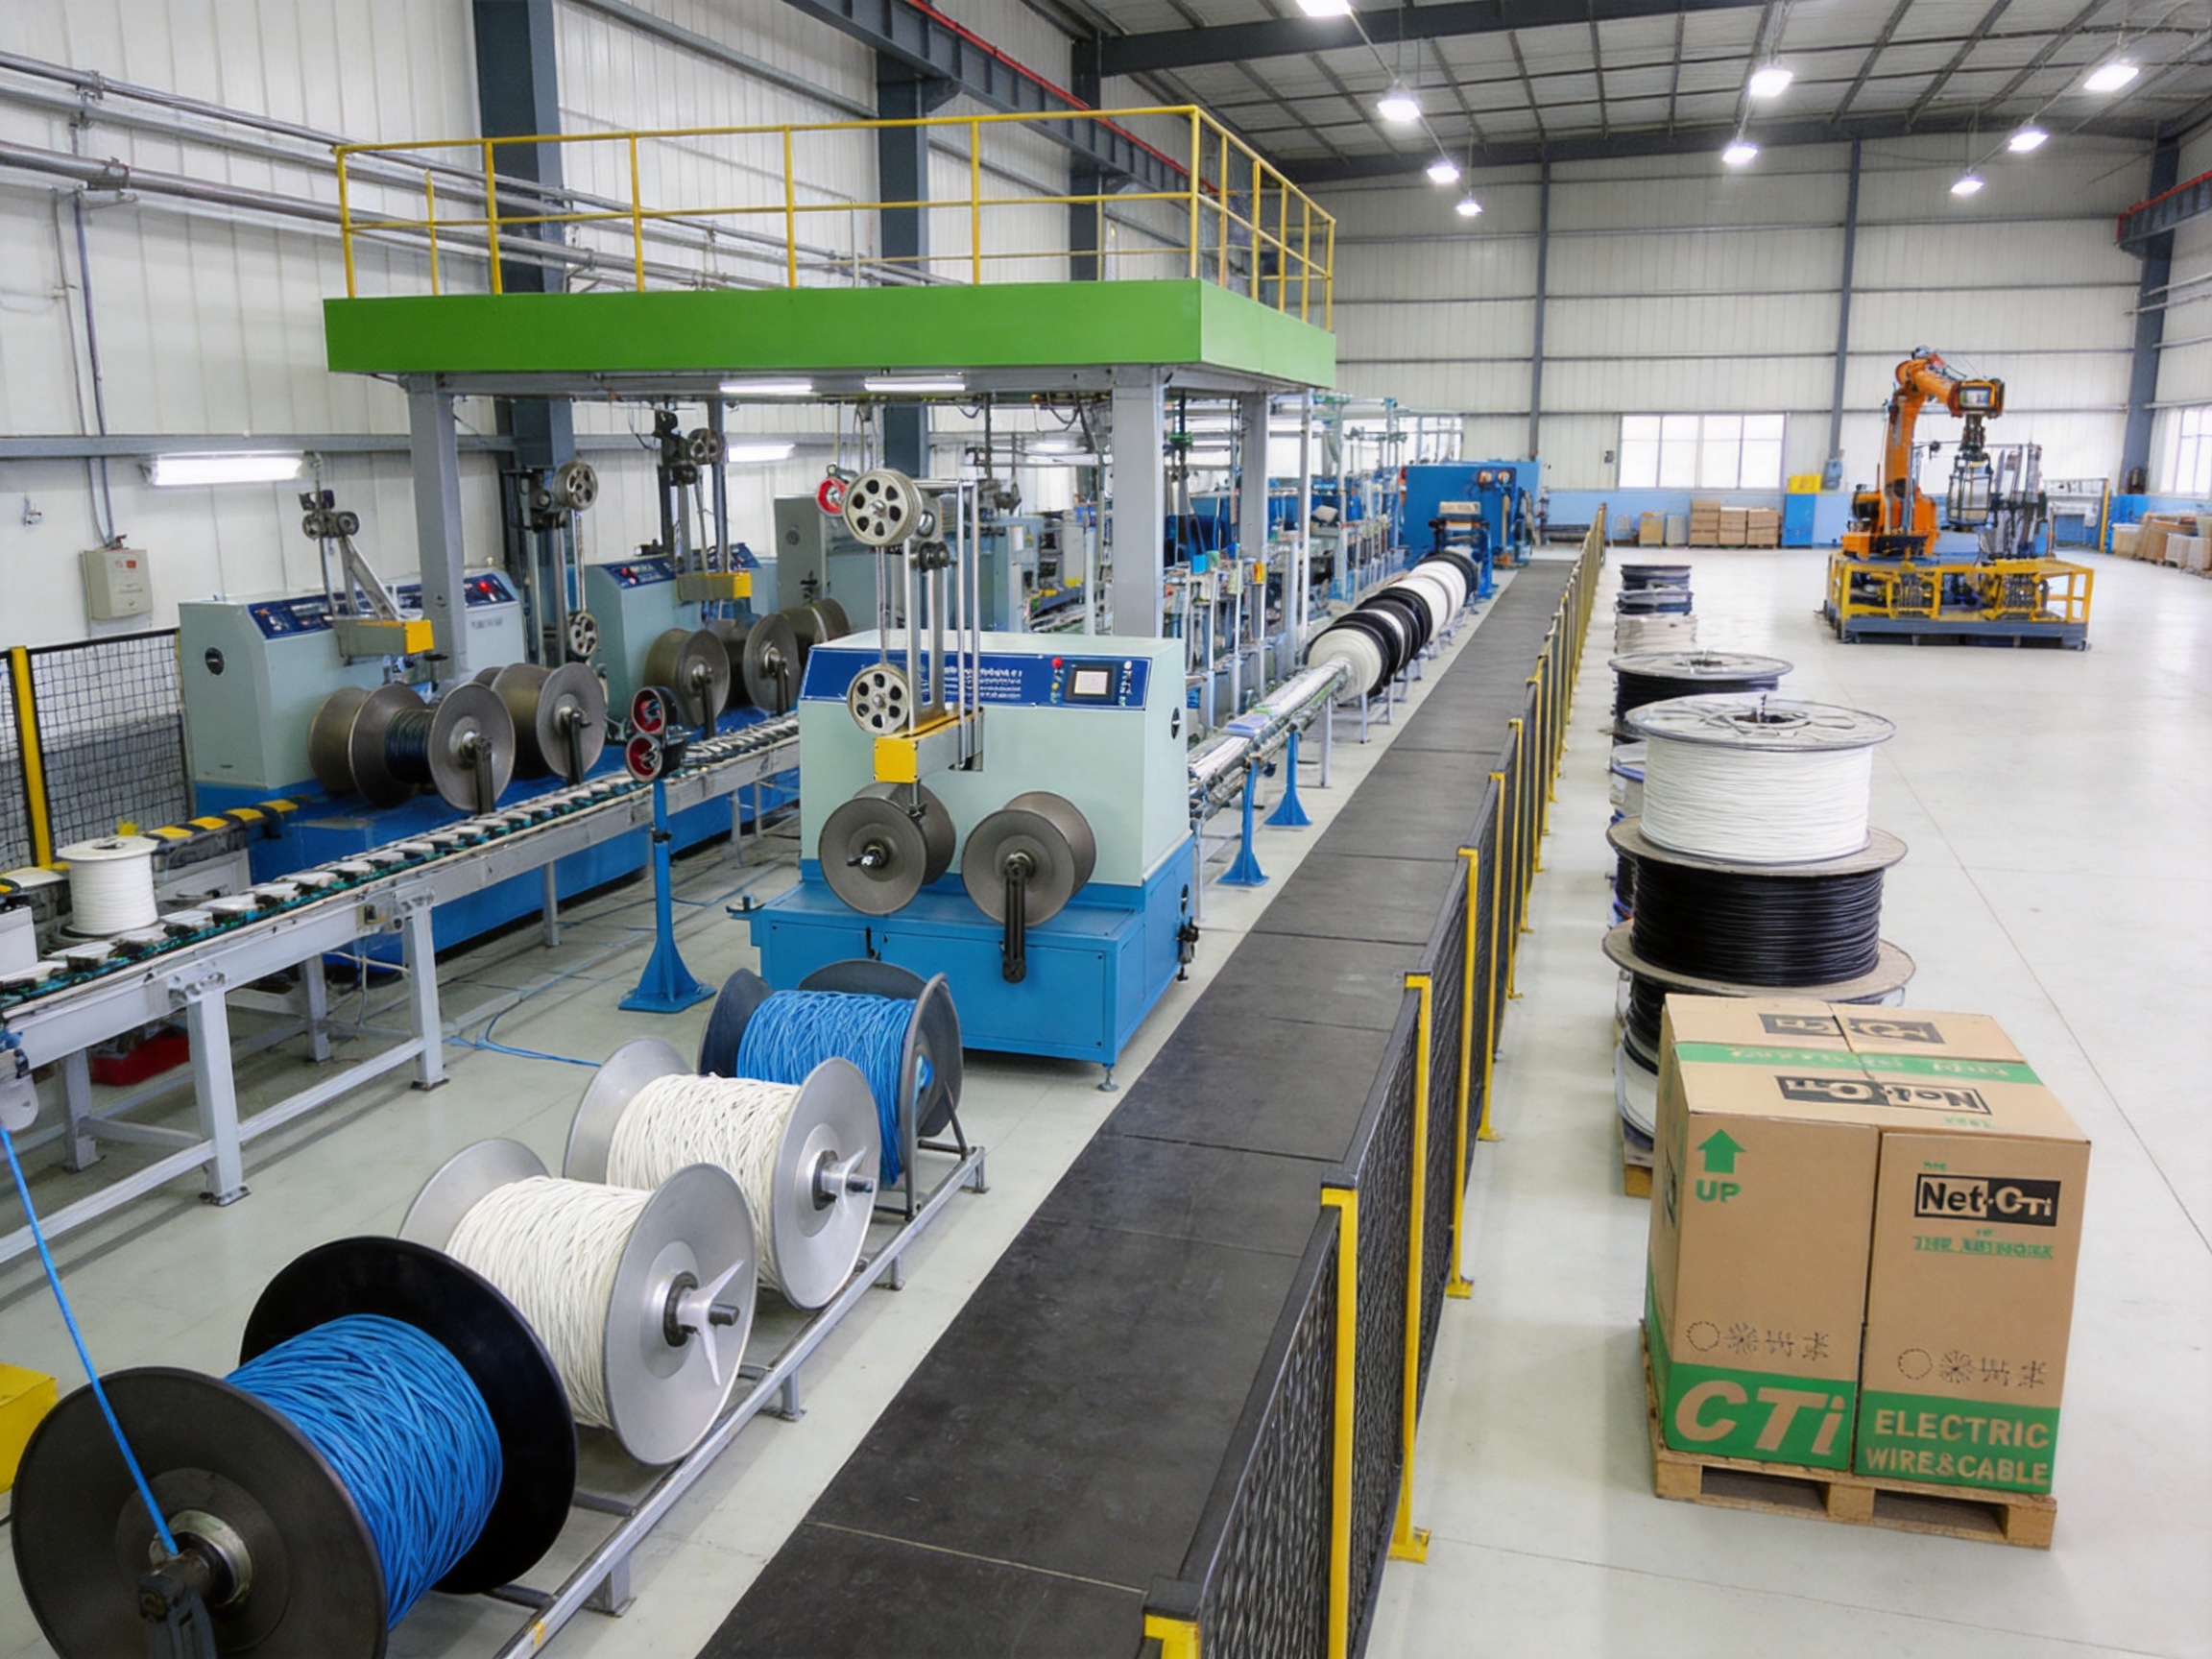
Why Supplier Support Matters
A coiling machine performs best when the supplier understands both the equipment and the customer’s cable products. Technical discussions should cover cable diameter, insulation and jacket materials, coil dimensions, winding length, center-hole requirements, box design, upstream equipment, downstream packing, and expected production capacity.
Shanghai Yessjet Precise Machinery Co., Ltd. provides wire and cable machinery and positions its product range around cable production turnkey solutions. Its wider equipment portfolio includes extrusion machinery, pay-off and take-up systems, coiling and packaging equipment, accessory equipment, and intelligent robot stackers.
This combination can be useful for customers planning a new cable production line or upgrading an existing factory. Instead of treating coiling as an isolated purchase, the user can evaluate how the machine will interact with cable extrusion, material handling, packaging, and palletizing equipment.
Supplier communication is especially important when the customer needs custom packaging dimensions, special cable construction, multiple product recipes, or integration with existing line controls. A clear technical specification and sample-testing process can reduce uncertainty before installation.
Information to Provide During an Inquiry
Customers should provide the cable type, nominal and maximum outside diameter, cable material, desired coil outside diameter, target coil height, center-hole requirement, hole size range, package dimensions, production speed, and expected daily output.
It is also helpful to provide photographs or drawings of the existing production line, details of the upstream pay-off, and information about available electrical and pneumatic utilities. If multiple cable products will be processed, a complete product list allows the supplier to recommend the most suitable model and operating strategy.
Samples of the actual cable and packaging box can provide the most reliable basis for testing. The supplier can then assess winding behavior, coil stability, package fit, and adjustment requirements.
Frequently Asked Questions
What types of LAN cable can the machine process?
The machine is designed for Cat5, Cat5e, and Cat6 LAN cables. It can also be used for coaxial cable within the applicable model range and after confirming the cable’s winding characteristics.
Can the machine produce a coil without a center hole?
Yes. The machine allows the operator to select winding with a hole or without a hole, depending on the packaging and product requirements.
Can the center-hole size be changed?
Yes. The hole size can be adjusted through the touch-screen interface. This allows the coil to be matched with different packaging box dimensions or internal support designs.
What is the maximum listed speed?
Both the DCW-2540 and DCW-2540P are listed with a maximum speed of 250 RPM. Actual production speed may depend on cable construction, winding settings, tension, operator adjustments, and the required coil quality.
What cable diameter can the DCW-2540 process?
The stated cable diameter range for the DCW-2540 is 0.8–6 mm.
What cable diameter can the DCW-2540P process?
The stated cable diameter range for the DCW-2540P is 1–12 mm. This model also includes pneumatic operation.
What are the listed coil dimensions?
Both models are listed with a coil height of 250 mm, an outside diameter of 400 mm, and an inside diameter of 180 mm.
Why is the net-type coil useful?
The net-type coil creates a more orderly arrangement of cable turns. It helps reduce tangling, supports easier handling, and provides a cleaner format for storage and packaging.
Is the machine suitable for a packaging line?
Yes. It is designed for automatic cable coiling before packaging and can be used as part of a broader line that includes pay-off equipment, take-up equipment, packing equipment, and other cable handling machinery.
Does the machine eliminate the need for operators?
No. Automation reduces manual coiling work, but operators are still needed for material preparation, parameter selection, quality checks, machine supervision, product removal, and routine maintenance.
How should the correct model be selected?
The selection should be based on cable diameter, cable type, required winding format, packaging design, pneumatic utility availability, production volume, and future product plans. Sample testing is recommended for final confirmation.
Can one machine process different cable products?
It may process different LAN and coaxial cable products when their dimensions and winding characteristics fall within the applicable range. Each product may require its own approved operating parameters.
What should be checked during a production trial?
Users should check the coil outside diameter, height, center-hole size, winding tightness, net-type arrangement, cable surface condition, package fit, and the ease with which the cable can be removed or dispensed.
What maintenance is normally required?
Routine maintenance generally includes cleaning cable debris, inspecting guides and moving parts, checking fasteners and drive components, reviewing control functions, and maintaining pneumatic equipment on the pneumatic model. The supplier’s maintenance instructions should be followed for specific intervals and procedures.
Conclusion
The Cross Winder for LAN Cable provides a practical solution for manufacturers seeking to automate the final handling and packaging stage of LAN cable production. Its ability to process Cat5, Cat5e, Cat6, and applicable coaxial cables makes it useful for a range of communication cable products. The net-type winding method creates an organized coil that is easier to store, transport, and place into packaging.
The machine’s most distinctive advantages are its automatic operation, adjustable center-hole size, selectable hole or hole-free winding, and availability in two configurations. The DCW-2540 supports cable diameters from 0.8 to 6 mm without a listed pneumatic requirement, while the DCW-2540P supports 1–12 mm cables and includes pneumatic operation. Both models provide listed coil dimensions of 250 mm in height, 400 mm in outside diameter, and 180 mm in inside diameter, with a maximum listed speed of 250 RPM.
Compared with manual coiling or less adaptable automatic systems, the machine can improve consistency, reduce labor demand, support multiple packaging formats, and reduce tangling during storage and transport. Its value is further strengthened when it is integrated with suitable pay-off, take-up, extrusion, packaging, and palletizing equipment.
As part of a broader wire and cable machinery portfolio, the equipment reflects a process-oriented approach to cable manufacturing. For companies planning a new production line or upgrading an existing facility, the Cross Winder for LAN Cable can serve as an important link between cable production and finished-product packaging.
References
1. Product specification sheet for the Cross Winder for LAN Cable, including DCW-2540 and DCW-2540P model data.
2. Industrial cable handling and packaging practices for communication cable production.
3. General principles of wire and cable extrusion, pay-off, take-up, coiling, and packaging line integration.
4. Manufacturer-provided information concerning automatic coiling equipment, cable production machinery, and turnkey line solutions.
5. General industrial guidance on machine safety, preventive maintenance, cable tension control, and production quality management.