LANGUAGE
 中文简体
 русский
 Français
 Español
 Português
 عربى
Content
- 1 What Is an Accumulator Dancer?
- 2 Main Functions of a Cable Storage Rack
- 3 Vertical and Horizontal Accumulator Configurations
- 4 Technical Specifications and Model Selection
- 5 Advantages Compared with Basic Cable Storage Methods
- 6 Application in Extrusion Lines
- 7 Application in CV Lines
- 8 Application in Rewinding and Take-Up Lines
- 9 Manufacturing and Engineering Strengths
- 10 How the Accumulator Improves Operational Efficiency
- 11 Installation Planning
- 12 Operation and Maintenance Recommendations
- 13 Selection Guide for Cable Manufacturers
- 14 Why Choose a Specialized Manufacturer?
- 15 Typical Customer Benefits
- 16 Q&A: Accumulator Dancer Cable Storage Rack
- 16.1 What is the main purpose of an accumulator dancer?
- 16.2 Where can the cable storage rack be installed?
- 16.3 What is the difference between vertical and horizontal types?
- 16.4 Can the accumulation capacity be customized?
- 16.5 How should the model be selected?
- 16.6 What cable diameter range is covered by the listed models?
- 16.7 How does the accumulator protect cable?
- 16.8 Can it be used with both payoff and take-up equipment?
- 16.9 Does the accumulator replace all production controls?
- 16.10 Why work with a manufacturer of complete cable machinery?
- 16.11 What information should be provided when requesting a quotation?
- 17 Conclusion
- 18 References
- 19 Product: Accumulator Dancer(cable storage rack)
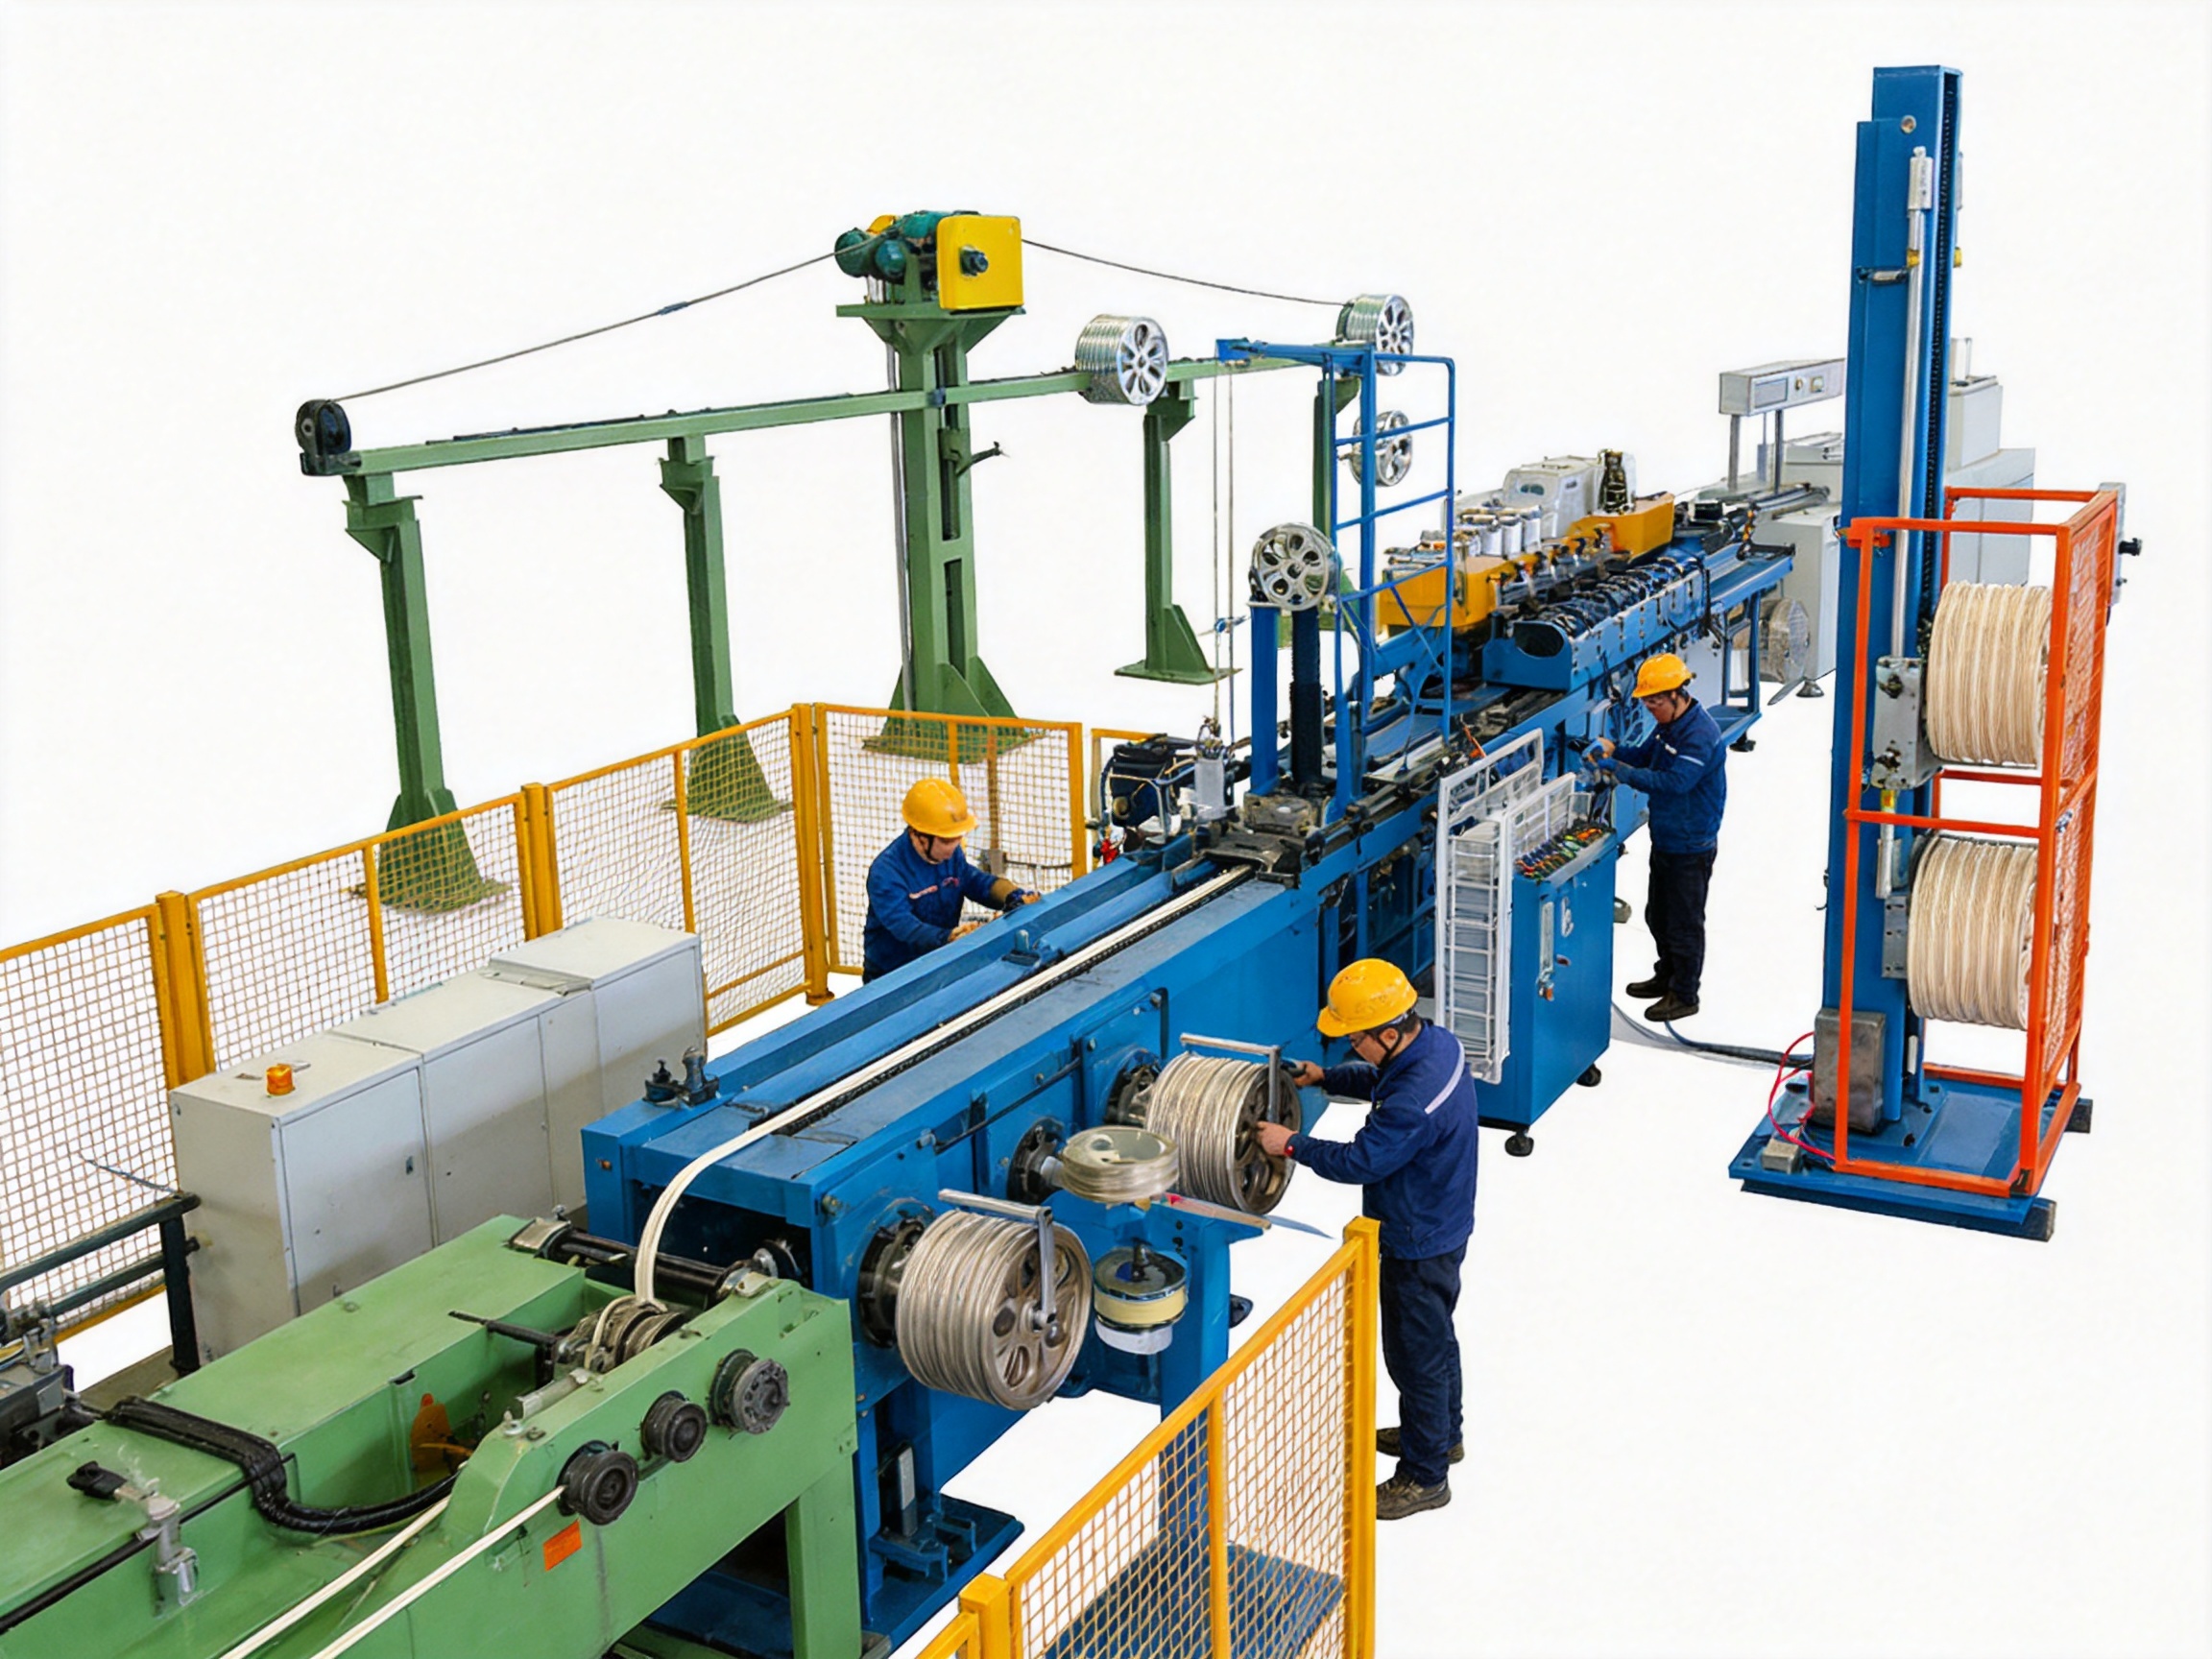
In modern wire and cable manufacturing, production continuity is just as important as extrusion speed, conductor quality, and finished-product accuracy. A cable line may operate at high speed for many hours, yet a reel changeover can interrupt the entire process if the cable cannot be temporarily stored, controlled, and released in a stable manner. The accumulator dancer, also known as a cable storage rack or wire accumulator, is designed to solve this challenge.
An accumulator dancer provides a controlled reserve of cable between process stages. It supports the cable, maintains an organized path, reduces unnecessary contact with surrounding structures, and allows upstream or downstream equipment to continue operating while a reel is being replaced. In extrusion, CV, rewinding, and related production lines, this function can make a substantial difference to productivity, cable protection, and operating convenience.
The equipment is available in vertical and horizontal configurations, with accumulation capacities that can be adapted to specific production requirements. The range includes models with different wheel diameters, wheel quantities, cable diameter ranges, and storage capacities. This flexibility allows manufacturers to select an accumulator that matches the cable structure, line speed, installation space, and reel-change procedure.
For cable producers seeking a practical way to reduce stoppages and improve material handling, the accumulator dancer is more than a passive storage device. It is an important part of a coordinated wire and cable production line. Its combination of cable support, controlled accumulation, compact structure, and application flexibility makes it suitable for both standard production environments and customized turnkey solutions.
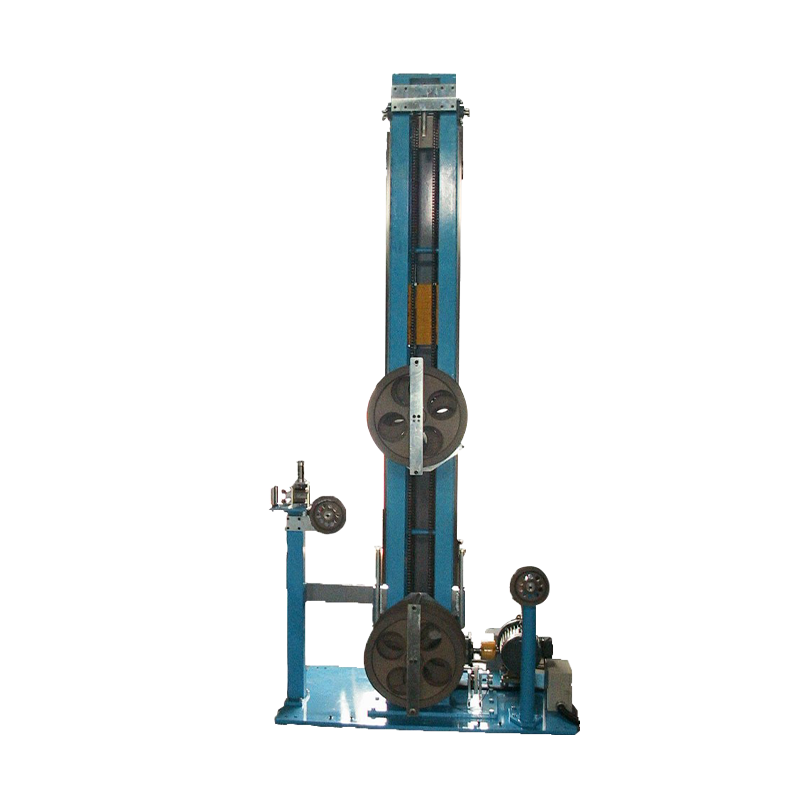
Accumulator Dancer(cable storage rack)
What Is an Accumulator Dancer?
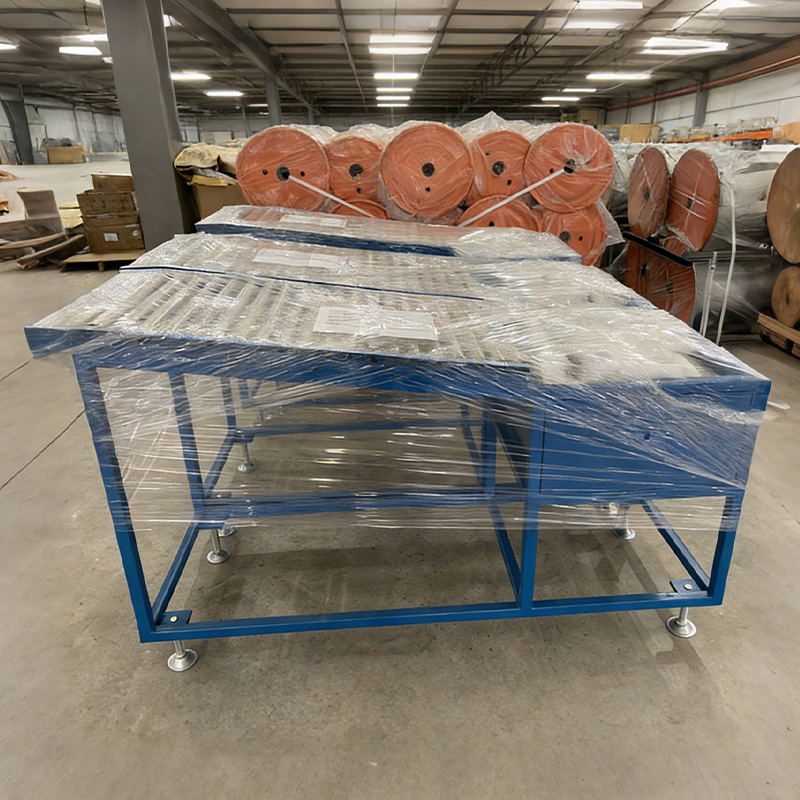
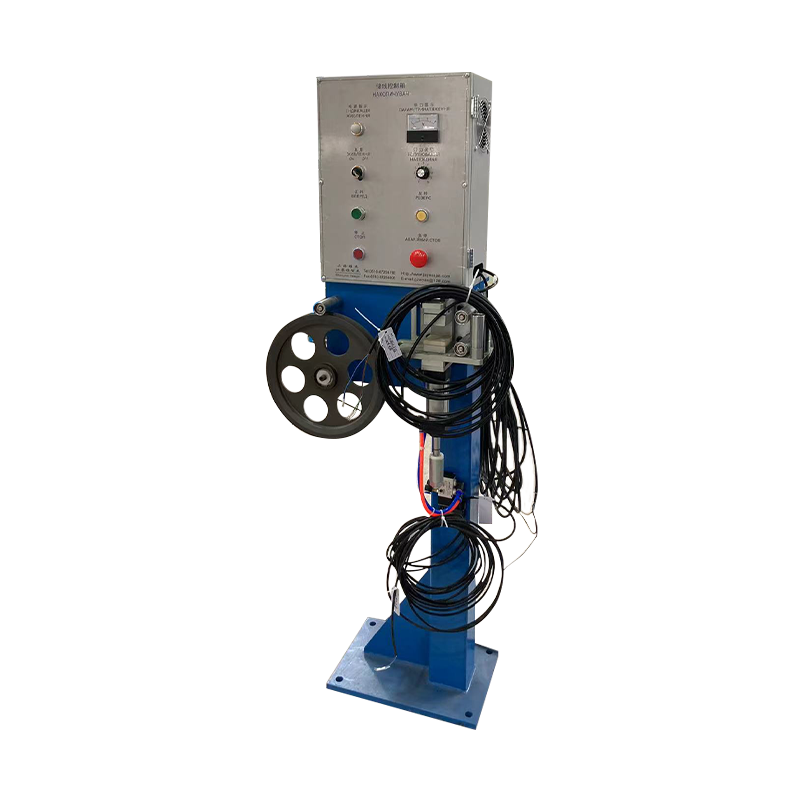
An accumulator dancer is a mechanical cable storage and control unit installed within a wire or cable processing line. It usually consists of a frame, a series of cable-guiding wheels or rollers, a moving or adjustable section, and supporting components that create a temporary cable reserve. The cable travels through the wheel arrangement in a controlled path. When the line requires additional cable during a reel changeover, the stored cable is released gradually so that production can continue.
The term “dancer” refers to the way the equipment can respond to cable movement and tension changes. Depending on the line design, the dancer section may move, adjust, or provide a controlled path that helps balance cable supply and take-up. This assists in maintaining a stable cable flow when the speed or operating condition of one part of the line changes.
In practical operation, the accumulator is positioned between two cable-handling processes. The upstream equipment may be an extrusion line, a payoff system, or another processing unit. The downstream equipment may be a take-up, coiling machine, rewinding machine, or packaging system. The accumulator provides a temporary buffer between these stages.
During normal production, the cable passes through the accumulator at a controlled speed. During reel replacement, the cable already stored in the unit supplies the line for a short period. This gives operators time to remove an empty reel, install a new reel, connect the cable, and restore the normal supply path without immediately stopping the main production process.
The storage capacity depends on the number and diameter of the wheels, the distance between the wheel groups, the cable diameter, and the overall machine design. Because cable products vary greatly in size and flexibility, an accumulator must be selected according to the actual production application rather than simply by physical size.
Main Functions of a Cable Storage Rack
Supporting and Fixing the Cable
The first function of the cable storage rack is to support and guide the cable during processing. Instead of allowing the cable to rest on the floor, rub against a machine frame, or form uncontrolled loops, the accumulator organizes the cable through a defined wheel path.
A controlled path helps prevent accidental contact with sharp edges, hot surfaces, moving components, or contaminated areas. It also makes the cable easier for operators to observe and manage. The supporting structure helps preserve a consistent route from one process to the next, which is especially valuable in long production lines.
Protecting the Cable from Wear and Damage
Cable insulation and outer sheaths can be damaged by excessive bending, dragging, impact, or repeated friction. A properly designed accumulator reduces these risks by guiding the cable around dedicated wheels or rollers. The cable is held away from the floor and is less likely to be caught by nearby equipment.
The wheel diameter is an important selection factor. Models with larger wheels are generally more suitable for larger cable diameters or applications in which a larger bending radius is required. Proper matching between cable diameter and wheel diameter helps reduce mechanical stress and supports stable product quality.
Maintaining Production During Reel Changeover
The most important productivity advantage of an accumulator is its ability to provide temporary cable storage during reel replacement. Without a storage section, the line may need to stop whenever the payoff reel becomes empty or the take-up reel must be changed. Each stoppage can create material waste, require repeated machine adjustments, and reduce effective operating time.
With a correctly sized accumulator, stored cable can continue feeding the line while operators complete the reel-change procedure. This minimizes interruptions and helps keep the process stable. The exact available time depends on the accumulation capacity and production speed, but even a relatively short buffer can simplify changeover work and prevent unnecessary emergency stops.
Controlling Payoff and Take-Up
The accumulator can also help coordinate the speed relationship between payoff and take-up equipment. Cable production is not always perfectly synchronized. One machine may accelerate, decelerate, or pause while another continues operating. The storage rack absorbs part of this difference and helps maintain a more orderly cable flow.
This function is especially useful in extrusion, CV, and rewind lines. The unit can be positioned according to the production layout and process requirements. In some applications, it supports payoff control; in others, it provides a buffer before take-up or rewinding. The final arrangement should be determined by cable type, line speed, reel dimensions, and the required operating sequence.
Improving Cable Maintenance and Management
A rational storage structure makes the cable easier to inspect, access, and maintain. Operators can identify the cable route more quickly, check for irregular movement, and locate potential problems before they affect finished-product quality.
Organized cable management also reduces the chance of tangling and makes the working area easier to clean. A clear cable path supports safer operation and simplifies routine adjustments. For plants producing multiple cable types, this improved organization can help reduce changeover confusion and improve production discipline.
Vertical and Horizontal Accumulator Configurations
Vertical Type Accumulator
A vertical accumulator arranges its storage path in an upright structure. This configuration is often selected when floor space is limited but sufficient vertical clearance is available. By using the height of the production area, a vertical unit can provide useful accumulation without occupying an unnecessarily large footprint.
Vertical designs can be integrated into extrusion and cable processing lines where the cable path naturally rises or descends between machine sections. They can also be suitable when the production layout requires clear access around the floor-level operating area.
The vertical design should be evaluated in relation to plant height, overhead structures, cable entry and exit elevation, maintenance access, and operator visibility. A well-planned installation allows the cable to travel smoothly without creating sharp bends or difficult service points.
Horizontal Type Accumulator
A horizontal accumulator uses a longer, lower arrangement for cable storage. It is appropriate when the plant has sufficient floor length but limited vertical clearance. Horizontal equipment may also be convenient when the upstream and downstream machines are positioned at a similar height.
This design can make certain operating points easily accessible from ground level. It may be preferred in workshops where operators need direct access to the cable path or where overhead clearance is restricted by building structures, cranes, ventilation systems, or other machinery.
Horizontal and vertical types perform the same fundamental storage and control function, but their installation requirements differ. The best choice depends on the production line layout, cable direction, available space, maintenance preferences, and required accumulation capacity.
Customized Configuration
Not every cable line has the same process speed, product range, or reel-change procedure. For this reason, accumulation capacity can be produced according to customer requirements. Customization may involve the storage length, wheel diameter, number of wheels, frame arrangement, cable entry and exit positions, or the overall equipment orientation.
Customization is particularly useful for manufacturers producing different cable diameters or operating several lines with different process conditions. A properly engineered design avoids the limitations of a one-size-fits-all machine and allows the accumulator to become an integrated part of the complete production system.
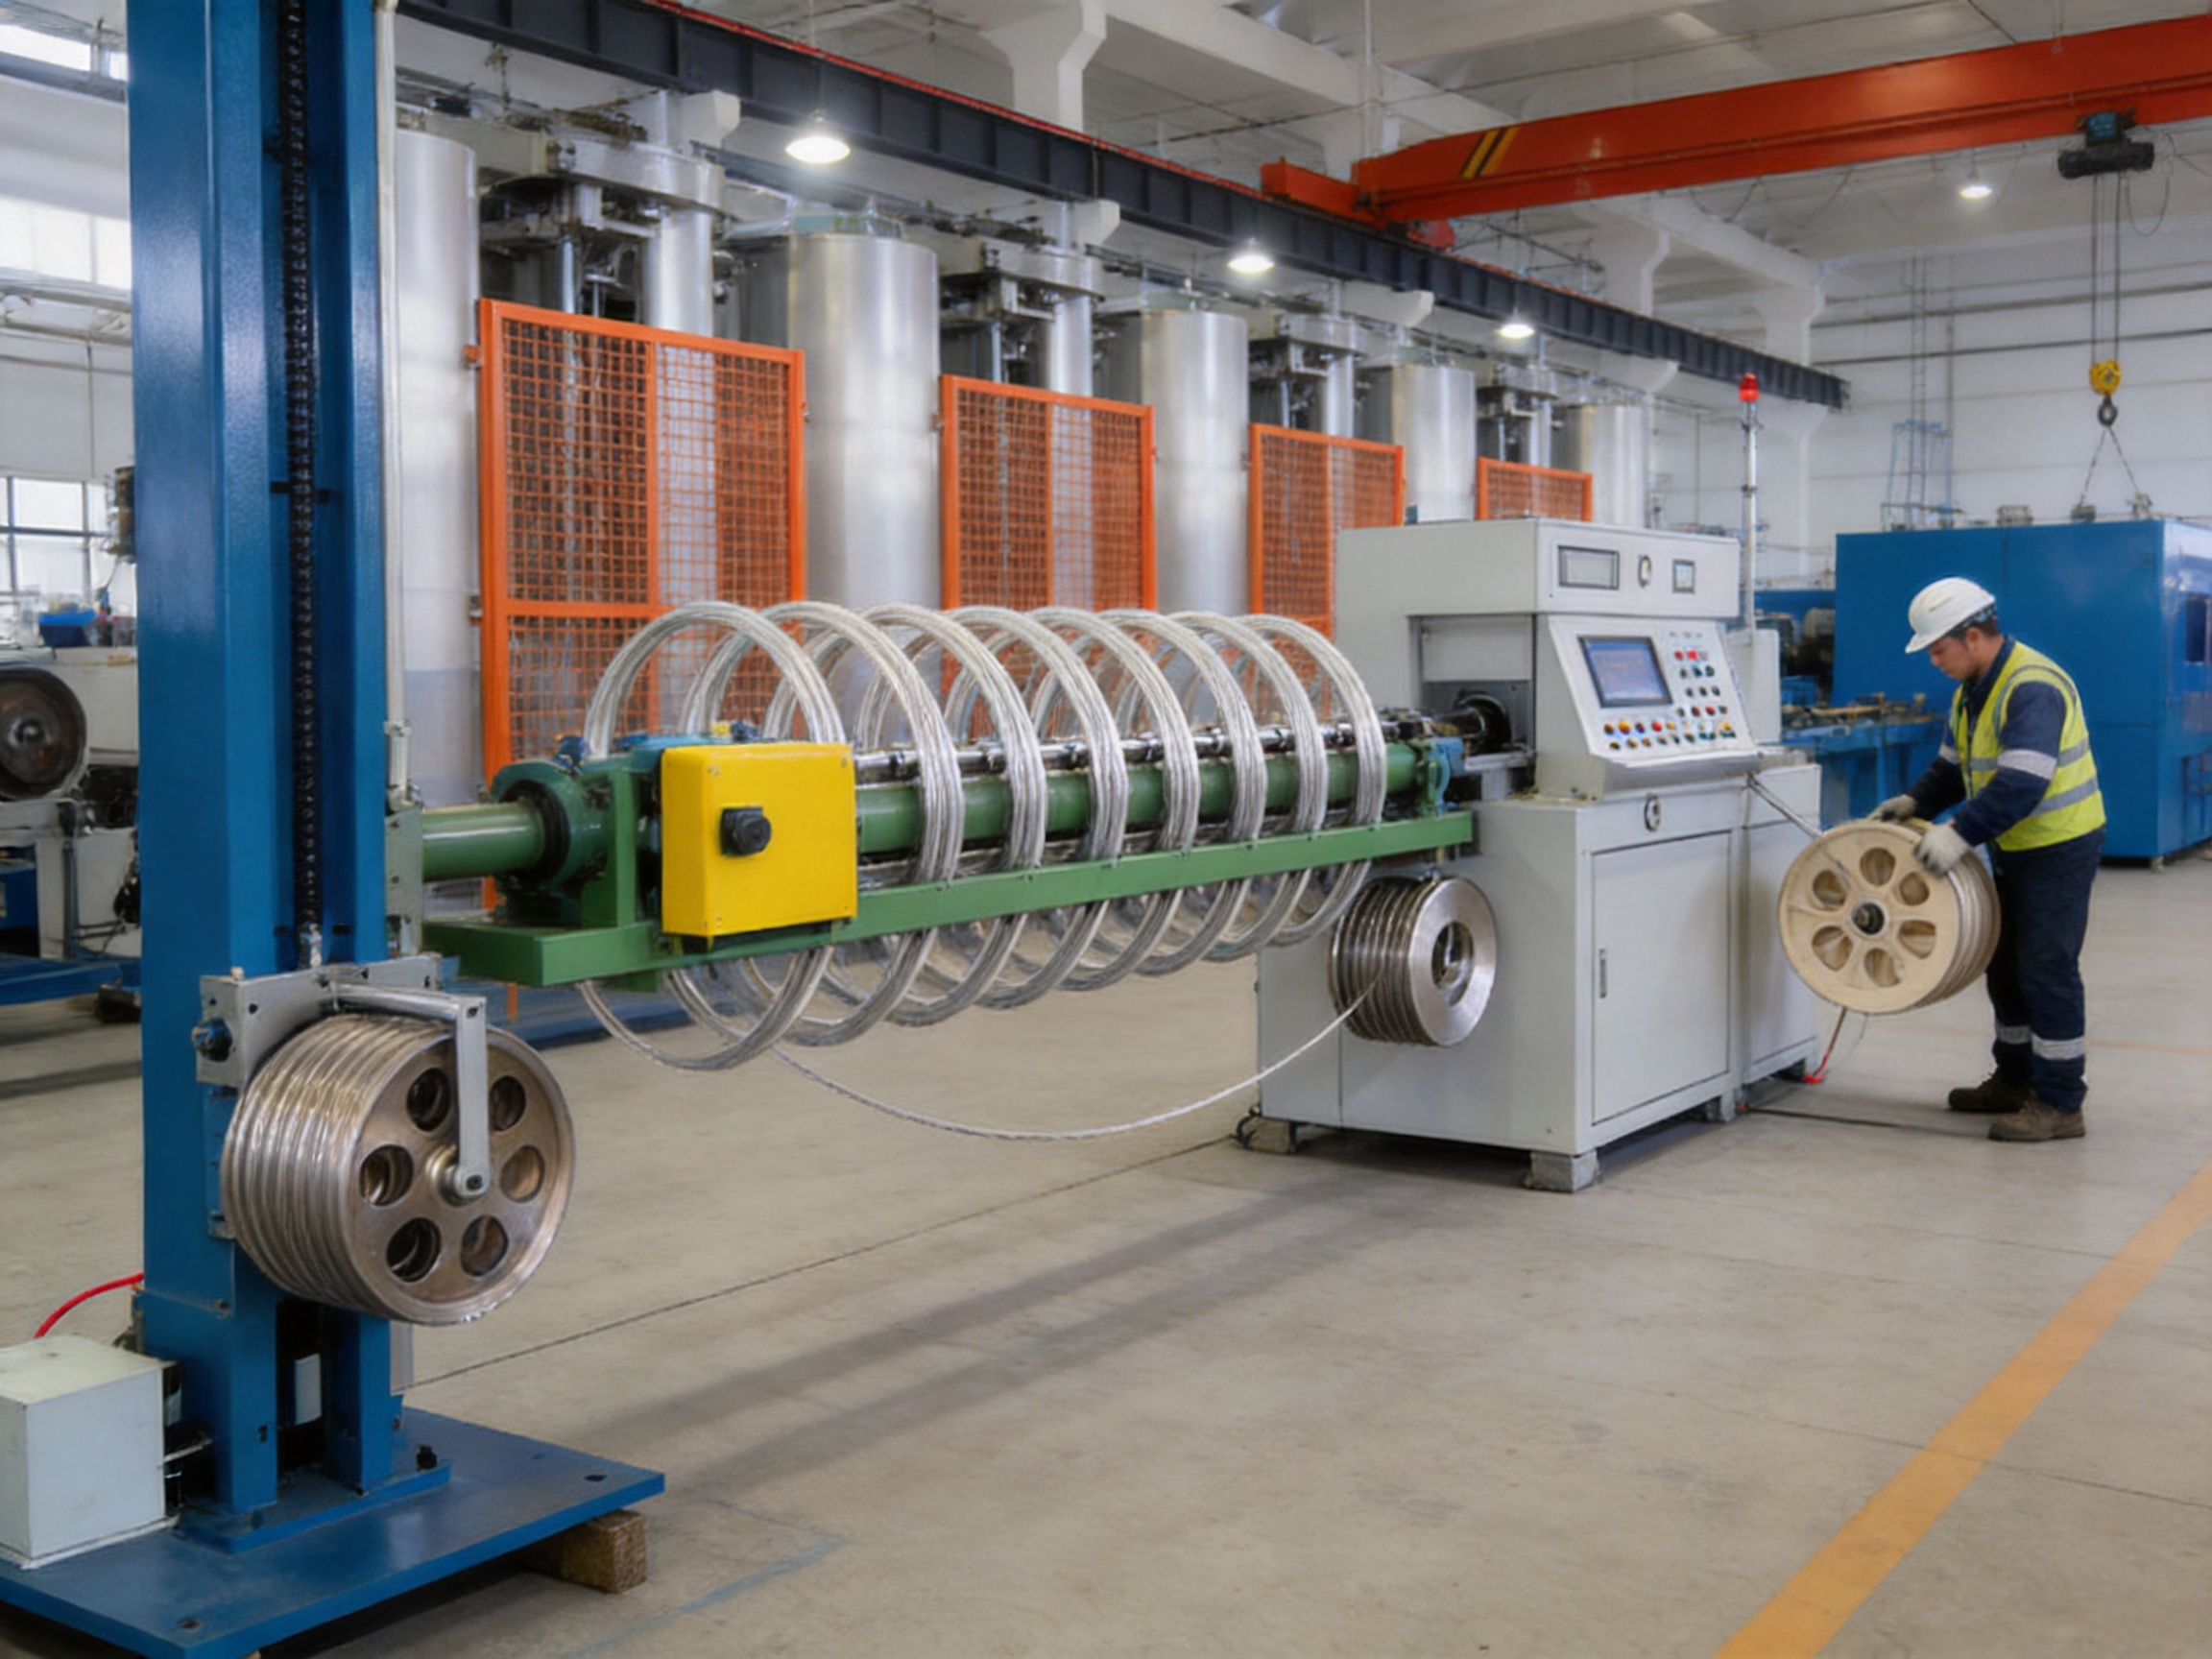
Technical Specifications and Model Selection
The listed accumulator models demonstrate how wheel diameter, wheel quantity, accumulation capacity, and cable diameter are related. The following table provides the available vertical model information supplied for this product range.
| Model | Wheel Diameter (mm) | Number of Wheels | Capacity (m) | Applicable Cable Diameter (mm) |
|---|---|---|---|---|
| AC-0330V | 300 | 10+11 | 41 | 2–6 |
| AC-0335V | 350 | 9+10 | 38 | 4–11 |
| AC-0340V | 400 | 7+8 | 30 | 6–12 |
| AC-0345V | 450 | 7+8 | 31 | 8–13 |
| AC-0350V | 500 | 6+7 | 24 | 10–15 |
| AC-0360V | 600 | 6+7 | 24 | 12–20 |
The AC-0330V model offers a stated capacity of 41 meters and is intended for cable diameters from 2 to 6 millimeters. Its 300-millimeter wheels and 10+11 wheel arrangement create a relatively long storage path for smaller cables.
The AC-0335V model uses 350-millimeter wheels and is designed for a cable diameter range of 4 to 11 millimeters. Its stated capacity is 38 meters, with 9+10 wheels in the storage arrangement.
The AC-0340V and AC-0345V models serve intermediate cable ranges. The AC-0340V model is specified for 6 to 12 millimeters, while the AC-0345V model is specified for 8 to 13 millimeters. These models use 400-millimeter and 450-millimeter wheels respectively.
The AC-0350V model is intended for cables from 10 to 15 millimeters, with 500-millimeter wheels and a stated capacity of 24 meters. The AC-0360V model supports a larger cable range of 12 to 20 millimeters and uses 600-millimeter wheels.
These specifications should be treated as a starting point for equipment selection. Actual suitability depends on cable construction, insulation material, minimum bending radius, operating speed, tension requirements, line elevation, and the required time for reel changeover. A technical review before ordering helps ensure that the selected unit matches the complete production system.
Advantages Compared with Basic Cable Storage Methods
More Controlled Than Floor Storage
A basic storage method may involve placing cable in loops on the floor or allowing it to hang between machine sections. Although this approach appears simple, it can create several operational problems. The cable may become tangled, contaminated, stepped on, or damaged by contact with vehicles and tools.
An accumulator dancer provides a dedicated path and a defined support structure. The cable remains elevated and organized, which improves both protection and operator visibility. This is a significant advantage in production environments where cleanliness and repeatability are important.
More Productive Than Manual Buffering
Manual buffering requires operators to handle and arrange the cable during production. This approach can be inconsistent and may expose personnel to unnecessary physical workload. It also makes the amount of available cable difficult to control.
A mechanical accumulator creates a repeatable storage method. Its wheel arrangement provides a known accumulation capacity, while the frame supports the cable in a stable position. This allows operators to focus on reel replacement and process control rather than manually forming and managing cable loops.
More Flexible Than a Fixed-Length Buffer
Some production lines use a simple fixed cable loop as a buffer. Such a loop may provide limited flexibility and may not accommodate different cable diameters or production speeds. It can also occupy more space than necessary.
The accumulator dancer offers a more structured solution. Different models provide different wheel diameters and capacities, and customized equipment can be developed for special requirements. This gives manufacturers more control over the relationship between cable size, storage length, and installation conditions.
Better Integrated with Production Lines
A standalone storage rack may support cable, but it may not be designed to coordinate with an extrusion, CV, or rewinding line. An accumulator dancer is intended to be installed as part of a cable processing system. Its purpose is not only to hold material but also to help manage the transition between payoff, processing, take-up, and reel changeover.
This integrated approach makes it easier to plan cable routing, machine positioning, and operating procedures. It also supports a more consistent line design when combined with other wire and cable machinery.
Reduced Risk of Unplanned Stops
Unplanned stops can affect output, labor utilization, material consumption, and process stability. When a reel is replaced without sufficient cable reserve, the line may stop suddenly. The result can include scrap, restarting adjustments, and additional inspection.
By providing a temporary cable reserve, the accumulator reduces dependence on immediate reel replacement. It gives the production team a controlled operating window and makes the changeover procedure more predictable.
Application in Extrusion Lines
Wire and cable extrusion lines often require coordinated movement between conductor payoff, extrusion, cooling, diameter control, capstan, and take-up equipment. Even when each machine is operating correctly, reel replacement can interrupt the entire sequence.
An accumulator installed at an appropriate point in the line can maintain cable movement while the payoff reel is changed. It can also help manage the relationship between the extrusion process and the take-up section. The cable remains supported as it passes through the storage path, helping protect the freshly processed surface from unnecessary contact.
When used after extrusion, the accumulator must be selected with attention to the condition of the cable surface. The guiding wheels should be suitable for the cable material and finish, and the cable route should avoid excessive pressure or bending. The production team should also consider cooling conditions, surface moisture, and the cable’s mechanical strength at the installation point.
For extrusion lines producing several cable sizes, a flexible equipment plan is essential. The accumulator range includes models for different cable diameter groups, and customized capacity can help adapt the equipment to the plant’s product mix.
Application in CV Lines
CV cable production involves specialized continuous processing conditions, and stable cable movement is important for maintaining product consistency. A cable storage rack can be used to accumulate or control cable during reel changeover within a suitable line arrangement.
The selection process for a CV application should consider the cable’s dimensions, weight, insulation condition, minimum bending requirements, and the operating speed of the surrounding equipment. The accumulator should be positioned so that it supports the production sequence without interfering with cooling, curing, inspection, or other essential process stages.
A vertical or horizontal configuration can be selected according to the layout of the CV line. A vertical unit may be useful where floor space is limited, while a horizontal unit may be preferred where overhead clearance is restricted. In both cases, the cable path should be planned carefully to maintain smooth entry and exit conditions.
Application in Rewinding and Take-Up Lines
Rewinding operations often involve transferring cable from one reel to another. During this process, the line may need to continue moving while the operator handles the full or empty reel. An accumulator provides an intermediate reserve that can reduce the need for an immediate stop.
In take-up applications, the cable storage rack can help manage the difference between the continuous production speed and the intermittent reel-handling activity. This is valuable when reels must be removed, positioned, secured, or replaced in a limited operating window.
The equipment can also support a more organized working area around the take-up section. By guiding the cable through a designated path, it reduces the possibility of uncontrolled loops and helps operators understand the direction of cable travel.
Manufacturing and Engineering Strengths
Application-Oriented Machine Design
The production of an effective accumulator begins with understanding the customer’s process rather than simply fabricating a frame with wheels. The equipment must correspond to the cable diameter, required storage length, operating speed, available space, and reel-change method.
Shanghai Yessjet Precise Machinery Co., Ltd. focuses on wire and cable machinery and provides equipment for cable production line applications. Its product scope includes wire and cable extrusion lines, fully automatic coiling and packaging equipment, intelligent robot stackers, coiling machines, motorized payoff equipment, motorized take-up equipment, accessory equipment, and cable extrusion machines.
This broader product range is an advantage when a customer requires more than an isolated accessory. The accumulator can be considered in relation to the complete line, including payoff, extrusion, take-up, coiling, rewinding, and packaging operations. Such coordination helps reduce compatibility issues that may occur when individual machines are selected without considering the whole production process.
Customization Capability
The accumulation capacity of the cable storage rack can be made according to customer requirements. This is a practical strength because production lines differ in speed, cable diameter, changeover duration, and floor plan.
Customization may be considered for vertical or horizontal installation, storage length, wheel arrangement, cable range, frame dimensions, and connection with neighboring machines. The purpose of customization is not simply to alter the appearance of the equipment. It is to ensure that the accumulator provides the required buffer time while maintaining a suitable cable route.
Structured Production Process
Advanced manufacturing is reflected in the way a machine is designed, fabricated, assembled, inspected, and prepared for installation. For cable machinery, a structured process is important because the equipment must maintain alignment, reliable cable guidance, stable support, and repeatable operation.
A professional manufacturing workflow generally includes application review, design confirmation, component preparation, frame fabrication, wheel and guide installation, assembly, functional inspection, and final delivery preparation. Each step contributes to the final reliability of the accumulator.
Accurate frame construction helps the wheel groups remain properly positioned. Careful assembly helps reduce unwanted cable deviation. Appropriate surface treatment and finishing support long-term use in industrial conditions. Inspection of moving and guiding components helps identify issues before the machine reaches the customer’s production floor.
Experience in Complete Cable Machinery
A supplier experienced in several categories of wire and cable machinery can evaluate the accumulator as part of a larger production sequence. This is important because an accessory that works well in one line may require different dimensions or controls in another.
Knowledge of extrusion, payoff, take-up, coiling, and packaging helps the manufacturer understand how cable tension, speed, reel handling, and product protection interact. The result is a more practical equipment recommendation and a better basis for customization.
Production Efficiency as a Design Priority
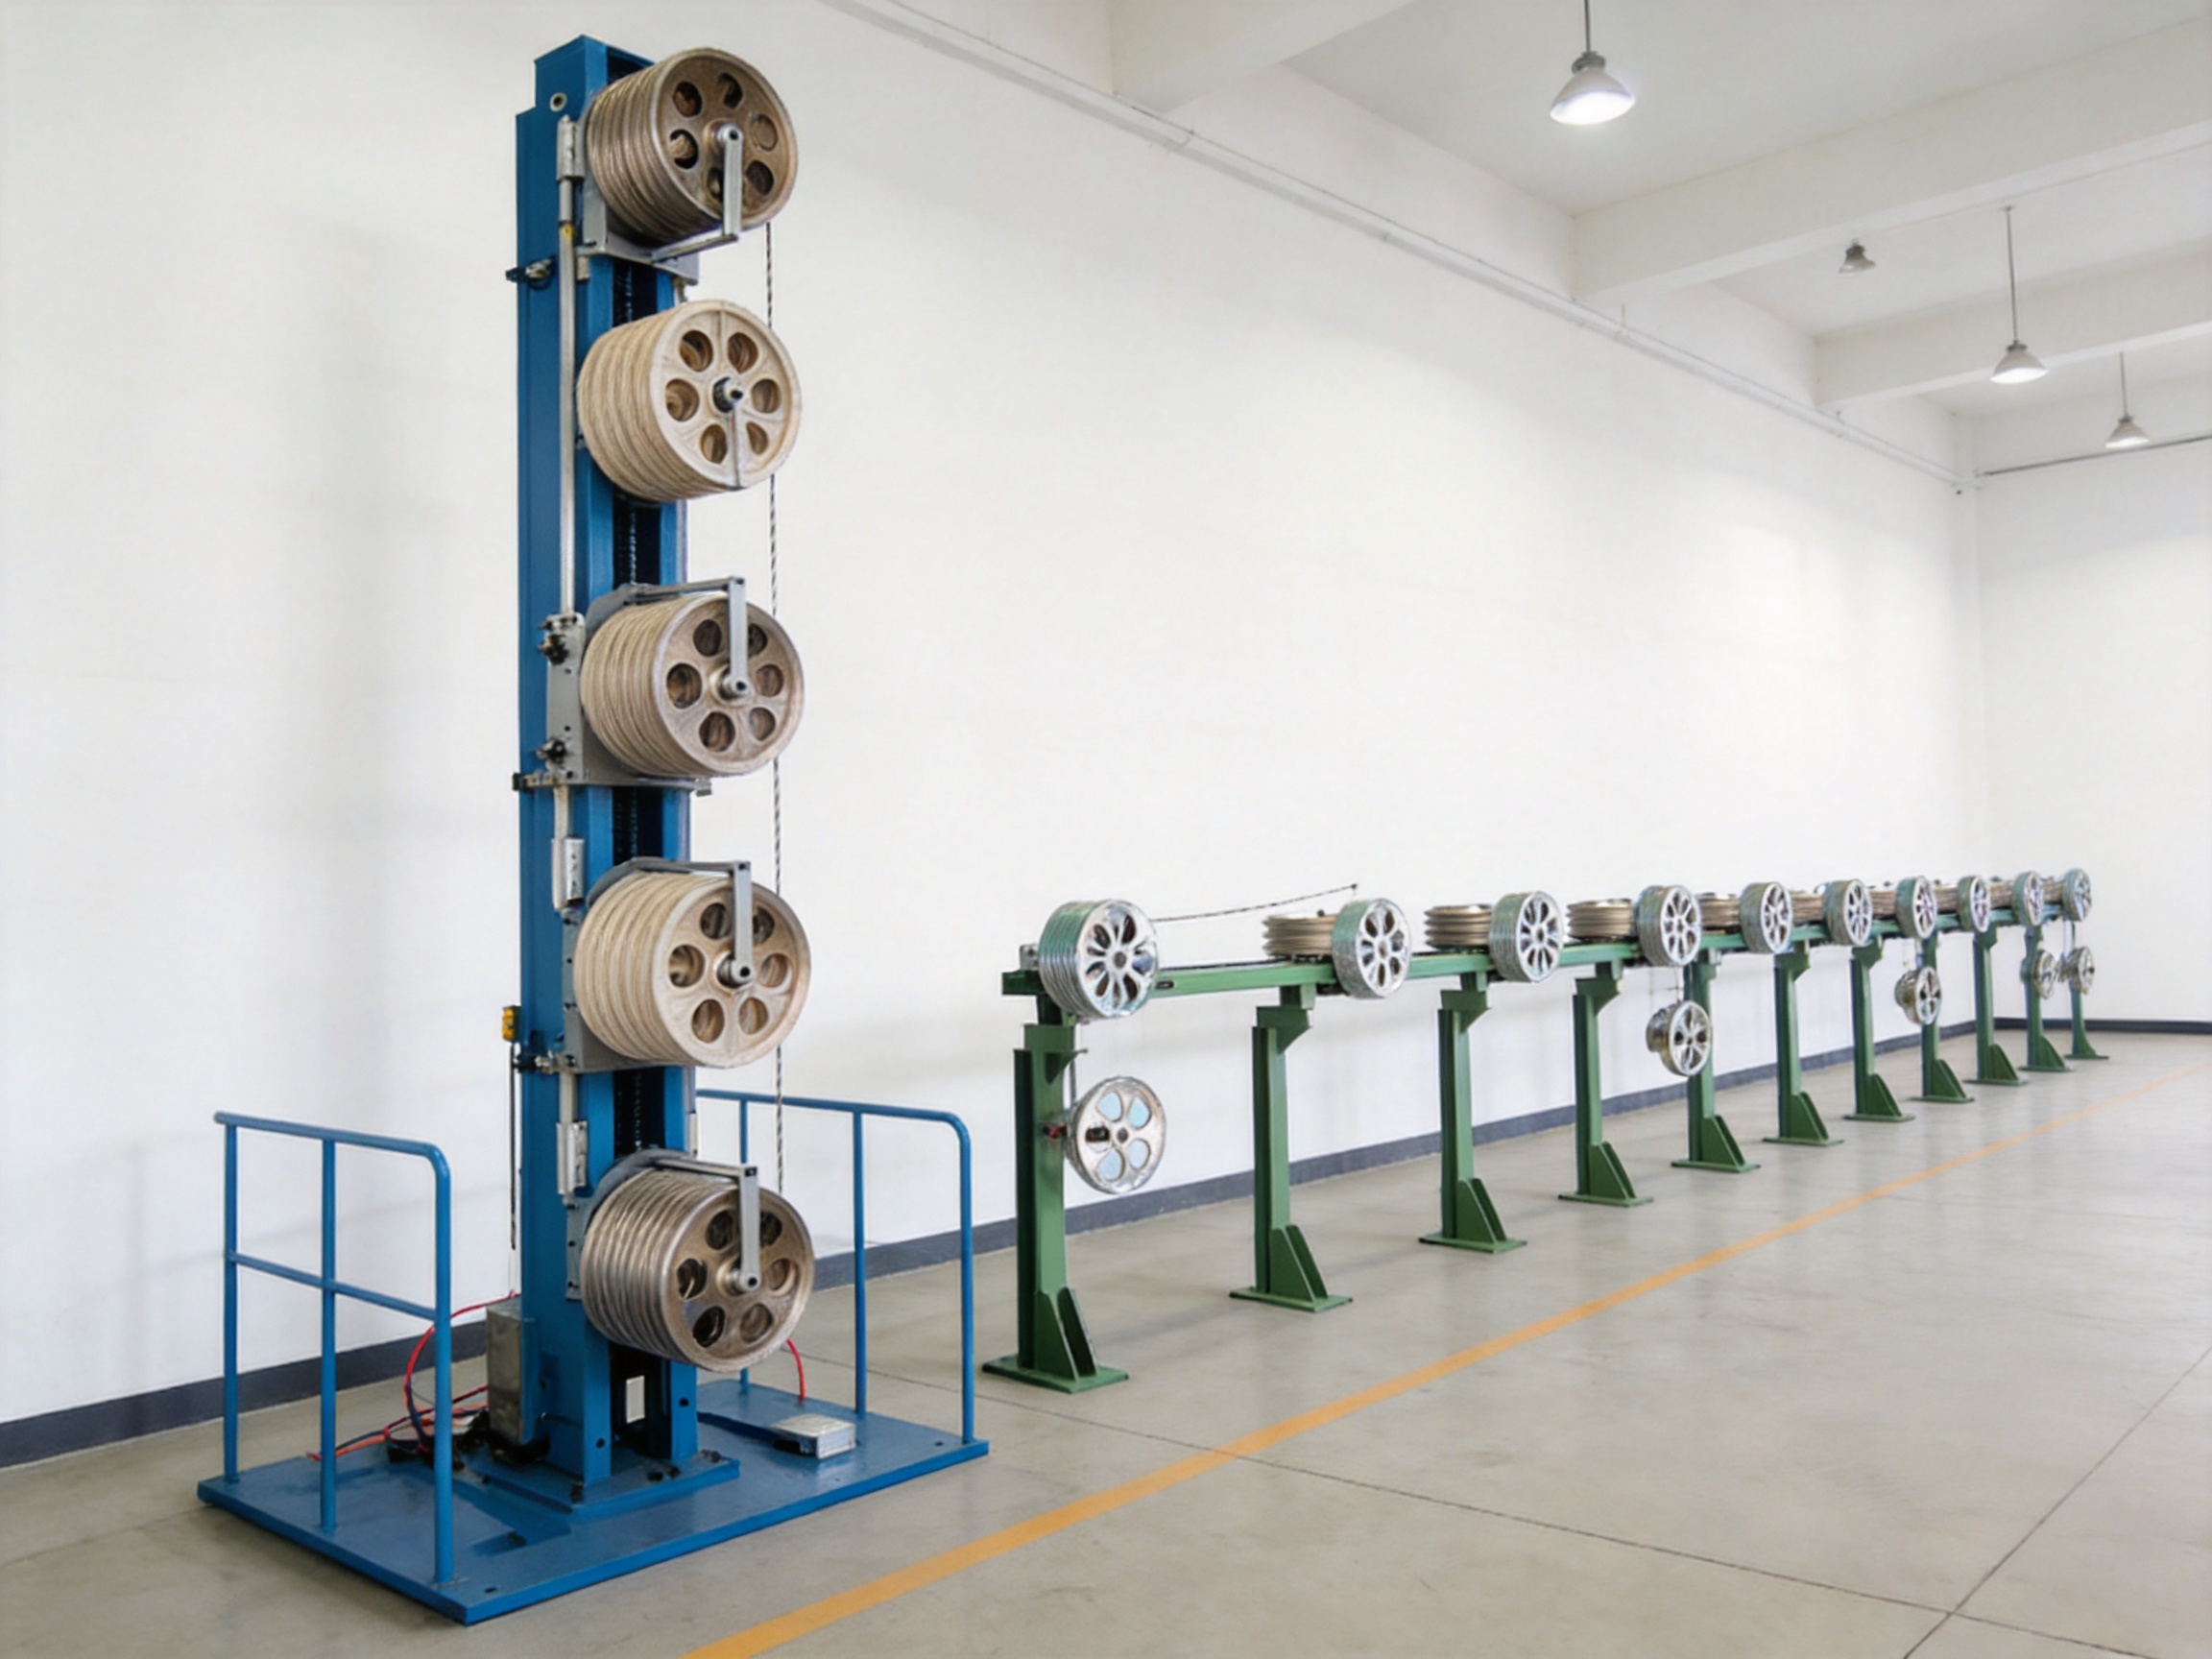
The accumulator is designed around a clear production goal: keeping cable processing stable during reel changeover. Its value is therefore measured not only by its physical construction but also by its effect on line utilization and operator efficiency.
Reducing unnecessary stops can improve effective production time. Organizing the cable route can simplify operation. Protecting the cable can reduce avoidable damage. Supporting maintenance can help operators identify issues more quickly. These benefits work together to improve the overall performance of a cable production line.
How the Accumulator Improves Operational Efficiency
Faster Reel Replacement
Reel replacement can be a repetitive but time-sensitive task. Operators must remove the old reel, position the new reel, secure it, connect the cable, and verify that the line is ready to continue. Without a buffer, each step may be performed under pressure because production must stop immediately.
The accumulator creates additional operating time. Operators can complete the replacement in a more controlled sequence, reducing the likelihood of hurried connections or incorrect cable routing.
Lower Material Waste
Production stops and restarts can result in cable that does not meet the required specification. Depending on the process, the line may need time to return to stable speed, temperature, tension, or dimensional control. A controlled cable buffer can reduce the frequency of these interruptions.
Lower waste is particularly valuable when the cable includes costly conductor materials, specialized insulation, or strict quality requirements. The exact reduction depends on the line and operating method, but preventing avoidable stops is an important way to improve material utilization.
Improved Operator Convenience
A cable storage rack reduces the need for manual cable handling. The cable follows a defined route, and the frame provides a visible reference for operation and maintenance. This can make daily work more predictable and reduce unnecessary physical effort.
Good equipment design should support operators rather than require them to compensate for poor cable routing. The accumulator contributes to a cleaner, more organized production environment and can simplify training for new personnel.
More Consistent Cable Movement
Irregular cable movement can affect both product protection and line stability. A dedicated storage path helps maintain a more consistent direction of travel. When properly matched to the cable and operating conditions, the wheel arrangement reduces uncontrolled loops and sudden changes in cable position.
Consistent movement is especially important when the cable passes through several connected machines. Each machine can perform more effectively when the incoming cable follows a predictable route.
Installation Planning
Before installing an accumulator dancer, the production team should review the complete line layout. Important points include the distance between neighboring machines, cable entry and exit elevations, available floor or ceiling space, operator access, maintenance clearance, and the direction of cable travel.
The selected location should allow the cable to enter and leave the accumulator smoothly. Sharp changes in direction should be avoided unless they are part of a carefully engineered route. The equipment should be placed where operators can safely observe the cable and perform reel-change procedures.
For a vertical model, building height and overhead obstructions must be checked. For a horizontal model, the available floor length and access around the machine must be evaluated. The base and supporting structure should be installed on a suitable foundation capable of maintaining the equipment’s position during operation.
Connection with upstream and downstream equipment should be verified before commissioning. The cable should not be forced sideways into the first wheel or pulled at an unsuitable angle from the final wheel. A smooth transition helps protect the cable and reduces unnecessary mechanical stress.
Operation and Maintenance Recommendations
Routine Inspection
Operators should regularly inspect the wheel surfaces, supports, frame, fasteners, and cable route. Any unusual noise, vibration, resistance, or cable deviation should be investigated before continued operation.
Inspection is particularly important after a product changeover. A larger or stiffer cable may require a different operating arrangement, and the cable path should be checked before the line is restarted at full speed.
Wheel and Guide Condition
The wheels or rollers are the main contact points between the machine and the cable. They should remain clean, smooth, and correctly aligned. Damage or contamination on a wheel can affect cable movement and may leave marks on the cable surface.
Where the machine is used with sensitive insulation or finished outer sheaths, operators should pay close attention to any sign of scoring, abrasion, flattening, or unusual wear. If such signs appear, the line should be stopped safely and the cause identified.
Frame and Fastener Checks
The accumulator frame must remain stable during operation. Fasteners, mounting points, and structural connections should be checked according to the plant’s maintenance schedule. Any looseness can affect alignment and create additional cable movement.
Keeping the area around the machine clean also improves inspection quality. Dirt, scrap cable, packaging material, and tools should not be allowed to accumulate around the moving path.
Safe Reel-Change Procedures
Reel replacement should follow a documented operating procedure. The procedure should identify when the cable reserve is being used, how the new reel is connected, and how normal cable supply is restored. Operators should be trained to work around moving cable and rotating reels safely.
The accumulator is designed to support the changeover process, but it does not replace the need for proper guarding, emergency-stop systems, lockout procedures, and plant safety rules. These measures should be determined according to the complete production line and applicable workplace requirements.
Selection Guide for Cable Manufacturers
The first selection factor is cable diameter. The listed models cover several diameter ranges, from smaller cables supported by the AC-0330V to larger cables supported by the AC-0360V. The cable’s actual construction and flexibility should also be considered, not only its nominal outside diameter.
The second factor is required accumulation capacity. The plant should estimate how much cable is needed during a normal reel changeover. This calculation should include the line speed, the time required to remove and install the reel, the time required to connect the cable, and a reasonable operating margin.
The third factor is available installation space. A vertical unit may be suitable for a narrow floor plan with adequate height. A horizontal unit may be more appropriate for a low-ceiling building with sufficient floor length. The equipment position should allow safe access for operation and maintenance.
The fourth factor is the production line application. An accumulator for an extrusion line may have different requirements from one used in a rewinding or take-up line. Cable temperature, surface condition, tension, line speed, and process position should all be reviewed.
The fifth factor is future production development. If the manufacturer expects to introduce larger cable sizes, increase line speed, or expand the product range, it may be practical to discuss a customized accumulator capacity rather than selecting only for current conditions.
Why Choose a Specialized Manufacturer?
A specialized wire and cable machinery manufacturer can provide more than a standard mechanical assembly. It can evaluate the accumulator according to the behavior of the cable, the sequence of the line, and the customer’s production objectives.
Shanghai Yessjet Precise Machinery Co., Ltd. is positioned as a China-based manufacturer and supplier of wire and cable machinery, including vertical wire accumulators and horizontal cable storage racks. Its experience across cable production equipment supports a system-oriented approach to product development.
Customers can benefit from discussing the accumulator together with their existing or planned extrusion, payoff, take-up, coiling, and packaging equipment. This approach helps determine whether the unit should be installed before or after a particular process, how much storage is needed, and which configuration best fits the plant.
The company’s product portfolio also supports turnkey cable production line planning. When several machines are sourced from a manufacturer familiar with the complete process, it may be easier to coordinate machine interfaces, cable routes, operating sequences, and production objectives.
A specialized supplier can also provide technical communication during the early planning stage. Information such as cable diameter, line speed, reel size, cable material, required changeover time, and available installation space allows the equipment to be configured more accurately.
Typical Customer Benefits
For a cable manufacturer, the purchase of an accumulator dancer can provide several practical benefits. The first is greater continuity during reel changeover. The second is better control of the cable path. The third is improved protection against abrasion and uncontrolled contact. The fourth is easier maintenance and inspection.
These benefits support broader production objectives. More continuous operation can improve equipment utilization. Better cable protection can support finished-product quality. A cleaner work area can improve operator efficiency. A customizable design can help the equipment remain useful as production requirements change.
The value of the machine should therefore be considered over its operating life rather than only by its initial purchase price. A low-cost storage method may appear economical but create hidden costs through downtime, cable damage, manual handling, and inconsistent changeover procedures. A purpose-built accumulator is designed to address these operating costs directly.
Q&A: Accumulator Dancer Cable Storage Rack
What is the main purpose of an accumulator dancer?
Its main purpose is to temporarily store and control cable in a wire or cable production line. It supports cable movement during reel changeover and helps prevent the need to stop the entire line whenever a payoff or take-up reel is replaced.
Where can the cable storage rack be installed?
It can be installed in extrusion lines, CV lines, rewind lines, and other cable processing systems. The exact position depends on whether the equipment is required to support payoff control, take-up control, or cable accumulation between two processing stages.
What is the difference between vertical and horizontal types?
A vertical accumulator uses an upright structure and is often selected when floor space is limited but building height is available. A horizontal accumulator uses a longer, lower structure and is useful where floor length is available but overhead clearance is restricted.
Can the accumulation capacity be customized?
Yes. The accumulation capacity can be made according to customer requirements. The design may be adapted to the required storage length, cable diameter, line speed, reel-change time, wheel arrangement, and available installation space.
How should the model be selected?
Model selection should consider cable diameter, cable construction, required capacity, wheel diameter, line speed, bending requirements, and plant layout. The listed models provide a starting point, but a technical review is recommended for a final selection.
What cable diameter range is covered by the listed models?
The supplied vertical models cover cable diameter ranges from 2–6 millimeters for the AC-0330V through 12–20 millimeters for the AC-0360V. Intermediate models cover several overlapping ranges, allowing selection according to the cable product.
How does the accumulator protect cable?
It guides the cable through a dedicated wheel path and supports it away from the floor and other possible hazards. This reduces uncontrolled dragging, contact, looping, and abrasion. The wheel diameter and surface condition should be appropriate for the cable being processed.
Can it be used with both payoff and take-up equipment?
Yes. The accumulator can be used to accumulate or control cable payoff or take-up during reel changeover. Its exact function depends on its location in the line and the operating sequence of the surrounding equipment.
Does the accumulator replace all production controls?
No. It is a mechanical cable storage and control device that supports the production line. It should be used together with appropriate line controls, guarding, emergency-stop systems, operator training, and safe reel-change procedures.
Why work with a manufacturer of complete cable machinery?
A manufacturer with experience in extrusion, payoff, take-up, coiling, rewinding, packaging, and accessory equipment can evaluate the accumulator as part of the complete line. This can improve compatibility and support a more coordinated equipment solution.
What information should be provided when requesting a quotation?
Useful information includes cable diameter, cable construction, line speed, required accumulation length, reel dimensions, reel-change time, cable entry and exit height, available floor or ceiling space, production line type, and whether a vertical or horizontal layout is preferred.
Conclusion
The accumulator dancer cable storage rack is a practical solution for improving continuity, cable protection, and operating control in wire and cable production. By creating a temporary cable reserve, it helps manufacturers manage reel changeover without unnecessary disruption to extrusion, CV, rewinding, payoff, or take-up operations.
Its advantages include organized cable support, reduced wear risk, improved operator convenience, better production continuity, and compatibility with different line arrangements. The availability of vertical and horizontal types allows the equipment to be matched to the factory layout, while customizable accumulation capacity supports different cable sizes, production speeds, and changeover procedures.
The listed AC-0330V through AC-0360V models provide several combinations of wheel diameter, wheel quantity, capacity, and applicable cable diameter. These options give cable manufacturers a practical basis for equipment selection, while customized engineering can address more specific production requirements.
As a wire and cable machinery manufacturer, Shanghai Yessjet Precise Machinery Co., Ltd. combines accumulator design with broader knowledge of extrusion lines, payoff systems, take-up systems, coiling machines, packaging equipment, and other cable production machinery. This system-oriented capability supports customers that need an accessory integrated into an existing line or require a coordinated turnkey production solution.
For manufacturers seeking to reduce reel-change downtime, organize cable handling, and protect product quality, a professionally engineered accumulator dancer is an important investment in stable and efficient production.
References
1. Product technical information for accumulator dancer and cable storage rack equipment, including vertical model specifications.
2. General principles of wire and cable extrusion line design and continuous cable handling.
3. Industrial guidelines for cable bending radius, controlled material routing, and reel changeover procedures.
4. Manufacturing practices for wire and cable machinery, including equipment integration, mechanical assembly, and production-line planning.
5. Technical product information covering wire accumulators, vertical cable storage racks, horizontal cable storage racks, payoff equipment, take-up equipment, coiling equipment, and cable extrusion machinery.