LANGUAGE
 中文简体
 русский
 Français
 Español
 Português
 عربى
Content
- 1 Why Tension Control Matters in Cable Production
- 2 Core Function of Wire Cable Tension Control Systems
- 3 Preventing Excessive Cable Tension
- 4 Preventing Insufficient Cable Tension
- 5 Integration with Storage Racks and Cable Handling Equipment
- 6 Advantages Compared with Basic or Uncontrolled Winding Methods
- 7 Product Quality Benefits
- 8 Efficiency, Yield, and Cost Control
- 9 Application Areas
- 10 Manufacturing and Engineering Strengths
- 11 Advantages of a Complete Machinery Supplier
- 12 Quality-Oriented Manufacturing Process
- 13 Operational Benefits for Cable Manufacturers
- 14 Selection Considerations
- 15 Installation and Commissioning Approach
- 16 Maintenance and Long-Term Performance
- 17 Role in Intelligent and Automated Production
- 18 Why Choose a Practical, Application-Focused Solution
- 19 Frequently Asked Questions
- 19.1 What is the main purpose of a Wire Cable Tension Control System?
- 19.2 Can the system be used with a storage rack?
- 19.3 What problems can uncontrolled tension cause?
- 19.4 Is the system suitable for existing cable production lines?
- 19.5 Can it be used with motorized pay-off and take-up equipment?
- 19.6 Does tension control improve cable quality?
- 19.7 Can the equipment support different cable specifications?
- 19.8 How does tension control reduce production waste?
- 19.9 Is the system useful for automatic coiling and packaging?
- 19.10 What should be considered before placing an order?
- 19.11 What manufacturing strengths are important when choosing a supplier?
- 19.12 What routine maintenance is required?
- 20 Conclusion
- 21 References
- 22 Product: Wire Cable Tension Control Systems
Wire and cable manufacturing depends on a series of connected processes in which small variations can create significant quality problems. Conductor preparation, insulation extrusion, cooling, take-up, winding, coiling, packaging, and storage must work together as one coordinated production system. Among these operations, cable tension control is particularly important because the cable is continuously pulled, guided, wound, or accumulated while the production line is running. If the tension is too high, the cable may become stretched, deformed, compressed, or damaged. If the tension is too low, the cable can become loose, overlap irregularly, or form disordered coils.
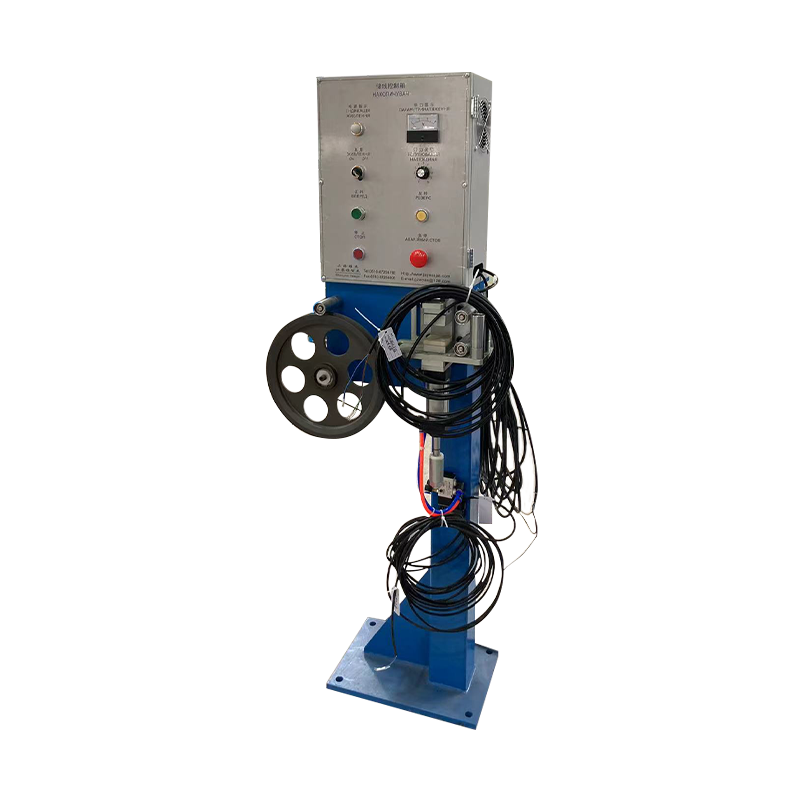
Wire Cable Tension Control Systems are designed to manage this challenge through real-time tension regulation. The equipment helps maintain a stable and appropriate pulling force as cable conditions change during winding and handling. By keeping tension within a controlled range, the system supports uniform winding, reduces material waste, improves the appearance of finished coils, and contributes to consistent production output.
As an accessory equipment solution, the system can be integrated with cable storage racks, coiling machines, take-up equipment, extrusion lines, and other wire and cable production machinery. This flexibility allows manufacturers to add reliable tension management to existing lines without necessarily redesigning the entire plant. For new projects, it can also be included as part of a complete cable production turnkey solution.
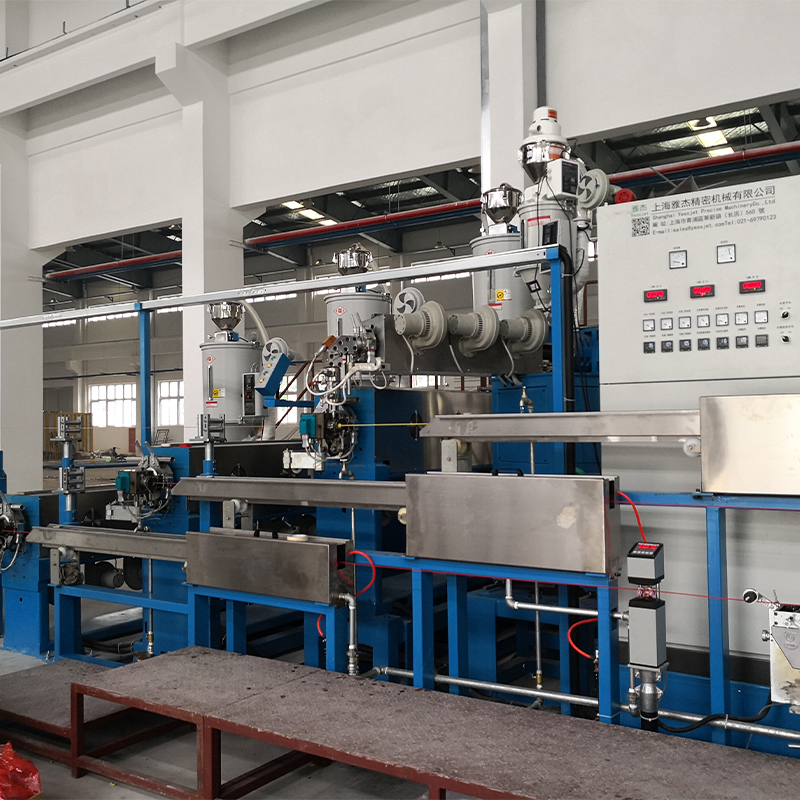
Shanghai Yessjet Precise Machinery Co., Ltd. develops and supplies equipment for wire and cable production, including extrusion lines, coiling and packaging equipment, intelligent robot stackers, motorized pay-off and take-up machines, coiling machines, and accessory systems. Its focus on coordinated machinery, process compatibility, and practical automation provides a strong foundation for supplying tension control equipment to different cable manufacturing environments.
Wire Cable Tension Control Systems
Why Tension Control Matters in Cable Production
Cable winding is not simply a matter of rotating a reel or collecting a length of finished product. The cable must travel through several points of contact while maintaining a controlled path. It may pass over guides, through a storage rack, around a traction mechanism, into a coiler, or onto a take-up reel. Every change in speed, direction, diameter, or material condition can influence the tension applied to the cable.
For a cable producer, stable tension has a direct relationship with product quality. A cable that is wound too tightly may show compression marks, flattened sections, excessive bending stress, or dimensional changes. In some cases, excessive tension can affect insulation, shielding layers, conductors, or the overall geometry of the cable. The problem may not become visible until the cable is unwound or installed by the customer.
Insufficient tension creates a different set of risks. Loose winding can lead to gaps between layers, crossed cable sections, uneven coil edges, unstable reels, and disordered accumulation. During later transportation or processing, loosely wound cable can shift, tangle, or require manual correction. These issues increase labor requirements and may reduce the amount of saleable product obtained from each production batch.
Manual tension adjustment is often inadequate for modern production lines. An operator may adjust a brake, clutch, or mechanical setting at the start of a run, but cable speed and material conditions can change during operation. Reel diameter decreases as material is paid off, while the effective winding diameter increases as cable is taken up. A fixed setting therefore cannot always deliver the same tension throughout the entire process.
A dedicated tension control system addresses this limitation by supporting continuous adjustment. The system is intended to respond to changes in operating conditions and keep the cable under a more stable pulling force. This creates a controlled transition between upstream and downstream equipment, reducing the chance that one machine will pull too strongly or allow the cable to become slack.
Core Function of Wire Cable Tension Control Systems
The central function of the Wire Cable Tension Control Systems is the adjustment of cable tension during winding and related handling operations. The equipment works as part of a larger material flow, helping to balance the movement of cable between storage, processing, and coiling equipment.
In a typical application, cable travels from an upstream process toward a storage rack, take-up unit, or coiling machine. The tension control system monitors or regulates the force applied to the cable so that the downstream machine can collect the material without creating excessive pull. At the same time, it prevents the cable from becoming so loose that it loses its correct path or forms an unstable winding pattern.
The system is especially useful where cable speed changes, where reel diameter varies, or where the cable must pass through different pieces of machinery. It can help create a smoother relationship between motorized pay-off equipment and motorized take-up equipment. When incorporated into a complete line, it also supports more stable coordination between extrusion, cooling, traction, storage, coiling, and packaging operations.
The equipment is not intended to replace every other control system in a production line. Instead, it provides a dedicated function that complements the main machines. This focused design makes it suitable for manufacturers that need to improve winding stability without adding unnecessary complexity or adopting exaggerated features that do not contribute to their actual production needs.
Preventing Excessive Cable Tension
Excessive tension is one of the most common causes of cable handling defects. When a cable is pulled with too much force, the conductor or insulation may be subjected to mechanical stress beyond the intended processing condition. Even if the cable remains visually intact, excessive tension may influence its dimensional stability, flexibility, or internal arrangement.
During winding, excessive tension can also cause a coil to become harder and more compact than required. This may make subsequent unwinding difficult and can increase the risk of deformation when the cable is stored for a long time. For products with sensitive insulation, fine conductors, shielding layers, or special outer jackets, controlled tension is particularly important.
The Wire Cable Tension Control Systems help reduce these risks by regulating the pulling force instead of allowing the cable to be driven only by uncontrolled machine speed or mechanical resistance. With better tension balance, the cable can be collected at an appropriate density while retaining its intended shape and performance characteristics.
Consistent tension also helps protect the interface between the cable and the machine. Excessive pulling force may cause unnecessary wear on guide rollers, winding components, and contact surfaces. By reducing sudden force variations, the system can contribute to smoother operation and more predictable maintenance requirements.
Preventing Insufficient Cable Tension
Too little tension can be just as damaging to winding quality as too much tension. When the cable is not held firmly enough, it may move away from its intended path. It can form loops, overlap previous layers, or collect unevenly at the edge of a reel. These defects are often difficult to correct after the winding process has been completed.
Loose winding can also reduce the effective capacity of a reel or coil. A reel that should contain a planned length of cable may reach its physical limit prematurely because the material is not arranged efficiently. In addition, loose sections may shift during transportation, causing the finished package to lose its shape.
A controlled tension system provides a more stable connection between cable movement and winding speed. It helps the cable remain properly positioned as it enters the coiling or take-up process. This is valuable for both short coils and long-length reels, especially when the production line operates continuously and manual intervention would interrupt output.
By preventing slack conditions, the system can reduce the need for operators to stop the line and rearrange cable manually. It therefore supports safer and more efficient production. Operators can focus on monitoring the process, checking product quality, and managing normal material changes rather than repeatedly correcting winding defects.
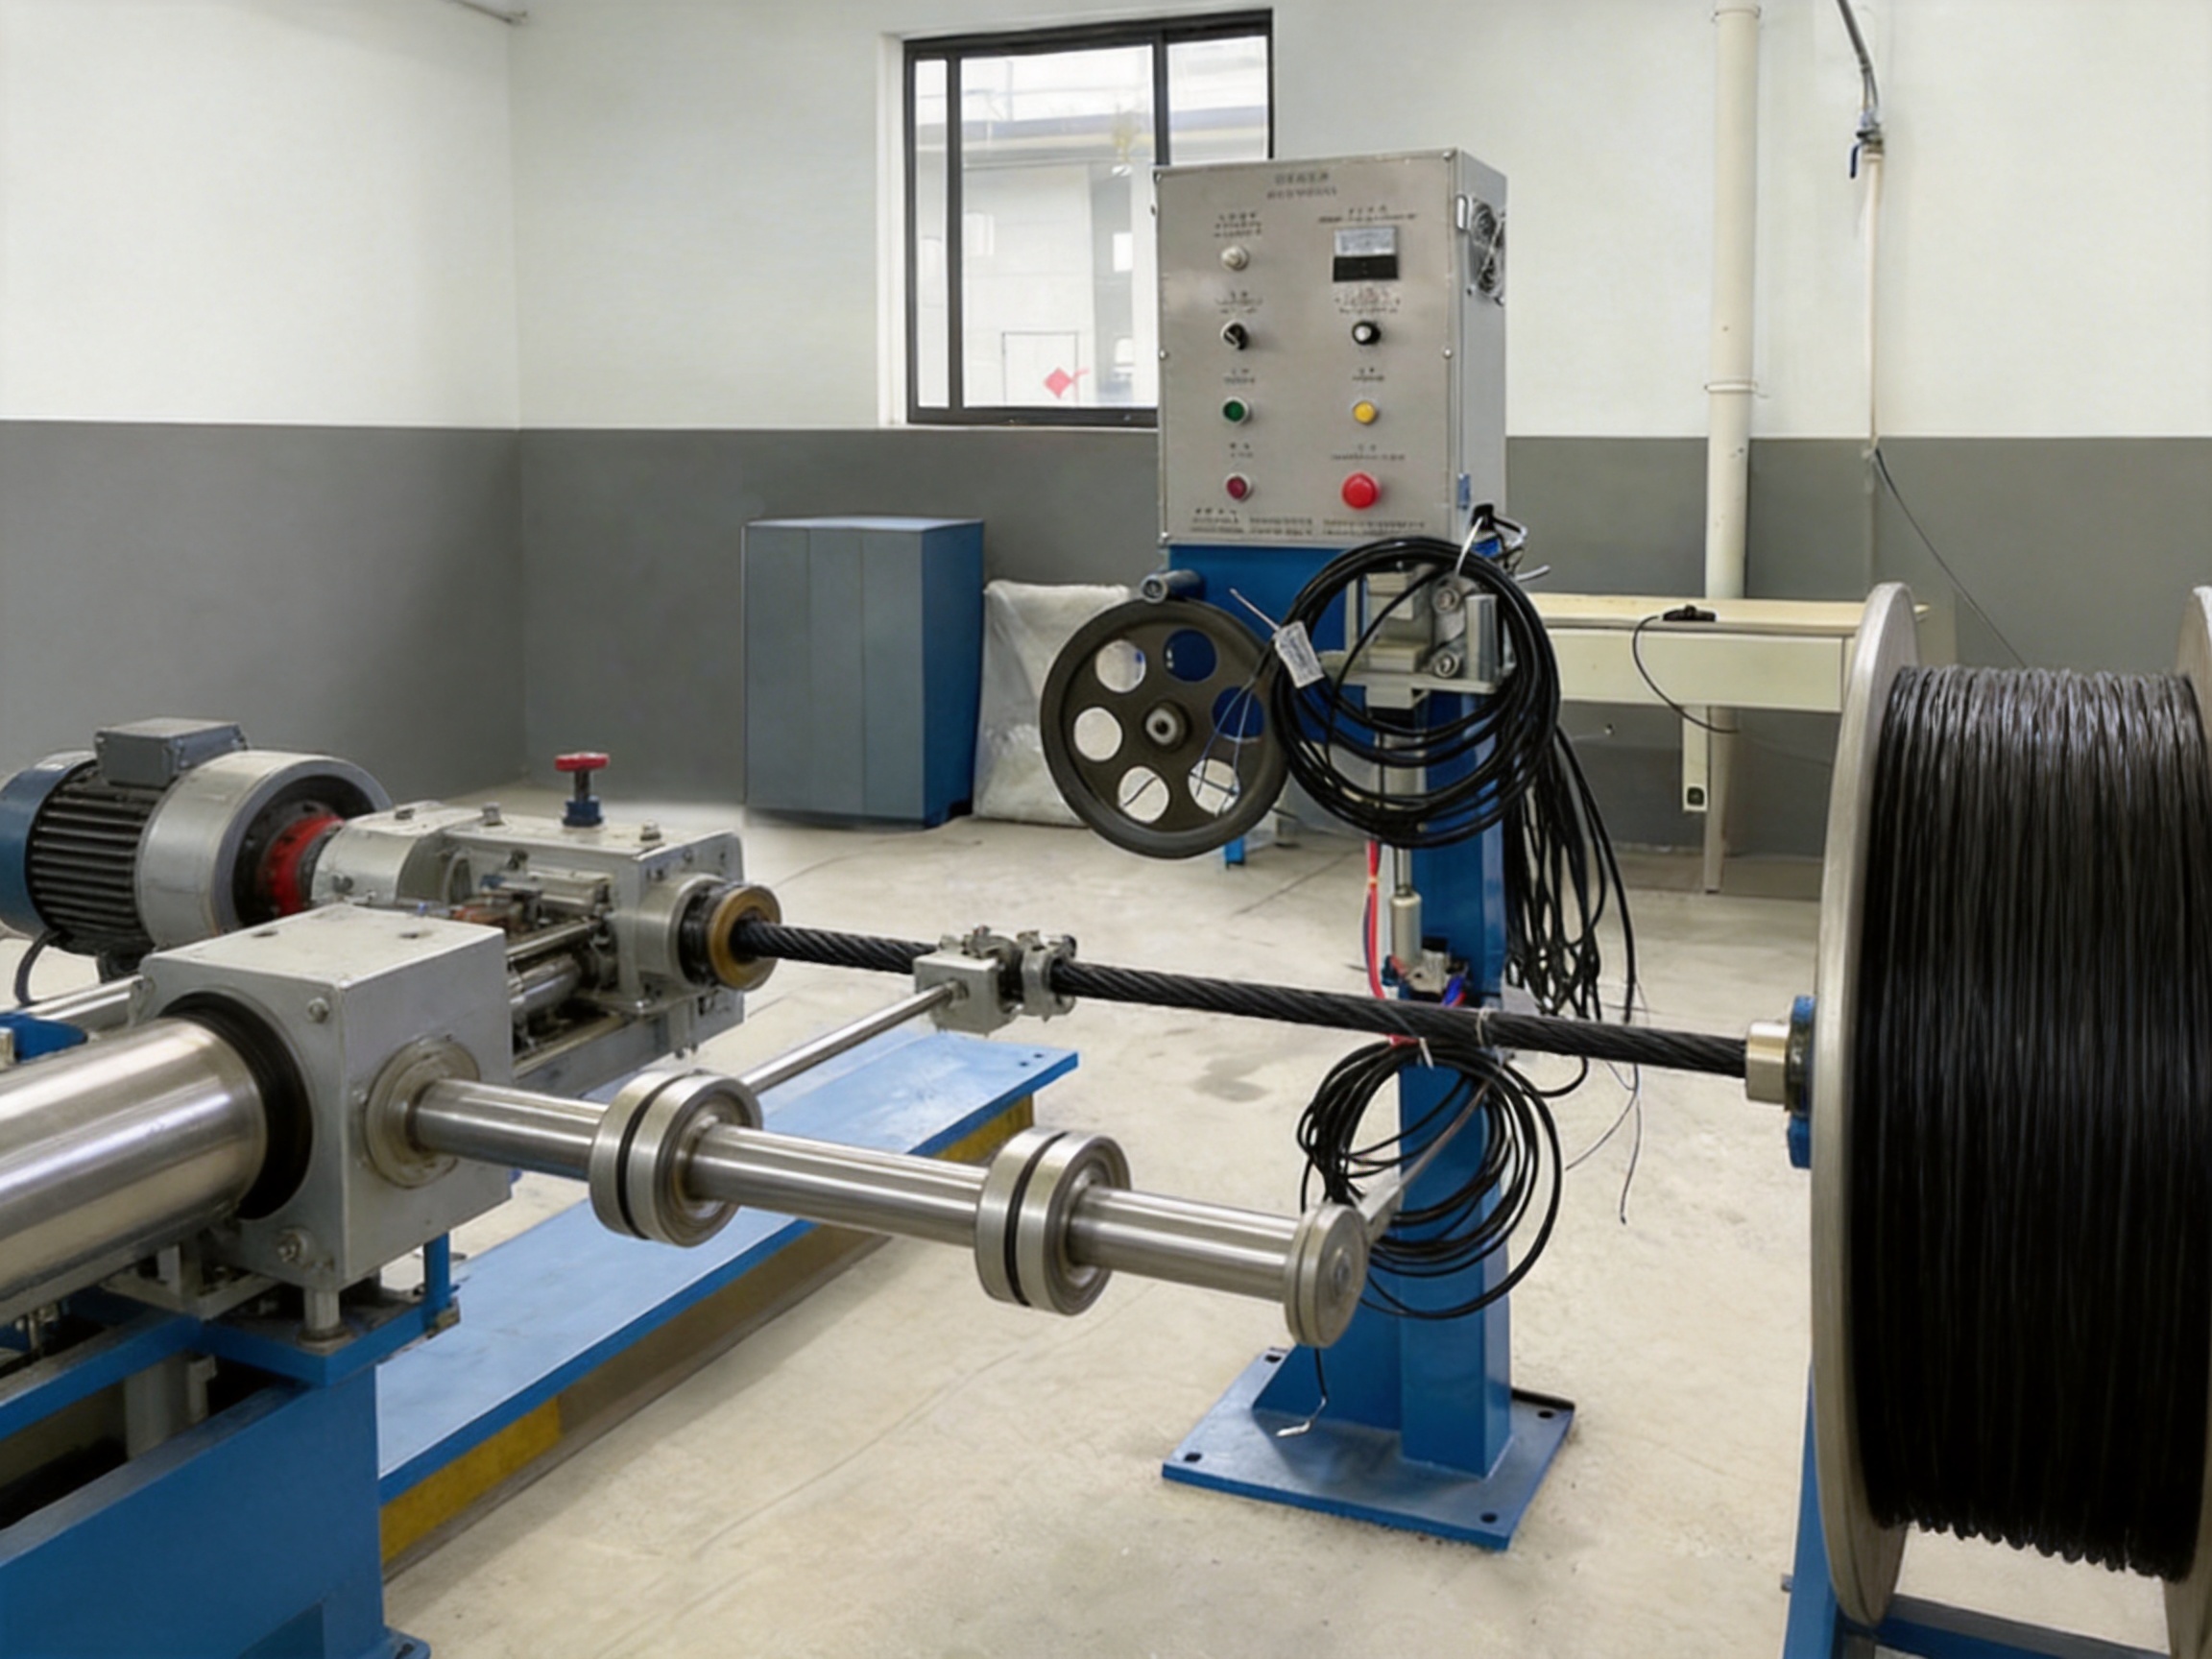
Integration with Storage Racks and Cable Handling Equipment
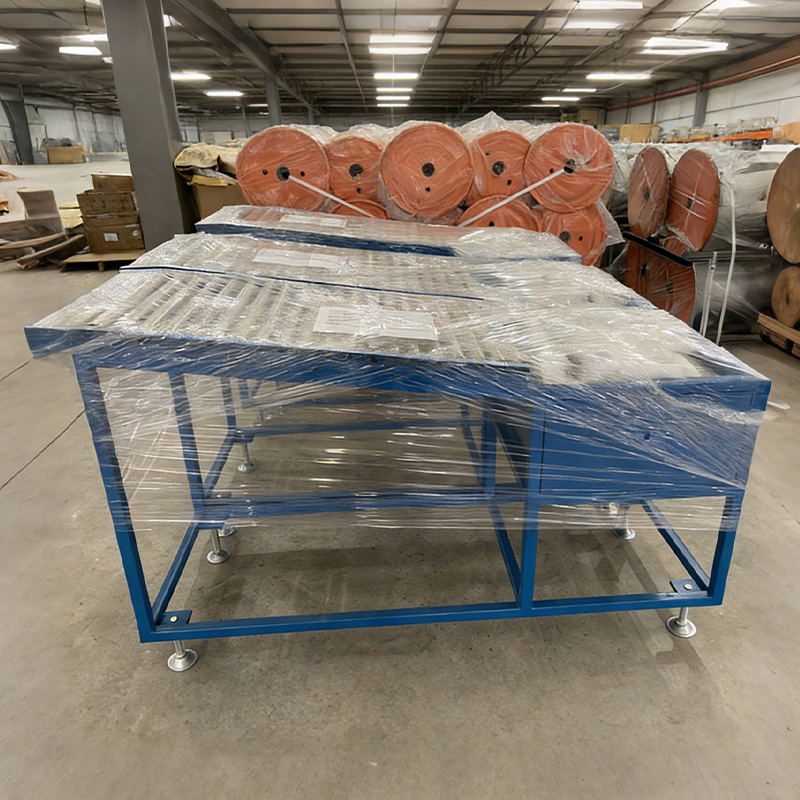
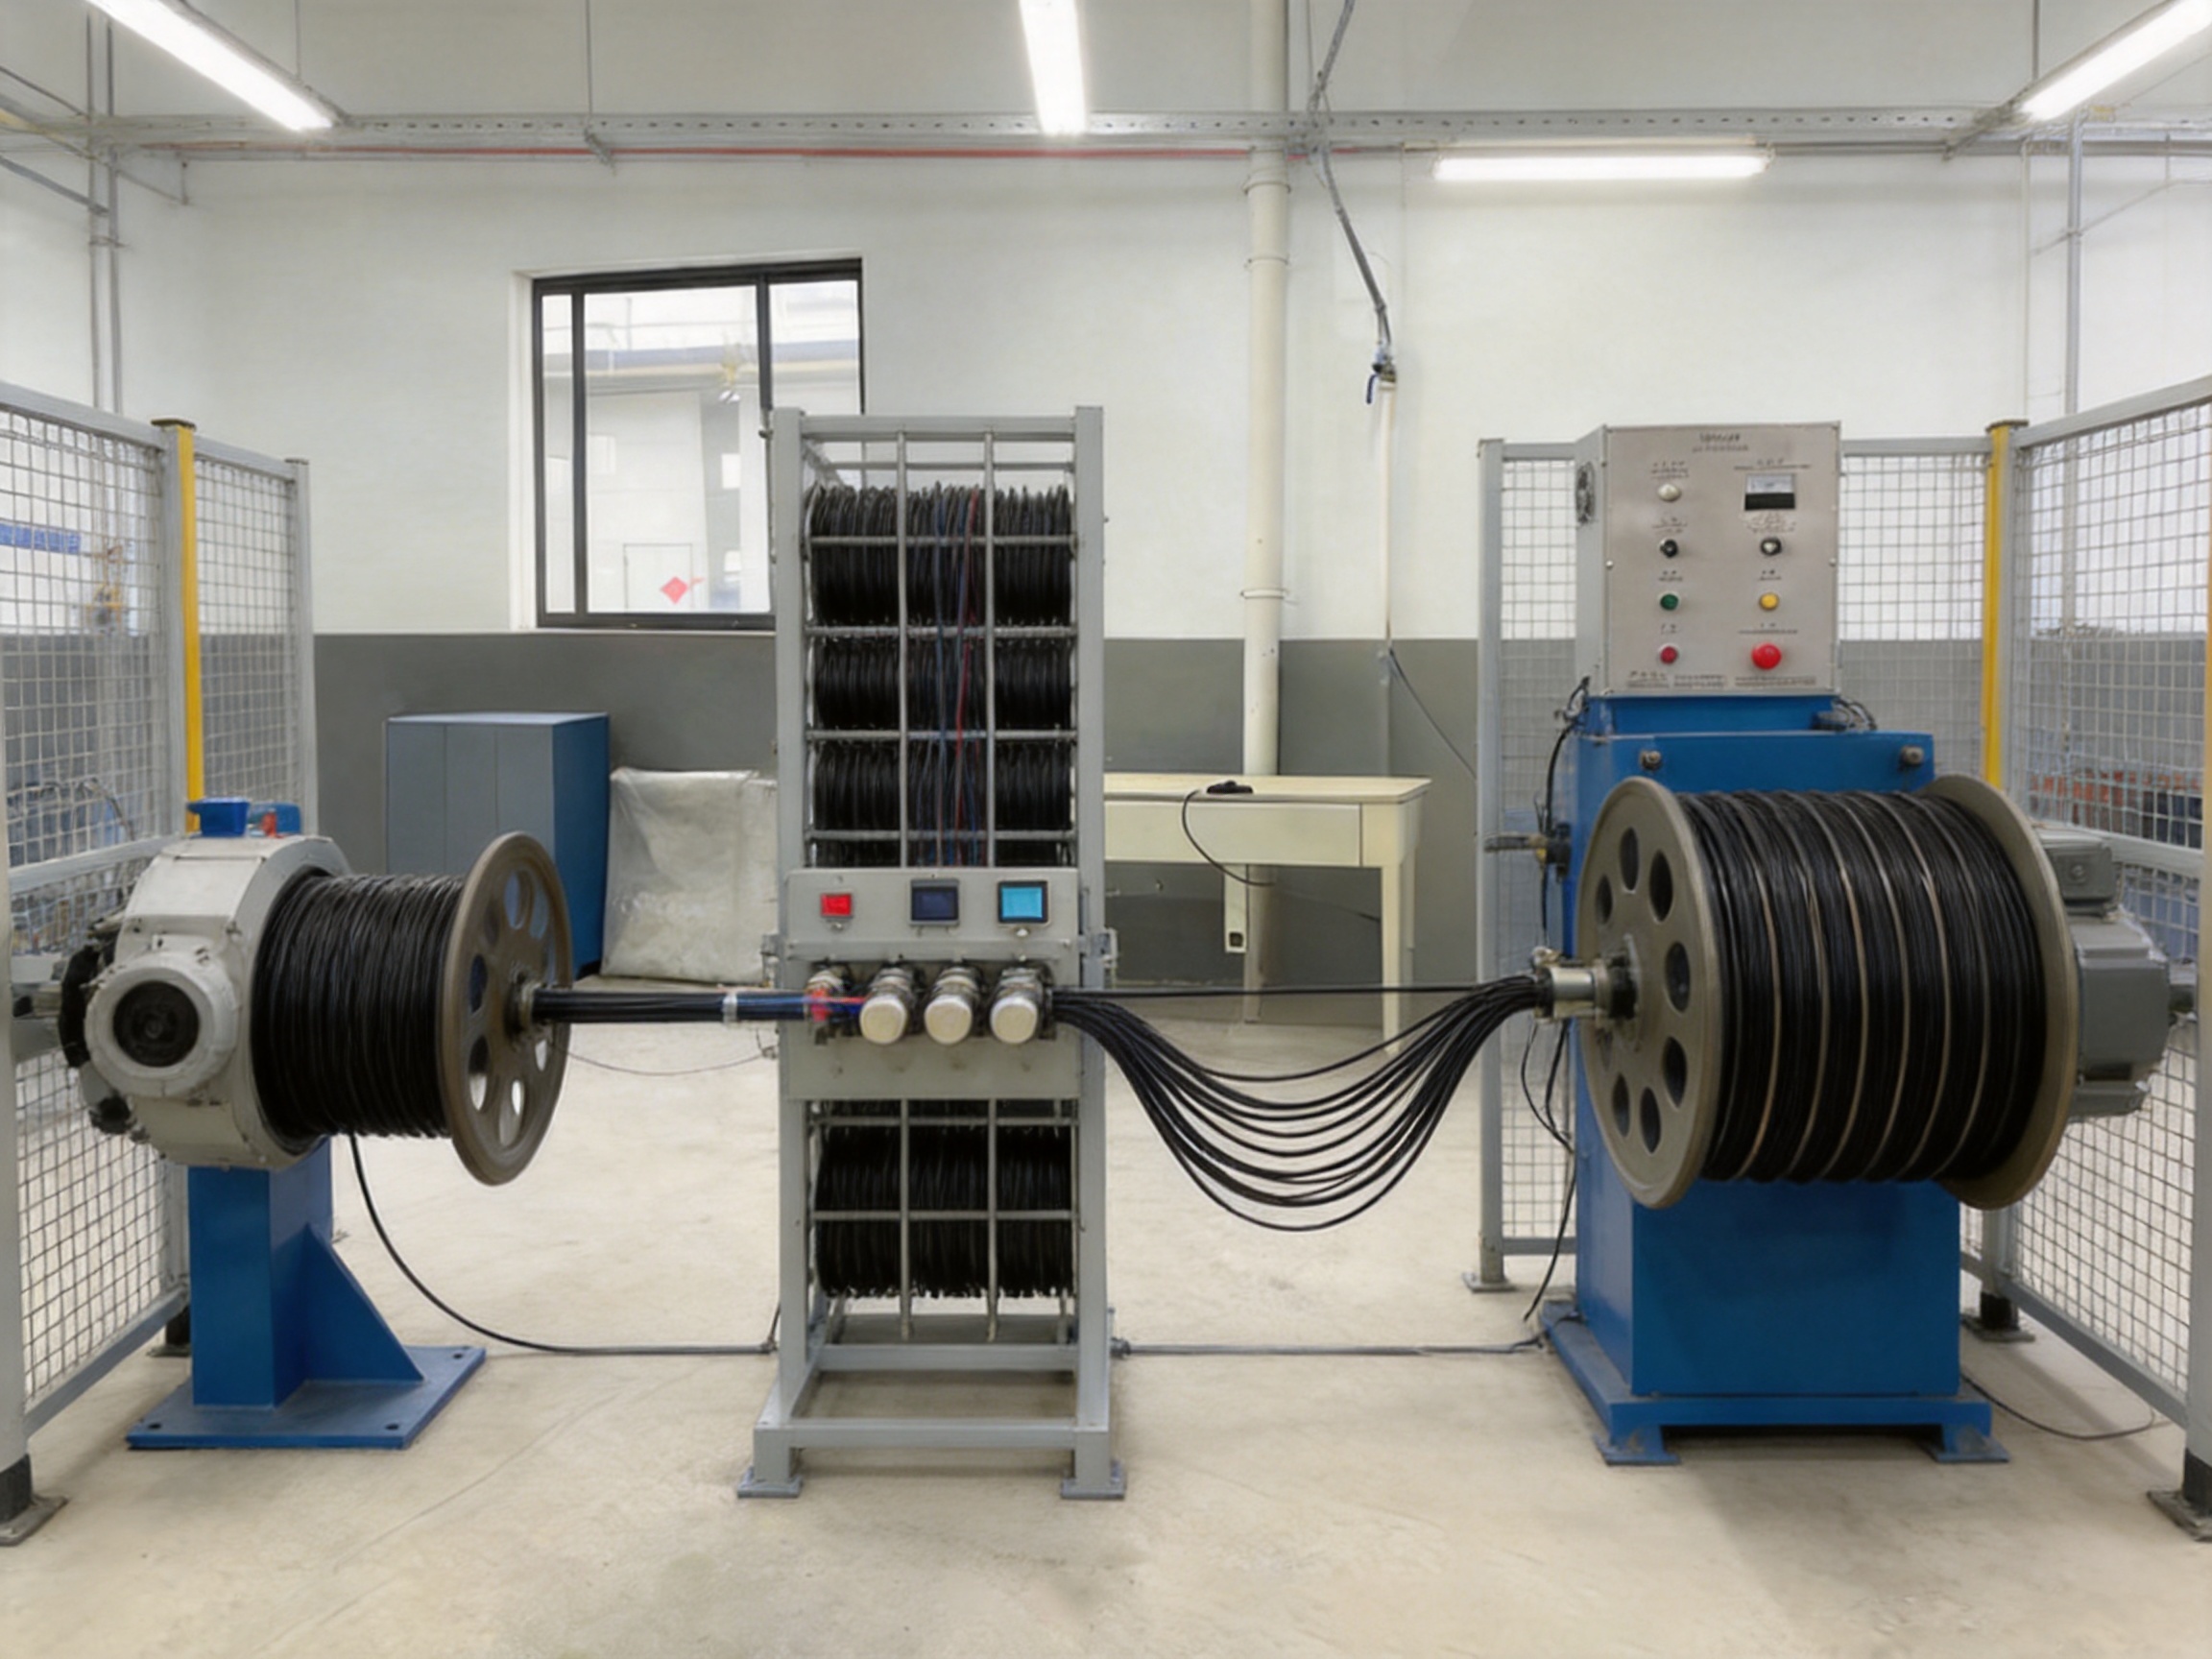
Wire Cable Tension Control Systems are often used together with storage racks. A storage rack can provide a controlled buffer between different stages of production, allowing upstream and downstream machines to operate with greater independence. However, the storage area must be managed carefully. If the cable enters or leaves the rack under unstable tension, the material may accumulate unevenly or become tangled.
When the tension control system is integrated with a storage rack, the cable can be guided through the buffer with a more consistent force. This helps preserve the order of the stored material and allows the line to absorb normal changes in speed. The result is a smoother material flow between extrusion, cooling, inspection, take-up, and coiling operations.
The system can also be paired with motorized pay-off equipment. A pay-off machine must release cable at a suitable rate without creating excessive resistance. If the pay-off is too slow, the downstream equipment may pull the cable too strongly. If it releases too quickly, slack may develop. Tension control helps balance these two conditions.
On the take-up side, the system supports consistent collection as the reel fills. The changing reel diameter can affect the relationship between motor speed and linear cable speed. Tension regulation helps compensate for these changes so the cable is not wound too tightly at one stage and too loosely at another.
For coiling machines, stable tension is essential to forming neat, repeatable coils. A coiler may need to guide cable into a circular or layered pattern. If tension fluctuates during this process, the coil edge may become uneven or the cable may cross over itself. A tension control system helps provide the stable material condition required for orderly coiling.
Advantages Compared with Basic or Uncontrolled Winding Methods
Some production lines rely on fixed mechanical brakes, manual adjustments, or simple speed matching. These methods may be sufficient for limited applications, but they can become unreliable when cable types, line speeds, reel sizes, or production volumes change. Wire Cable Tension Control Systems offer several practical advantages over these basic approaches.
| Production concern | Basic or uncontrolled method | Controlled tension approach | Practical result |
|---|---|---|---|
| Changing reel diameter | Requires repeated manual adjustment | Supports ongoing tension regulation | More uniform winding conditions |
| Speed variation | May create slack or sudden pulling force | Helps balance cable movement and machine speed | Fewer winding interruptions |
| Operator workload | Frequent visual correction and intervention | More stable automated handling | Improved labor efficiency |
| Coil appearance | Uneven layers or loose sections may occur | Supports orderly arrangement | More consistent finished packages |
| Material yield | Higher risk of damage and rework | Reduced tension-related defects | Lower waste and improved production yield |
| Line integration | Separate machines may operate independently | Can be paired with racks, pay-offs, and take-ups | Better overall workflow coordination |
The most important advantage is process consistency. A tension control system does not merely add another machine to the line; it helps stabilize the relationship between machines. This is valuable because production defects often occur at the transition between equipment rather than inside one machine alone.
Another advantage is adaptability. Cable products differ in diameter, construction, flexibility, surface material, and allowable mechanical stress. A practical tension control solution should support adjustment for different production conditions. This makes it more useful than a fixed setting designed for only one cable specification.
The system also offers an advantage in production management. When tension-related problems are reduced, quality personnel can spend less time dealing with irregular coils and more time verifying planned product standards. Maintenance teams can benefit from smoother machine loading, while production managers gain a more stable basis for planning output and material consumption.
Product Quality Benefits
The immediate quality benefit of tension control is improved winding order. A properly controlled cable can be arranged in regular layers or coils with fewer overlaps and fewer loose sections. This improves the visual appearance of the package and makes the product easier to inspect, transport, store, and unwind.
Stable tension also helps preserve cable geometry. The system is designed to avoid the excessive pulling force that can stretch or compress the cable during winding. This is important when the finished cable must maintain a particular diameter, flexibility, bending radius, or surface condition.
Another benefit is reduced risk of hidden mechanical stress. A cable may pass a basic visual inspection even when it has experienced excessive tension. By controlling the process before the defect occurs, manufacturers can reduce the possibility of quality concerns appearing later during installation or use.
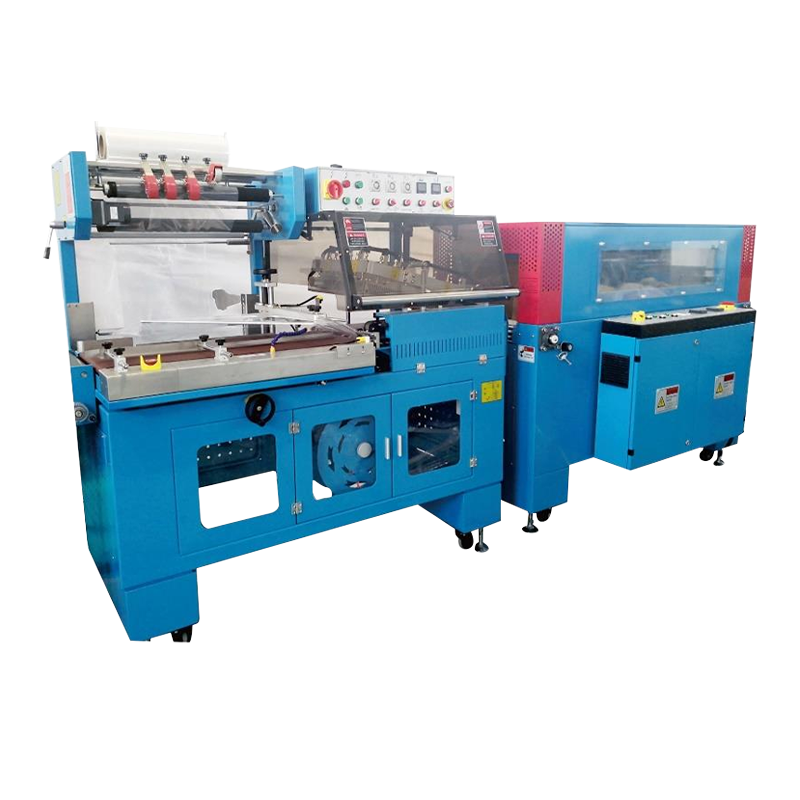
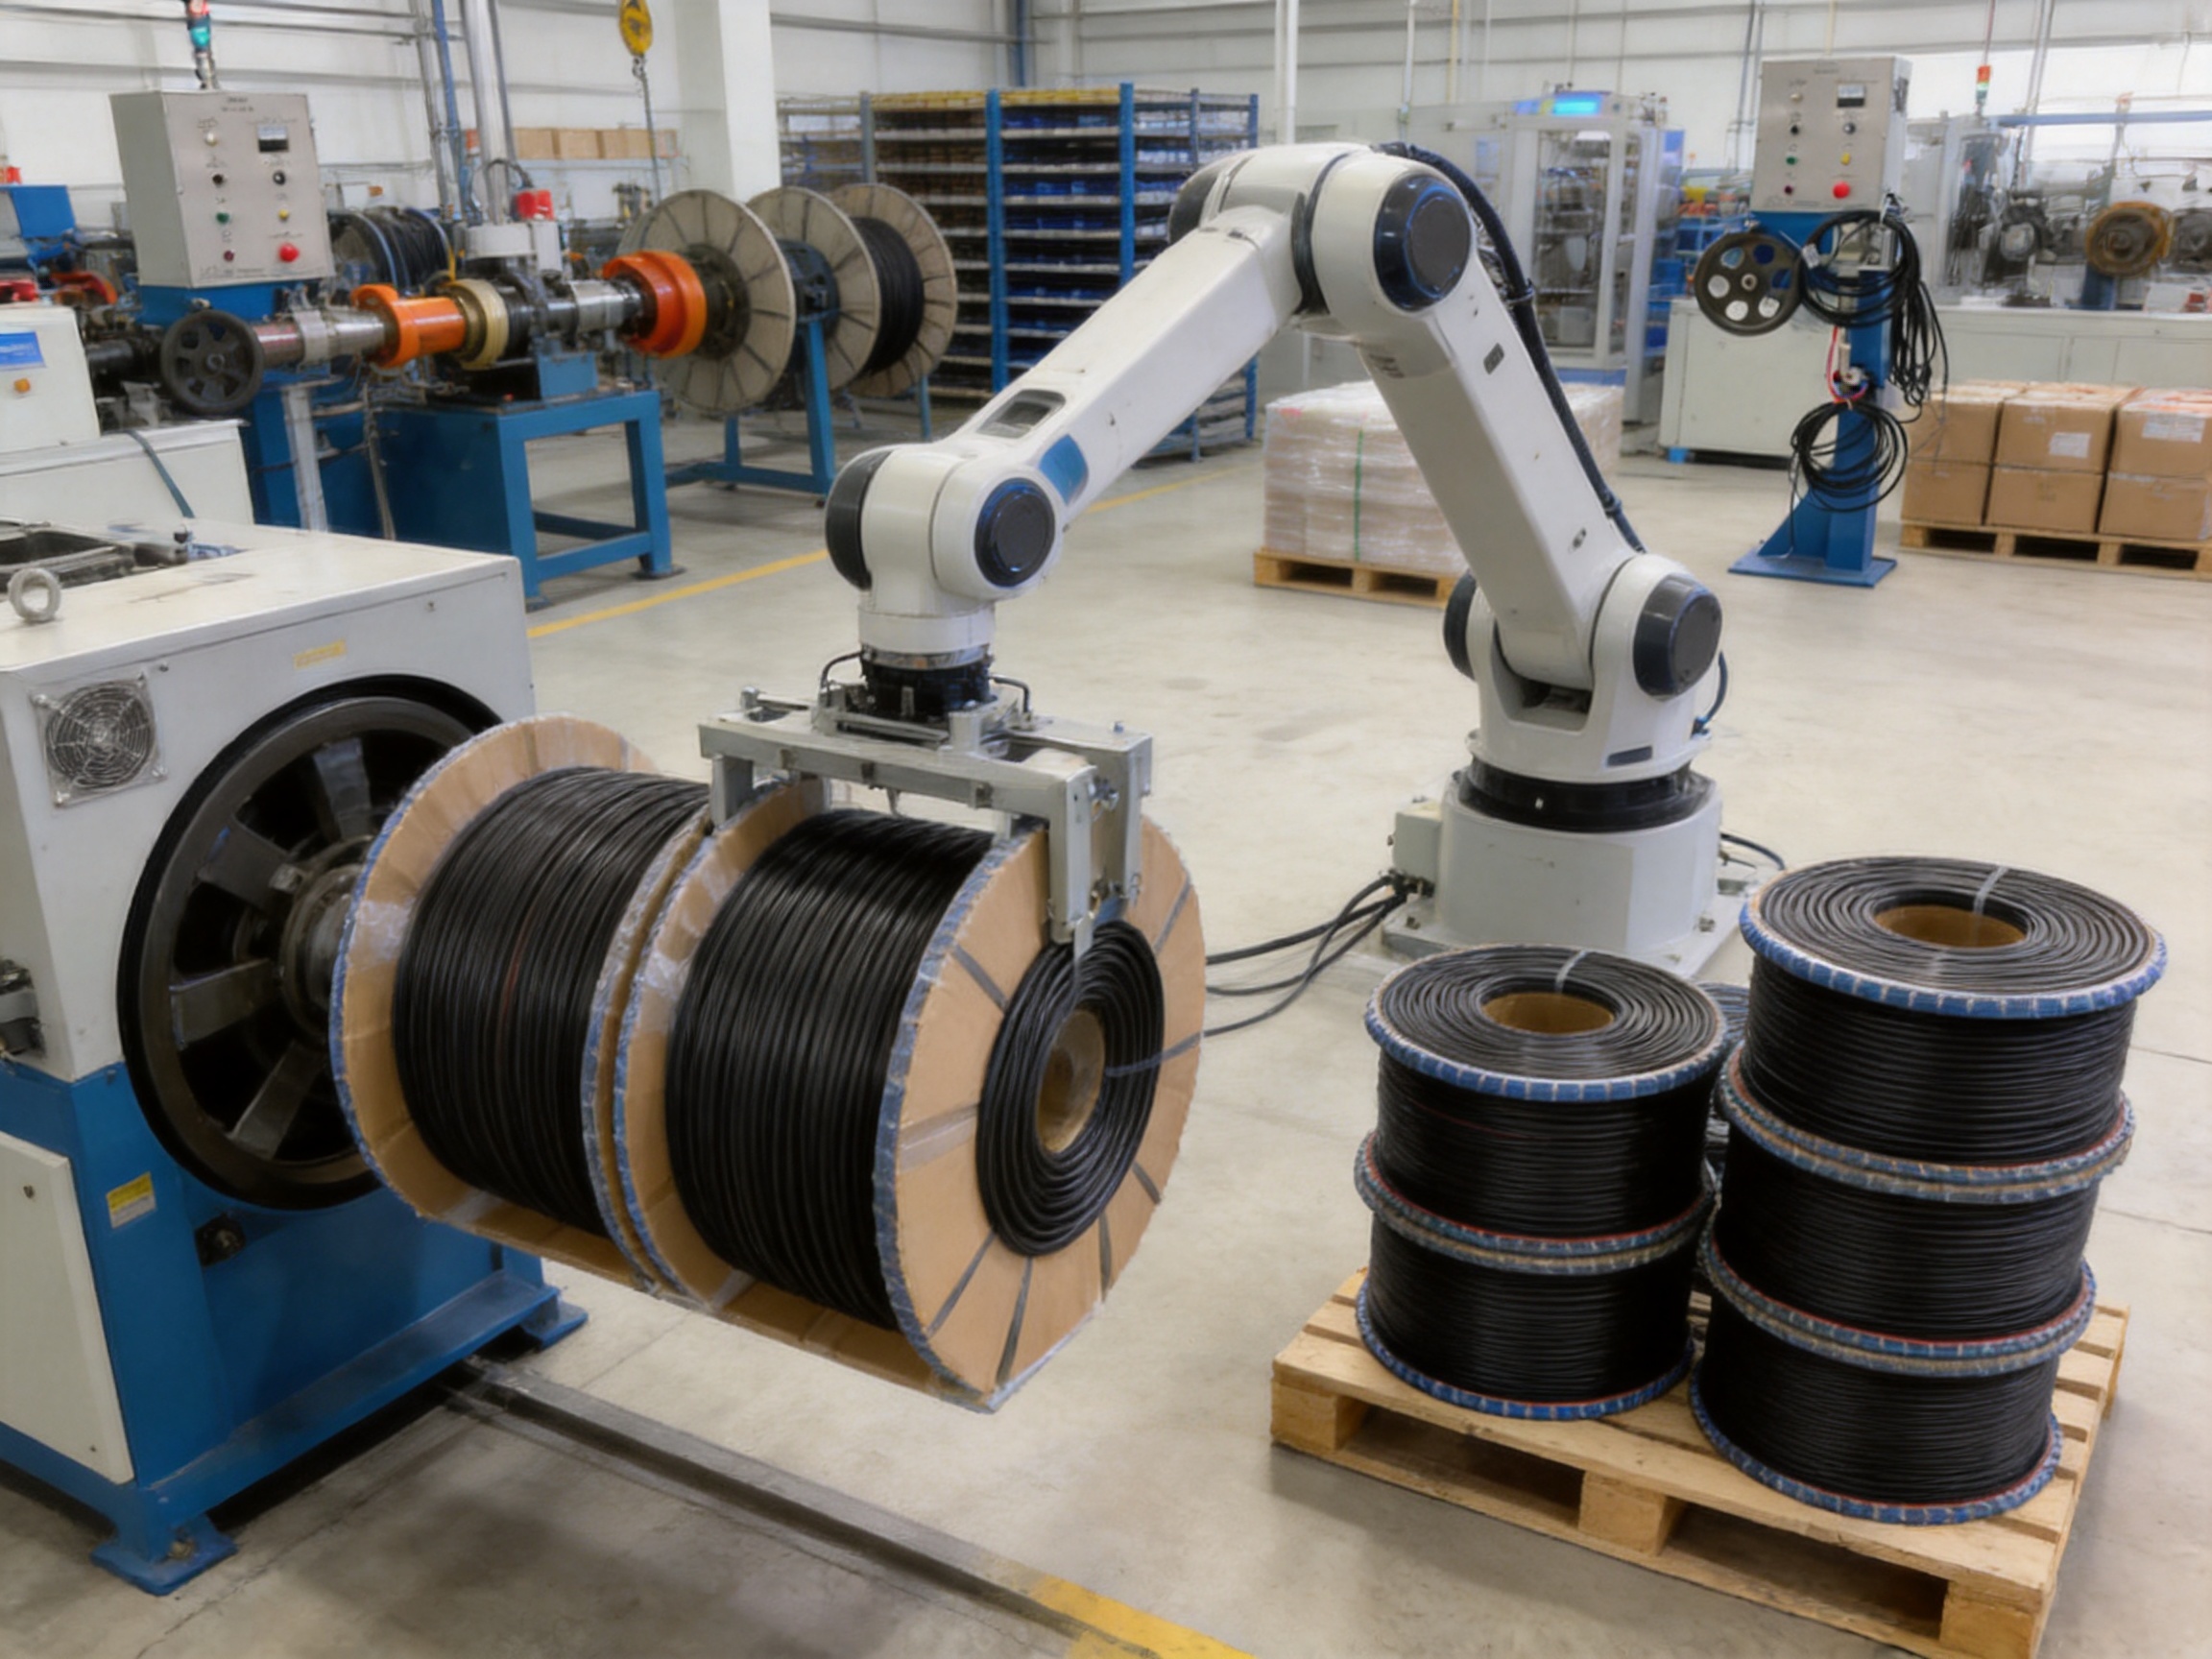
Consistent winding improves packaging reliability as well. Coils and reels with stable edges are less likely to shift during handling. They can be labeled, wrapped, stacked, and transported more efficiently. When combined with fully automatic coiling and packaging equipment, tension control contributes to a more complete finished-product handling system.
For manufacturers producing multiple cable specifications, repeatable tension management can also support faster changeovers. Once suitable operating parameters have been established for a product family, operators can use a controlled procedure instead of relying entirely on personal experience. This encourages more consistent results between production shifts.
Efficiency, Yield, and Cost Control
Product waste is a major concern in wire and cable manufacturing because cable materials, insulation compounds, conductors, and packaging materials all represent direct production costs. Tension-related defects may force a manufacturer to trim damaged sections, rewind a coil, downgrade a product, or scrap material completely.
By maintaining a more stable winding condition, the Wire Cable Tension Control Systems can help reduce these losses. The system supports the correct arrangement of cable and reduces the likelihood of damage caused by excessive or insufficient force. Even a small improvement in usable output can have a meaningful impact when the line operates continuously or processes high-value cable.
Efficiency improvements also come from reduced stoppage time. When a cable becomes tangled or forms a disordered coil, the operator may need to stop the line, remove defective material, reset the equipment, and restart production. These interruptions reduce effective machine utilization and may affect the schedule of downstream packaging or delivery.
Stable tension supports continuous operation by reducing the frequency of manual correction. It can also help lower the amount of rework required after production. The equipment therefore contributes to both direct savings, such as reduced scrap, and indirect savings, such as lower labor requirements and better use of machine capacity.
For a complete cable production line, these benefits accumulate across several processes. A stable extrusion output can be taken up more effectively, storage racks can be used more efficiently, coiling equipment can operate with fewer interruptions, and automatic packaging can receive a more consistent product. The result is a more coordinated production workflow.
Application Areas
Wire Cable Tension Control Systems are suitable for a wide range of cable manufacturing and processing scenarios. Their primary application is cable winding, but the same tension management principle is useful wherever cable must be transferred, accumulated, coiled, or taken up under controlled conditions.
Extrusion Lines
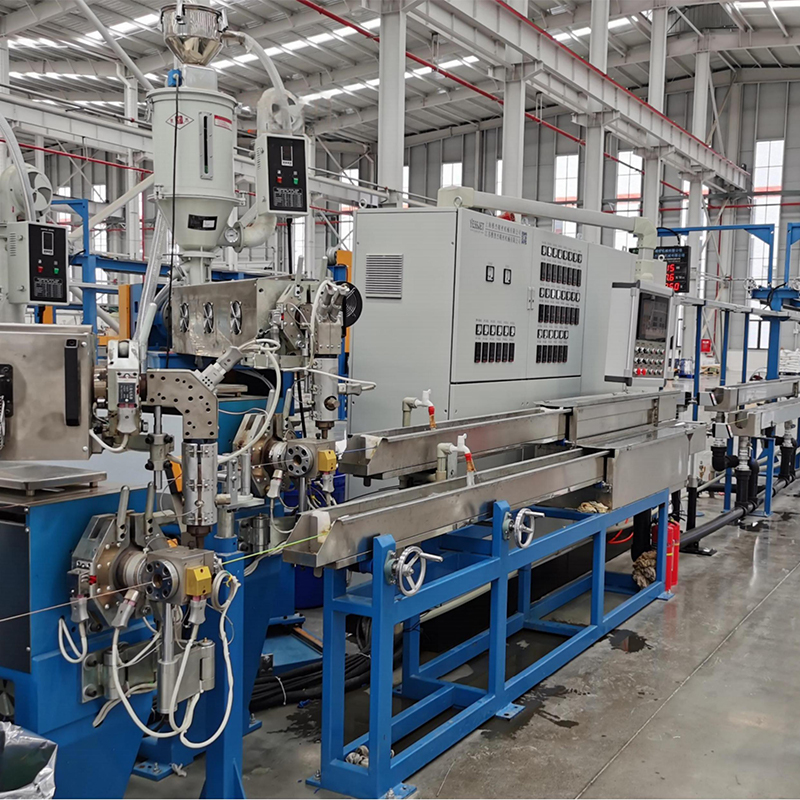
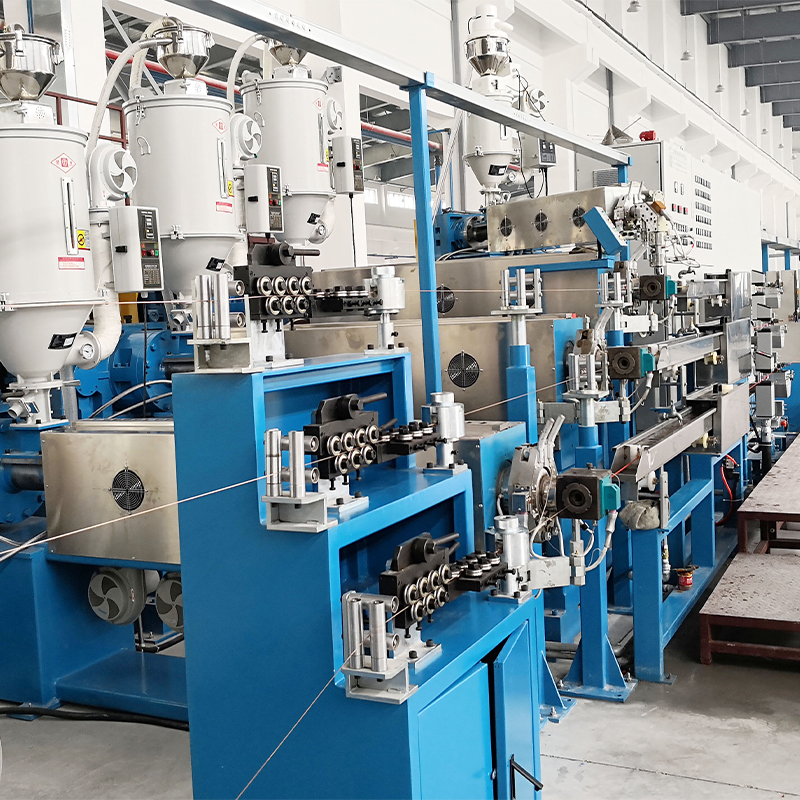
After insulation or jacketing, cable usually moves through cooling, drying, inspection, and traction stages before it reaches a take-up machine. Tension control can help maintain stable movement at the downstream end of the extrusion line. This supports orderly collection and reduces the chance that a change in take-up behavior will affect the finished surface or cable geometry.
Motorized Take-Up Equipment
Take-up equipment must collect cable at a suitable speed while the reel diameter changes. Tension control helps the take-up unit operate with more consistent cable force. This is important for long production runs, where the winding condition at the beginning of a reel may differ from the condition near the end.
Motorized Pay-Off Equipment
During unwinding, the cable must leave the supply reel smoothly. Excessive resistance can damage the cable or increase the pulling force required by downstream machinery. Insufficient resistance can allow slack to develop. Tension control supports a balanced pay-off process.
Coiling Machines
Coiling machines require stable cable entry to create uniform, well-formed coils. A controlled tension condition helps the machine arrange the cable consistently and reduces the risk of crossed or loose sections.
Storage and Buffer Systems
Storage racks can be used to buffer material between processes or to provide temporary cable accumulation. Tension control helps maintain orderly material placement while allowing different machines to operate at their required speeds.
Packaging and Finished-Product Handling
When cable is coiled for shipment, consistent tension contributes to better package shape and more reliable wrapping. This makes it easier for downstream automatic packaging equipment and intelligent robot stackers to handle the finished product.
Manufacturing and Engineering Strengths
A tension control system must be manufactured with attention to mechanical stability, control accuracy, material guidance, and compatibility with other production equipment. Shanghai Yessjet Precise Machinery Co., Ltd. operates in the wire and cable machinery field and supplies a broad range of related equipment. This product range provides an important engineering advantage because tension management can be considered within the context of the complete production line rather than as an isolated accessory.
The company’s product categories include wire and cable extrusion lines, fully automatic coiling and packaging equipment, intelligent robot stackers, coiling machines, motorized pay-off equipment, motorized take-up equipment, accessory equipment, and cable extrusion machines. This broad scope supports a systems-oriented approach to project planning.
In practical terms, a systems-oriented manufacturer can evaluate how cable enters the tension control unit, how it leaves the system, how it interacts with storage racks, and how it connects with take-up or coiling equipment. This reduces the risk of selecting an accessory that performs well independently but creates compatibility problems within the overall line.
The manufacturing process should begin with application analysis. Cable diameter, construction, material flexibility, line speed, winding method, reel size, and production objectives all influence tension requirements. Understanding these conditions allows the equipment configuration to be matched more closely with the customer’s actual process.
Mechanical design is another important stage. Cable guides, rollers, supports, adjustment components, and connection points must be arranged to provide a stable cable path. The structure should be sufficiently rigid for continuous industrial operation, while access points should permit inspection, cleaning, adjustment, and maintenance.
Control-system preparation is equally important. Tension control is most useful when the machine can respond predictably to changes in cable movement. The control concept should therefore consider signal stability, adjustment range, operating response, and communication with related equipment where required by the line design.
Assembly quality has a direct influence on performance. Components must be installed with appropriate alignment so that the cable does not experience unnecessary side loading or friction. Mechanical movement should be checked before the system is connected to production equipment. Proper assembly also helps reduce premature wear and makes the system easier to maintain.
Testing should cover both basic operation and application-related behavior. The equipment should be checked for smooth cable travel, stable adjustment, correct response to operating changes, and compatibility with the intended winding process. A manufacturer that combines design, assembly, testing, and line integration experience is better positioned to deliver a practical solution.
Advantages of a Complete Machinery Supplier
One of the main advantages of working with a supplier that offers multiple types of wire and cable machinery is improved coordination. A customer may need more than a tension control accessory. The project may include extrusion, pay-off, take-up, coiling, packaging, storage, and robotic stacking. When these requirements are considered together, the equipment can be planned around a common material flow.
This approach can simplify technical communication. Instead of discussing the tension system separately from the take-up or coiling machine, the customer can describe the complete production objective. The supplier can then consider the relationship between line speed, cable movement, winding quality, and finished-product handling.
A broad product portfolio can also support staged investment. A manufacturer may initially add tension control to an existing line and later upgrade coiling, packaging, or stacking equipment. Because the equipment is considered as part of a wider machinery family, future expansion can be planned more effectively.
Another strength is the ability to provide customized wire and cable production line solutions. Cable manufacturers often have different factory layouts, product specifications, output targets, and automation requirements. A standard accessory may not be sufficient for every application. Engineering support allows the system to be adapted to the customer’s working conditions without adding functions that provide no practical value.
Shanghai Yessjet Precise Machinery Co., Ltd. is positioned as a wire and cable machinery manufacturer serving customers that require production equipment and turnkey solutions. Its equipment scope reflects experience across several connected stages of cable processing. For tension control applications, this means the product can be evaluated in relation to the customer’s existing or planned machinery.
Quality-Oriented Manufacturing Process
A reliable industrial accessory is the result of a controlled manufacturing process rather than one individual component. The process should connect application requirements with engineering design, component preparation, assembly, testing, and final delivery.
Application Review
The first step is a review of the cable and production line. Important information includes the cable type, diameter range, winding method, supply and take-up arrangement, expected speed, reel dimensions, and whether a storage rack is used. This information helps establish the operating conditions for the tension control system.
Configuration and Design
After the application has been reviewed, the system can be configured for the intended line. The design should address cable entry and exit, equipment position, adjustment method, connection with upstream and downstream machines, and access for operators. Good design minimizes unnecessary cable bending and simplifies daily use.
Precision Assembly
During assembly, mechanical components must be aligned carefully. Cable-contact surfaces should be suitable for the intended application, and moving parts should operate smoothly. The frame and support structure should be installed securely so that vibration or movement does not interfere with stable tension management.
Functional Inspection
Functional inspection confirms that the equipment can perform its basic adjustment role. The manufacturer should verify movement, response, cable guidance, connection points, and operating consistency. Inspection also provides an opportunity to identify assembly issues before the equipment reaches the customer’s factory.
Line Compatibility Verification
Because tension control equipment is normally connected to other machinery, compatibility is an essential part of quality assurance. The system should be considered in relation to pay-off speed, take-up speed, coiling movement, storage capacity, and the intended production sequence. This broader verification helps reduce commissioning difficulties.
Delivery and Technical Support
Clear documentation, installation guidance, and operating recommendations can help customers bring the equipment into production more efficiently. Technical support is particularly valuable when the system is integrated into an existing line with equipment from different manufacturers. A practical supplier should help the customer understand the correct operating logic and maintenance requirements.
Operational Benefits for Cable Manufacturers
The system provides benefits to several levels of a manufacturing organization. For machine operators, it reduces the need for constant manual intervention. For quality personnel, it supports more consistent cable arrangement and fewer tension-related defects. For maintenance staff, smoother operation can help reduce unnecessary mechanical stress. For production managers, it contributes to better yield and more predictable output.
Operator convenience is important in continuous cable production. A line may operate for many hours, and cable conditions can change during that period. A tension control system allows the process to respond more effectively than a purely manual approach. Operators can monitor the equipment and make planned adjustments rather than reacting to every small variation in winding behavior.
Quality consistency is also easier to achieve when the process is repeatable. If different operators use different manual techniques, the same cable may be wound with different tightness or arrangement from one shift to another. A controlled system helps reduce this variation and establishes a more stable operating method.
Production planning benefits from fewer unexpected interruptions. When winding defects are reduced, the line can maintain a more predictable output rate. This supports scheduling, material preparation, packaging coordination, and shipment planning.
The equipment can also support a cleaner and more organized factory workflow. Neatly wound cable is easier to identify and move. When combined with automatic packaging and robot stacking systems, it can contribute to a more efficient finished-product area with less manual handling.
Selection Considerations
Before selecting a Wire Cable Tension Control System, manufacturers should evaluate the complete application rather than focusing only on the accessory itself. The correct solution depends on the cable, production line, and desired winding result.
Cable Characteristics
The cable diameter, weight, flexibility, insulation material, outer jacket, and construction should be considered. A delicate or flexible cable may require a different tension range from a large, rigid power cable. The system should be selected according to the mechanical sensitivity of the product.
Line Speed
Production speed influences the response required from the tension control system. Higher speeds can make tension changes more noticeable and may require closer coordination with pay-off and take-up equipment. The intended operating range should therefore be communicated during the selection process.
Winding Method
Different products may be wound on reels, formed into coils, placed in baskets, or accumulated in storage racks. The winding method affects how tension should be managed. A system for a take-up reel may have different requirements from one used with a coiling machine.
Reel Diameter and Material Length
Changing reel diameter is a major reason why fixed settings may not be sufficient. The solution should be suitable for the expected reel sizes and cable lengths. Long continuous runs may require especially stable operation over the full winding cycle.
Existing Equipment
If the system is being added to an existing production line, the supplier should understand the current pay-off, extrusion, storage, take-up, and coiling equipment. Installation space, cable path, machine interfaces, and control requirements should be reviewed before final configuration.
Maintenance and Accessibility
Operators should be able to inspect cable-contact areas, clean the equipment, and perform routine checks without excessive downtime. A practical industrial design should support straightforward maintenance and provide access to components that may require adjustment or replacement.
Installation and Commissioning Approach
Installation begins with positioning the equipment so that the cable follows a smooth and controlled path. The entry and exit points should be aligned with adjacent machines. Sudden changes in direction, unnecessary friction, and unstable supports should be avoided because they can introduce tension variations that the system is not intended to correct.
The system should then be connected to the relevant production equipment according to the line design. This may include a storage rack, motorized pay-off, motorized take-up, coiling machine, or other accessory unit. The installation team should confirm that all mechanical and control interfaces are secure before starting production.
Commissioning should begin at a moderate operating condition. The cable path, winding arrangement, and tension response can be observed before the line is raised to its normal speed. This step helps identify alignment issues and allows the operator to become familiar with the adjustment process.
Trial production should cover the expected cable specifications and winding conditions. The manufacturer and customer can review coil tightness, layer arrangement, cable surface condition, reel stability, and the consistency of tension during changes in speed or reel diameter.
Once the process has been verified, operating parameters can be recorded for future production. Keeping a clear record helps different operators reproduce the same conditions and makes product changeovers more efficient. It also provides useful information for preventive maintenance and process improvement.
Maintenance and Long-Term Performance
Routine maintenance is important for preserving stable tension control. Operators should regularly inspect cable guides, rollers, contact surfaces, supports, fasteners, and adjustment components. Any accumulation of dust, insulation residue, or foreign material should be removed according to the equipment’s maintenance instructions.
Alignment should be checked if the cable begins to show unusual wear, uneven winding, or inconsistent movement. A change in cable behavior may be caused by the upstream or downstream machine, but it may also indicate that a guide or support has shifted. Early inspection can prevent a small issue from becoming a larger production problem.
Operating personnel should also monitor the finished coil or reel. Regular layers, stable edges, and an appropriate winding density are useful indicators of correct operation. If the cable becomes too loose or too tight, the line should be reviewed before continuing with a large production quantity.
Maintenance records can help identify recurring conditions. If tension variations occur only at a particular reel diameter, speed, or cable specification, the information may indicate a process setting that requires adjustment. A systematic record allows the manufacturer and customer to improve the line based on actual production data.
Long-term performance also depends on correct use. The system should not be forced to operate outside its intended cable range or speed range. Application changes should be discussed with the equipment supplier so that the configuration remains appropriate for the new product.
Role in Intelligent and Automated Production
Modern cable factories increasingly combine mechanical equipment with automation, data monitoring, automatic packaging, and robotic handling. Tension control is a valuable part of this development because stable material movement is necessary for reliable automation.
Automatic coiling equipment depends on predictable cable entry. Intelligent robot stackers depend on finished coils or reels having consistent dimensions and stable shapes. Packaging equipment depends on products arriving in a repeatable condition. If tension variation causes irregular coils, the performance of these downstream systems may be affected.
By supporting orderly winding, the Wire Cable Tension Control Systems create better conditions for automated handling. The system does not need to perform every automation function itself. Its role is to stabilize one important part of the material flow so that other machines can work more effectively.
This modular approach is practical for manufacturers with different automation levels. A company can use the tension control system with a semi-automatic line, or integrate it into a highly automated production cell. The equipment therefore provides value both as an improvement to an existing process and as a component of a new intelligent factory project.
Why Choose a Practical, Application-Focused Solution
In industrial machinery, more functions do not always mean better performance. Unnecessary complexity can increase installation time, operator training requirements, maintenance difficulty, and overall project cost. A practical tension control system focuses on the essential task: maintaining suitable cable tension during winding and handling.
This focused design is an advantage for manufacturers that want a dependable improvement without purchasing functions unrelated to their production needs. The system can be integrated with the equipment already used in the factory and can be configured around the cable and winding process.
An application-focused manufacturer also pays attention to the complete workflow. Tension control should not be evaluated only by its individual adjustment mechanism. Its value depends on how well it works with storage racks, pay-offs, take-ups, coilers, extrusion lines, packaging machines, and operator procedures.
Shanghai Yessjet Precise Machinery Co., Ltd. combines its tension control offering with a broader portfolio of wire and cable production machinery. This creates an opportunity for customers to obtain coordinated equipment and technical guidance from a supplier familiar with cable processing requirements. The company’s strength lies in connecting accessory equipment with complete production line objectives.
Frequently Asked Questions
What is the main purpose of a Wire Cable Tension Control System?
Its main purpose is to regulate cable tension during winding, coiling, pay-off, take-up, and related handling operations. It helps prevent excessive tension that may stretch or damage the cable and insufficient tension that may cause loose, crossed, or disordered winding.
Can the system be used with a storage rack?
Yes. The system is often used together with storage racks to help maintain orderly cable accumulation and provide a smoother connection between upstream and downstream production equipment.
What problems can uncontrolled tension cause?
Uncontrolled tension can lead to stretched cable, damaged insulation, deformed sections, loose winding, irregular coil edges, overlapping layers, tangling, unstable reels, material waste, and frequent production stoppages.
Is the system suitable for existing cable production lines?
It can be suitable for existing lines when the cable path, machine interfaces, operating speed, and available installation space are reviewed. The final configuration should be selected according to the current pay-off, take-up, storage, coiling, or extrusion equipment.
Can it be used with motorized pay-off and take-up equipment?
Yes. Tension control can help coordinate cable movement between motorized pay-off and take-up equipment. It supports smoother release from the supply side and more consistent collection on the take-up side.
Does tension control improve cable quality?
It can contribute to improved cable quality by reducing mechanical stress and supporting uniform winding. It does not replace the quality controls required for extrusion or conductor production, but it helps protect cable quality during handling and collection.
Can the equipment support different cable specifications?
The applicable range depends on the equipment configuration and the customer’s process requirements. Cable diameter, flexibility, material, speed, winding method, and reel size should be reviewed before selecting the system for multiple product specifications.
How does tension control reduce production waste?
By reducing loose winding, excessive pulling, cable damage, and rework, the system helps increase the amount of usable finished product. It can also reduce stoppages caused by tangled or disordered cable.
Is the system useful for automatic coiling and packaging?
Yes. Automatic coiling and packaging equipment performs more consistently when cable enters the process with stable tension and a predictable arrangement. Tension control supports the material conditions required for these automated operations.
What should be considered before placing an order?
Customers should provide information about cable type, diameter, construction, line speed, winding method, reel dimensions, storage rack arrangement, existing machinery, and desired output. This allows the equipment to be configured more appropriately.
What manufacturing strengths are important when choosing a supplier?
Important strengths include experience with cable production lines, mechanical and control engineering capability, careful assembly, functional testing, line integration knowledge, customization support, and technical service. A supplier with a broad equipment portfolio can often provide better coordination between the tension system and related machinery.
What routine maintenance is required?
Routine maintenance generally includes checking guides, rollers, cable-contact areas, fasteners, supports, alignment, and adjustment components. Operators should also monitor winding quality and clean the equipment as required by the operating instructions.
Conclusion
Wire Cable Tension Control Systems provide an essential solution for manufacturers that need stable, orderly, and reliable cable winding. By adjusting cable tension in real time, the system helps prevent the two opposite problems that frequently affect cable handling: excessive force that may stretch or damage the product, and insufficient force that may create loose or disordered winding.
The equipment is especially valuable when integrated with storage racks, motorized pay-off machines, motorized take-up machines, coiling equipment, extrusion lines, automatic packaging systems, and intelligent robotic handling. Its role is practical and focused, but its effect can extend across the entire production workflow through improved material stability, reduced waste, fewer interruptions, and more consistent finished packages.
Compared with fixed mechanical settings or frequent manual adjustment, a dedicated tension control solution provides better adaptability to changing reel diameters, production speeds, cable specifications, and line conditions. It supports product quality while also improving labor efficiency and production yield.
Shanghai Yessjet Precise Machinery Co., Ltd. brings this accessory equipment into a broader wire and cable machinery portfolio. Its experience with extrusion lines, coiling machines, pay-off and take-up equipment, automatic packaging, robot stacking, and related accessories supports a coordinated approach to cable production projects. Through application analysis, equipment configuration, precision assembly, functional inspection, and line integration, the company can help manufacturers develop practical tension management solutions suited to their production requirements.
For cable manufacturers seeking steady, high-quality output, tension control should be treated as an important part of the production system rather than a minor accessory. Stable cable movement creates a stronger foundation for efficient winding, reliable packaging, and continuous manufacturing performance.
References
1. General principles of web and cable tension management in continuous manufacturing processes.
2. Industrial practices for wire and cable extrusion, take-up, pay-off, coiling, and packaging operations.
3. Manufacturing quality control methods for cable winding, reel handling, and finished-product packaging.
4. Engineering guidelines for integrating storage racks, motorized handling equipment, and coiling systems.
5. Technical information supplied for Wire Cable Tension Control Systems and related wire and cable machinery.